The Vericut Users’ Exchange (VUE) returned to the UK last month and brought customers together for a day of technical insight, awareness, practical CNC machining solutions and knowledge sharing. Prominent among the highlights was a presentation by Stoneswood Precision Components on how Vericut is facilitating innovative processes like interpolation turning to push CNC machining capabilities beyond conventional limits.
For CNC machine shops, the value of Vericut simulation extends well beyond identifying potential collisions. At VUE 2026, held at the Silverstone Museum adjacent to the world-famous Silverstone Formula 1 Circuit, around 60 attendees explored how Vericut software can support everything from production planning and tooling decisions to the development of advanced machining processes.
Following breakfast and registration, attendees were welcomed by Gavin Powell, managing director of Vericut UK, before Gavin Bridger, applications engineering manager, opened the technical programme with a presentation entitled: ‘Feature, Future or Fiction: Vericut 9.6, 9.7 and Beyond’.
An interactive format saw delegates use their phones to vote on whether Vericut capabilities presented by Bridger were current features, planned future developments or pure fiction. With a live leaderboard adding a competitive element, the session proved an entertaining approach. Many attendees were surprised to discover that capabilities such as Vericut Assistant, tool-tip caption pop-ups, verified coolant usage per tool, FANUC TP language support and bidirectional connectivity with Siemens’ Run MyVirtual Machine (RMVM) digital-twin platform, are already available.
The presentation also offered a glimpse of potential future developments, including cloud-based Vericut, virtual reality (VR) for Vericut, and data management for Siemens’ Teamcenter PLM (Product Lifecycle Management) software platform.
Jonathan Hollinworth, area sales manager for northern England and Scotland, followed with an overview of Vericut 9.7. He revealed the latest release delivers performance improvements of 10-40%, alongside expanded AI assistance, streamlined workflows and enhancements to tooling management. He also discussed future developments, including reading semantic PMI (Product Manufacturing Information), an embedded Mastercam interface, and direct Vericut connection to the CNC machine (eliminating the need for a third-party connection).
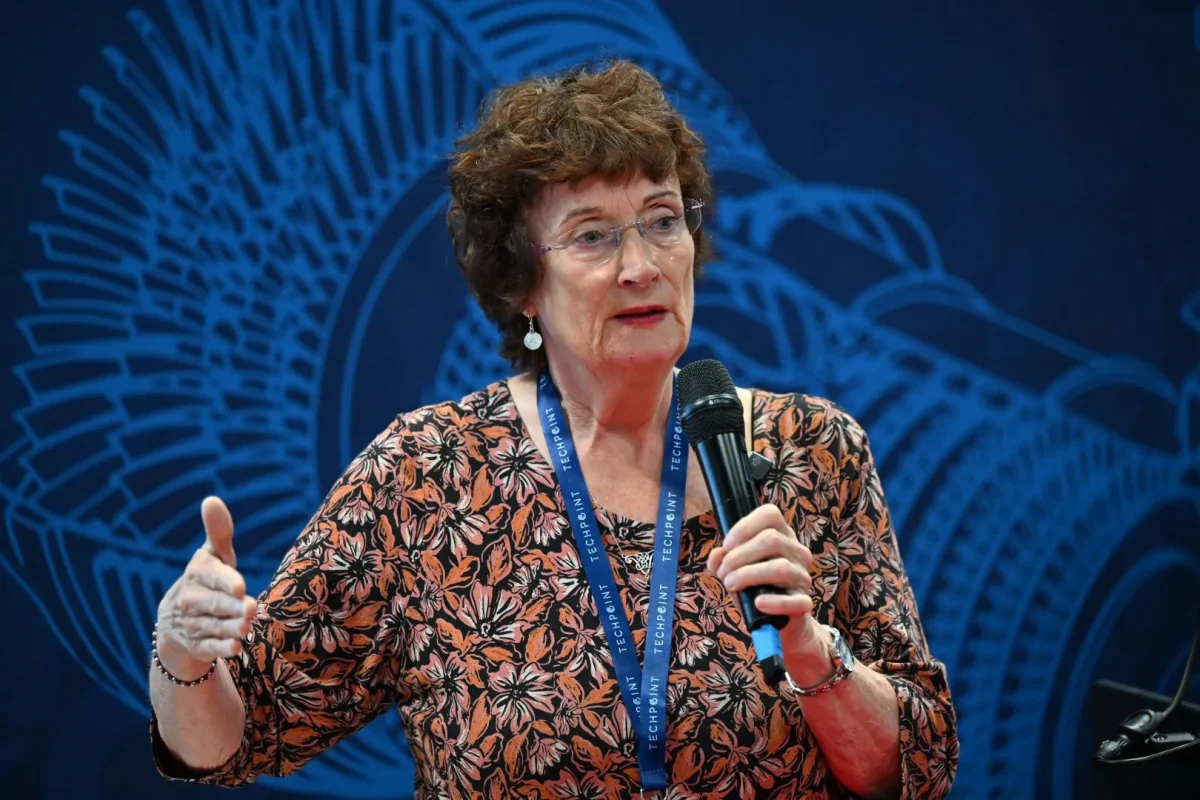
The day’s keynote presentation came from Tom Whitbread, technical engineer at Cheshire-based Stoneswood Precision Components, part of Hyde Aero Products. Specialising primarily in aerostructures for civil and defence applications, Stoneswood’s programming workflow starts in hyperMILL CAM software, with Icam (part of the Vericut software suite and ecosystem) providing the post-processing before Vericut independently verifies the resulting NC code.
“We want to show how we’re using Vericut for more than simply checking whether a toolpath is going to collide,” stated Whitbread. “For instance, the simulation provides useful information for production planning, tooling decisions and developing processes that aren’t necessarily supported by a conventional workflow.”
One notable aspect of Stoneswood’s approach is that its Vericut sessions are built using the same documentation issued to shop-floor operators. Fixture selection, component position, work offsets, tooling assemblies and machine configuration are all checked against the set-up sheet. This strategy provides an independent check of more than the NC code. If the set up documented for the operator does not correspond with the Vericut session, the discrepancy can be investigated before the job reaches the machine.
The company also uses Vericut’s cycle-time estimates to support production planning. After posting and verifying a program, the simulated manufacturing time is fed back to the planning department, helping inform production scheduling and machine capacity decisions.
Whitbread highlighted another practical application: reviewing cutting flute engagement. Vericut’s graphical representation enables programmers to assess how much of a solid-carbide tool is engaged in the cut and evaluate changes to axial engagement as part of process development. The focus is on understanding tool engagement and verifying tooling decisions within the digital workflow.
Stoneswood uses Icam to develop bespoke post-processing functionality for its machine tools. This activity includes controlling specific C-axis table orientations, enabling the company to reposition components and access machining areas that might otherwise exceed the available machine envelope.
Whitbread illustrated the point with a component approximately 2.3 m long that required machining in a working envelope of around 1.6 m. By controlling table rotations through bespoke post-processing, the company could access the required length while working within the machine’s physical limitations. Vericut then independently simulated the resulting machine behaviour. It was close, but perfectly safe, providing complete peace of mind for Stoneswood.
The presentation by Whitbread also covered the use of gear-driven and coolant-driven angled heads for hole-making, with Vericut representing the complete assemblies to verify access, orientation and collision risks.
However, it was interpolation turning that provided the most striking example of Stoneswood’s efforts to extend its manufacturing capabilities.
Available on the company’s DMG Mori DMC series machining centres, interpolation turning enables the production of turned features through co-ordinated machine movement, rather than transferring the component to a conventional turning operation. The challenge was not simply making the machines perform the process. Stoneswood wanted to integrate interpolation turning into the same controlled digital workflow used for its conventional machining operations.
Said Whitbread: “It’s one thing to know that the machine can perform a particular function. It’s another to make sure we can program it, post-process it and independently verify what the machine’s going to do before we press start.”
To achieve this, Stoneswood used hyperMILL’s general turning functionality to create the required toolpaths. Using Icam, the company then developed bespoke post-processing logic to translate the output and utilise DMG Mori’s CYCLE806 functionality, producing the machine-specific NC code.
The next step was to develop the Vericut environment so it could interpret the posted code and accurately reproduce the interpolation turning process on both machine configurations.
The result is a workflow that follows the same sequence as conventional machining. Rather than relying on the first physical machining cycle to confirm that the specialist functionality works as intended, Stoneswood can now evaluate the process digitally before it reaches the shop floor.
“That’s the real outcome for us,” stated Whitbread. “We haven’t just made interpolation turning possible on the machine; we’ve brought it into a process where we can understand and prove the behaviour before manufacturing begins.”
After lunch, attendees had the opportunity to tour the Silverstone Museum with a free pass courtesy of Vericut UK before returning for a demonstration of the latest Icam Post V27, delivered by Bridger.
The latest release includes AI-powered assistance, regression testing and enhanced debugging tools designed to support post-processor development and validation. The demonstration highlighted how the software can help teams compare NC output, investigate changes and maintain reliable machine-specific code.
Bridger also provided an informative Vericut ‘Tips & Tricks’ presentation, before the event concluded with round tables led by Vericut experts, providing attendees with an opportunity to discuss their own challenges and exchange practical knowledge.
Ultimately, every VUE event is about bringing the Vericut community together to share experiences, explore possibilities and learn from industry peers. The Stoneswood presentation in particular was a great example of how customers are using Vericut in innovative ways, perhaps providing attendees with ideas they could take back to their own manufacturing operations.
More information www.vericut.com/en-gb