Interchangeable-head PCD Mill Reduces Machining Costs

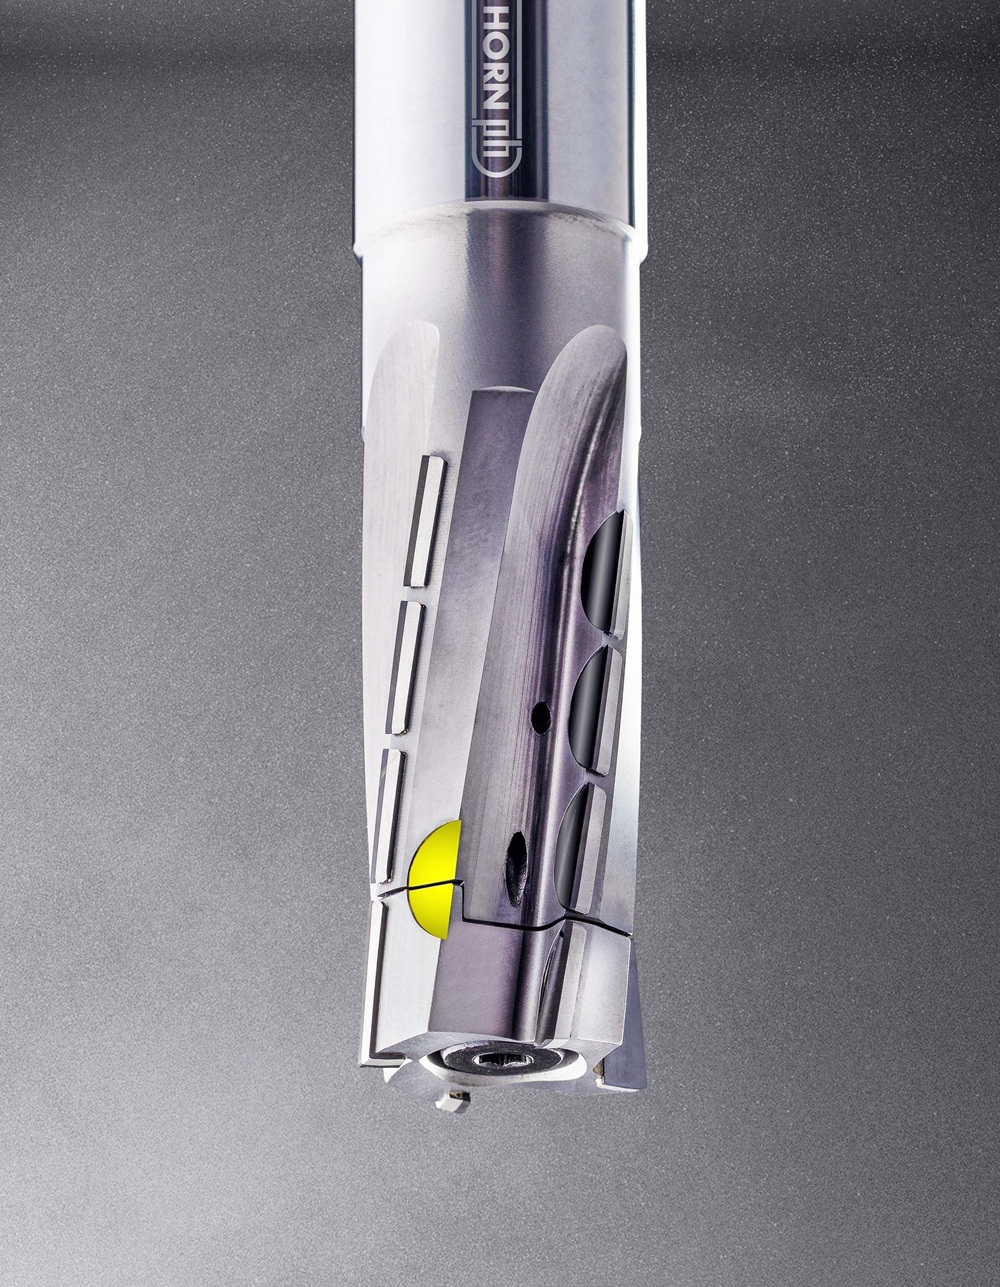
Cutting tool manufacturer Horn has introduced a modular range of PCD (polycrystalline diamond) end mills for machining aluminium, plastics and other materials in groups N (non-ferrous) and O (non-metallic). The system combines a reusable, solid-carbide shank and a PCD-tipped, interchangeable steel head. Availability in the UK and Ireland is through Horn Cutting Tools. 
 
Horn has designed the DM40 system to conserve resources and ensure cost-effective machining. The end cutting edges of the mill are among the main wear zones, while peripheral cutting edges longer than twice the tool diameter are susceptible to high lateral cutting forces, vibration and chipping. Notably, the ability to change just the head reduces follow-on costs compared with conventional monobloc tools, especially as the worn, brazed-on, PCD tips can be resharpened up to twice. 
 
By designing the cutter with a separate shank and head, Horn has ensured that the consumable cost is not only lower but also more predictable, making the tool system suitable for series production runs and automated lines. Users can quickly replace the head module on-site, so the tool is rapidly back into service, maximising spindle uptime. 
 
The head is attached to the shank via a central clamping screw that provides both a force-fit and a form-fit connection. Colour coding facilitates the identification of components, while a poka-yoke principle prevents assembly errors. The rigidity of the interface ensures precise machining, whether using a new or a resharpened tool, and the large axial rake angle enables smooth cutting and produces a smooth surface finish. 

More information www.horn-group.com 

Walter Launches Two New Tiger·tec Gold Turning Grades

Whether for offshore applications, oil and gas production, food manufacturing or the defence, chemical or energy sectors, the new Tiger·tec Gold MT-TiCN-CVD turning grades WMP20G and WMP30G can make a difference. With this product line, Walter is responding to growing global demand for stainless steel components. 

The WMP20G universal grade is now Walter’s first choice for traditional applications involving ISO M materials. Thanks to its hardness, it is suited to high cutting speeds and mass production. The grade is designed to deliver maximum productivity and long tool life when machining austenitic, ferritic, martensitic and duplex materials up to ISO P.  

Walter’s tougher WMP30G grade is a problem-solver, particularly for large and expensive components and in single-part manufacture, where maximum reliability is paramount. The company cites turning weld seams in armour plating as a typical example that demonstrates its durability. 

The most significant special feature is the new gradient substrate. Thanks to localised cobalt insertions, it is particularly tough at the cutting edge yet hard at the core. Such a design protects the cutting edge from chip impact and helps minimise fractures. A double post-treatment of the cutting edge further reduces friction.  

This completely new type of indexable insert design is rounded off by a Tiger·tec Gold coating specially adapted for ISO M machining, as well as the stable RM7 roughing geometry.  

The coating is particularly suitable for machining forged parts or for standard geometries that are prone to fracture when turning against a shoulder. Together, they form a solution package that Walter says is unique on the market to date, offering high levels of reliability and wear resistance, and suitability for the entire range of stainless steels. 

More information www.walter-tools.com 

MAPAL Unveils Technological Breakthrough in Fine Boring

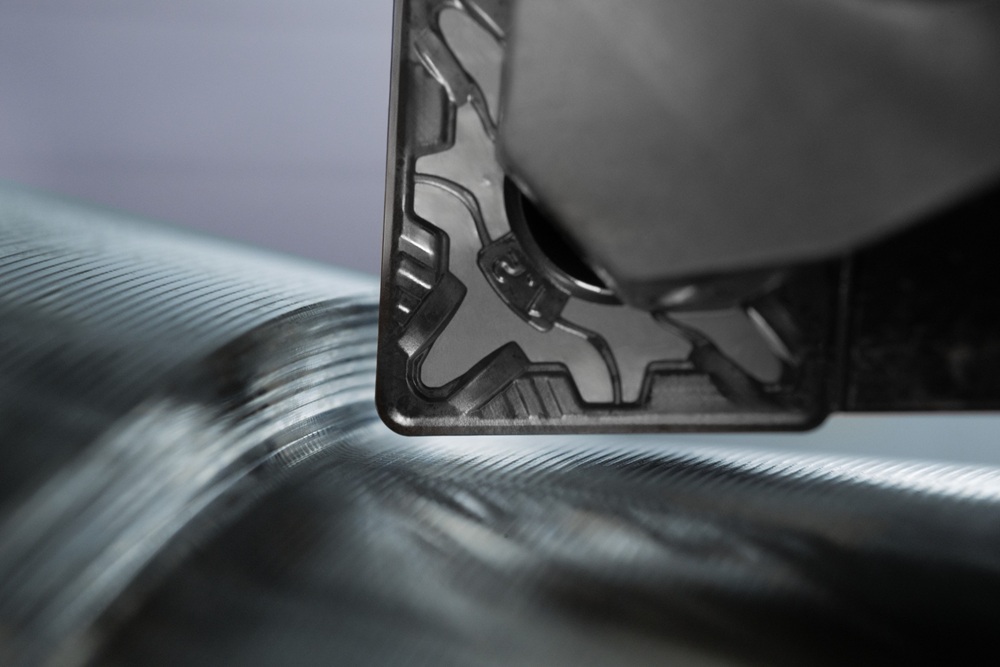
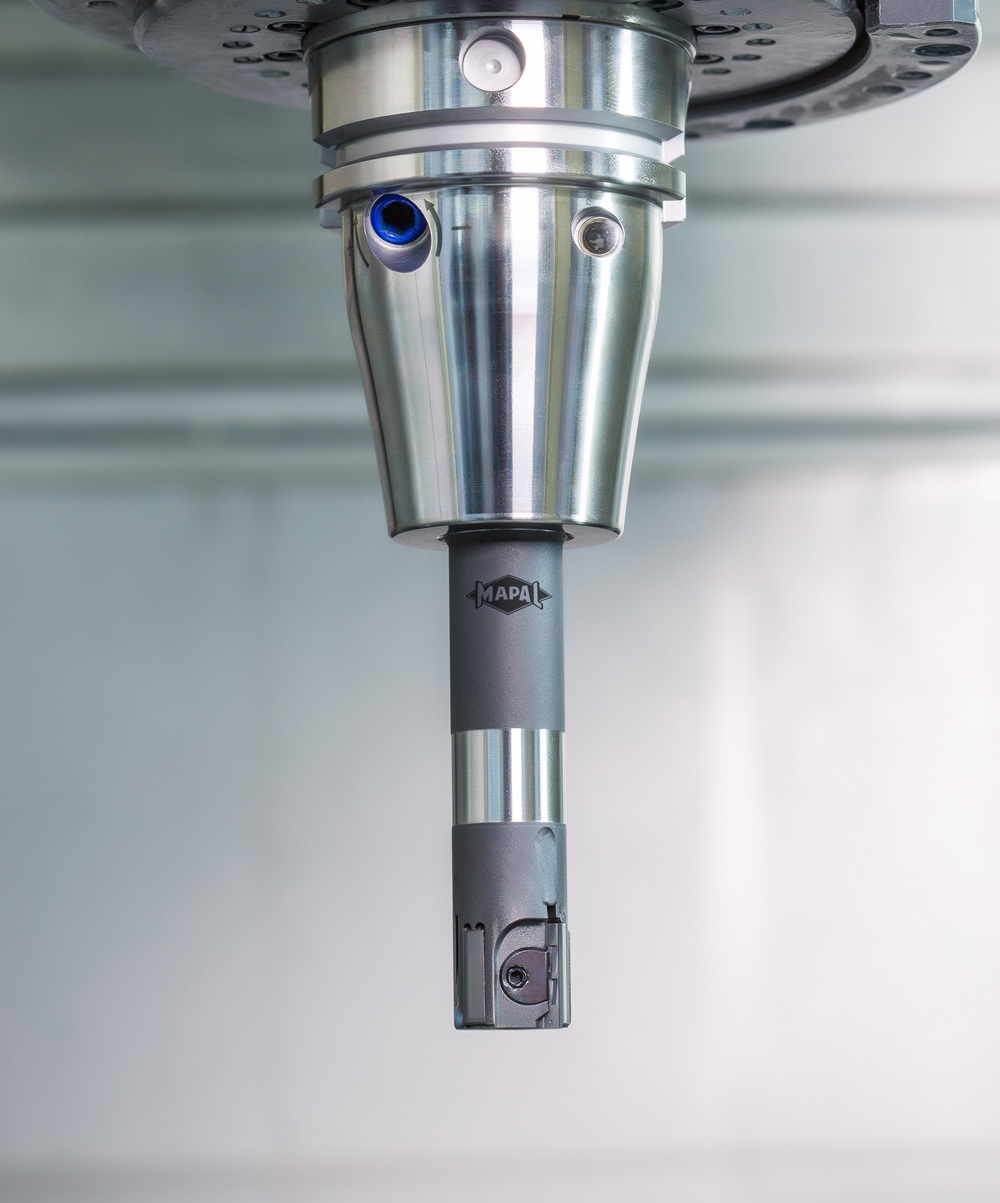
According to MAPAL, the company’s new EA-Performance-System sets a new benchmark in fine boring, bringing one-screw setting to the demanding 10 to 19 mm diameter range for the first time. The system reduces setting effort while maintaining high precision, surface quality and process reliability. 

Conventional fine-boring tools use two adjustment elements to set diameter and cutting-edge taper, making the process sensitive and dependent on operator expertise. MAPAL’s EasyAdjust-System, previously available from 20 mm diameter, simplifies this process with a single adjustment screw for diameter and a back taper permanently integrated into the cartridge system. 

MAPAL has now transferred this principle to the 10 to 19 mm range, using a new design configuration suitable for a broad spectrum of materials. The stable insert fixation required at these small diameters places high demands on system design, manufacturing precision and stability. MAPAL has addressed this by adapting the connection between the indexable insert and clamping system. 

At the heart of the EA-Performance-System is a newly developed indexable insert with defined contact geometry. Combined with a matching clamping jaw, this provides positive-locking, reproducible insert positioning. The clamping mechanism transfers the setting movement precisely while maintaining secure fixation under process load. 

The system enables micrometre-precise setting with simplified handling, helping to minimise correction effort and reject rates while supporting stable machining processes. This capability makes it suitable for applications including high-precision fit and bearing bores in transmission housings, cylinders, crankshafts and camshafts. 

MAPAL’s EA-Performance-System is already in use at selected customers, with ongoing production confirming stable setting behaviour and reproducible machining results. 

More information www.mapal.com

Introducing the CoroMill MR20 for Controlled Profile Milling

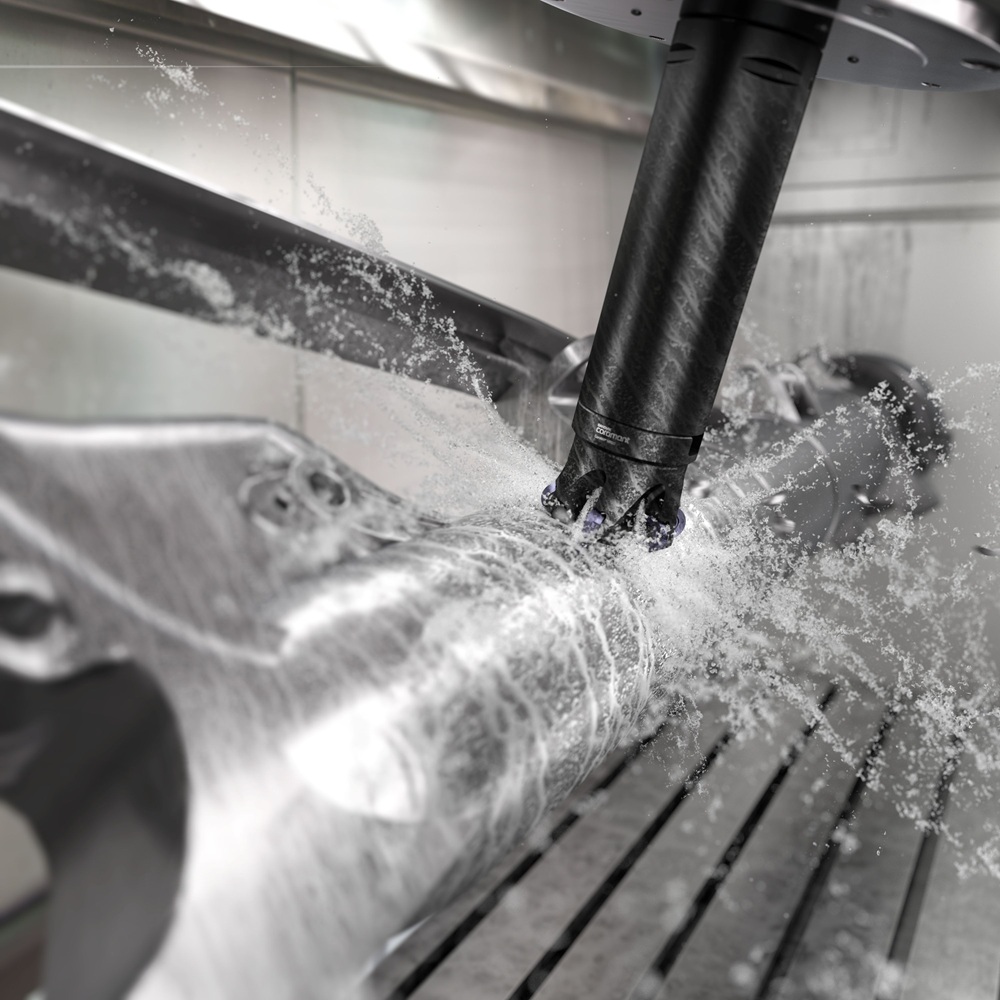
Sandvik Coromant says its new indexable milling concept combines stability, predictable performance and high metal removal rates across demanding materials and applications. CoroMill MR20 is a single-sided round-insert milling concept developed for secure, high-performance profiling and face milling. Optimised for ISO M, ISO S and ISO P materials, it is suited to pocketing and complex profiling in titanium and other HRSA materials. 

CoroMill MR20 also provides reliable roughing and semi-finishing in ISO P die and mould applications, while its high metal removal capability makes it suitable for pump and valve components in ISO M materials. 

“Our goal while developing CoroMill MR20 was to create a polyvalent cutter that offers the highest level of process security,” reveals Alvaro Ruiz, global product application specialist at Sandvik Coromant. “Customers machining high-value components need predictable, repeatable performance, and CoroMill MR20 delivers exactly that.” 

The cutter features an optimised insert seat with a large contact area between the insert and cutter body, minimising micro-movement for greater stability. An advanced cutter body design provides resistance to fatigue and deformation, while an integrated under-coolant system supports performance in long-chipping and difficult-to-machine materials. 

The six-edged insert has a thick, robust body for high bulk strength and edge-line security. Tight manufacturing tolerances promote gradual, predictable wear, supporting unmanned production, reduced scrap and high uptime. 

CoroMill MR20 can also contribute to more sustainable machining. Higher feed-per-tooth capability can reduce machining energy requirements, while long tool life means fewer inserts are consumed, reducing waste and associated carbon emissions. 

“Increasing feed capability while extending tool life means fewer resources used and less waste generated,” adds Ruiz. “It’s a win for productivity and for sustainability.” 

More information www.sandvik.coromant.com 

MANUFACTURERS URGED TO BE BOLD, NOT BOWLED OVER, BY ARTIFICIAL INTELLIGENCE 

Manufacturers are being urged to harness the huge potential of AI without getting lost in the hype. The rallying call emerged from a major gathering of northwest manufacturers and technology experts hosted by Safran Nacelles in Burnley. An honest debate explored the opportunities, barriers and real-world impact of one of the fastest-moving technologies facing industry. 

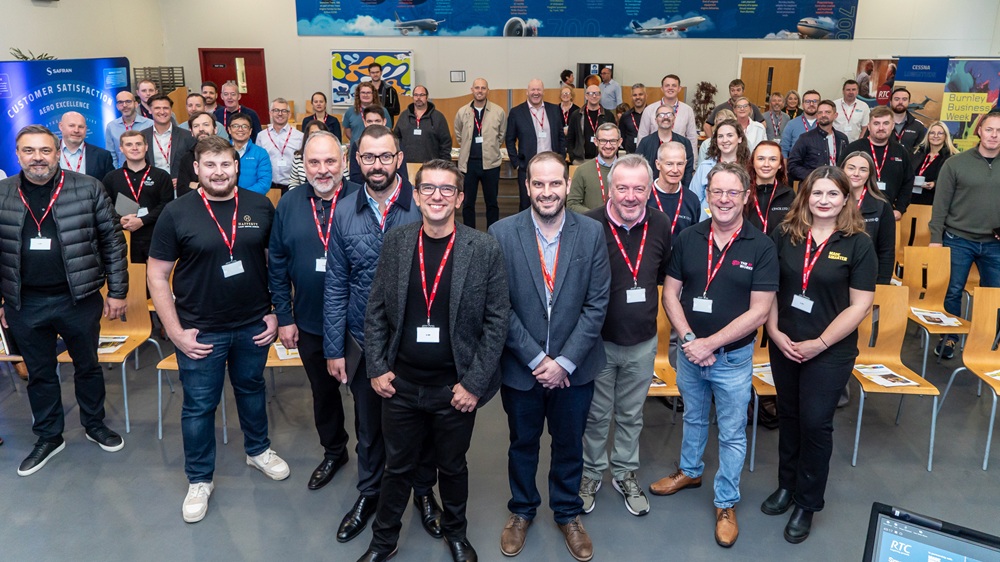
The event, entitled ‘Smarter Manufacturing: Using AI to Improve Productivity and Performance’, was organised by RTC North, Made Smarter North West and Burnley Council, as part of Burnley Business Week and to mark the recent Make UK’s National Manufacturing Day. 

Almost 50 delegates attended the event, including manufacturers from sectors spanning aerospace, automotive and machinery to plastics and printing, with attendees travelling from across the northwest and as far afield as Yorkshire, London and the southwest. 

Business leaders shared how they are already using AI to save time, cut costs and improve productivity, but also spoke candidly about ‘AI fatigue’, a lack of time and specialist skills, concerns around data and security, and the challenge of keeping pace with the technology. 

The message was to be brave enough to experiment, but sceptical enough to question the results. Businesses were encouraged to start small, focus on genuine problems and keep human judgement firmly in the loop. 

Steve Wilkinson, of innovation and business support consultancy RTC North, said manufacturers should not be put off by the “noise” surrounding AI or feel under pressure to make a giant leap: “There’s a lot of dabbling and playing going on, and that’s a good thing. It’s part of technology adoption. What matters is finding justified, meaningful applications that help people in manufacturing make better decisions faster.” 

Ronan Hafferty, founder of Salford-based Hafferty Interiors, is already putting that approach into practice. With support from Made Smarter North West – the Government-backed programme helping SME manufacturers adopt digital technologies through expert advice, skills development, internships and grant funding – his company has deployed a digital intern to develop an AI strategy and explore applications from quality through to manufacturing. 

“AI has already made a real difference, particularly in design where it has saved us a huge amount of time and cost,” he said. “It’s blowing our minds every week with how quickly it’s developing. But you can’t be lazy with it. You can’t get rid of common sense and the human element.” 

That mix of excitement and healthy scepticism ran throughout the event. Judson Smythe, MD of Blackburn-based MGS Plastics, warned against ignoring AI’s potential or handing over too much control, urging fellow makers to “use AI as a tool, but don’t be the tool that AI is using”. 

Firms struggling to find the specialist skills or time to explore AI were also encouraged to look within their own organisations. Mike Riding, MD of Burnley-based Process Instruments, discovered an unexpected pool of knowledge and enthusiasm among his workforce after setting up an internal group to explore where AI could benefit the business. 

Safran Nacelles – which designs, builds and services jet engine housings known as nacelles for commercial, regional and business airplanes – offered a different perspective from a major manufacturer already well into its digital transformation journey. The 750-strong Burnley operation is exploring AI alongside technologies including manufacturing execution systems, connected machinery, simulation and automated inspection. 

Michelle Hubel, head of digital transformation, said the key for any business was to focus on the fundamentals of good data, the right skills, strong governance and security, and people able to question and verify what the technology produces. She said: “We all think we’ve got good data until we actually start looking at it.” 

A second panel featuring experts from Made Smarter North West, marketing agency Door4, IT and cyber security specialist Seriun and training consultancy The AI Works focused on how manufacturers can move from curiosity to practical applications. 

Mark Edwards of Seriun challenged the idea that AI needs to be sophisticated to make an impact, highlighting real-world examples of simple applications already delivering significant bottom-line gains for businesses. 

“Don’t worry about the stuff that AI can’t fix or can’t help,” he stated. “Use it to fix the things you can today to make your business quicker, faster, better.” 

Kevin Smith, lead technology adoption specialist for Made Smarter North West, urged manufacturers to start with the business problem rather than the technology: “AI doesn’t automate jobs, it automates tasks. Look at what takes up people’s time, what frustrates them and where AI could make a difference. 

“Then start small, get some quick wins and build confidence and skills,” he added. “Keep people at the heart of it and make sure you’re solving a genuine business problem. The opportunity is huge, but ultimately AI has to deliver value for your business.” 

The event concluded with a guided tour of Safran Nacelles’ Burnley manufacturing operations, giving delegates an opportunity to see its sheet-metal and nacelle production, and learn more about the aerospace manufacturer’s own digital transformation journey. 

More information www.madesmarter.uk