CHMER Strengthens Dutch Presence Through Hoffman-Metalcare 

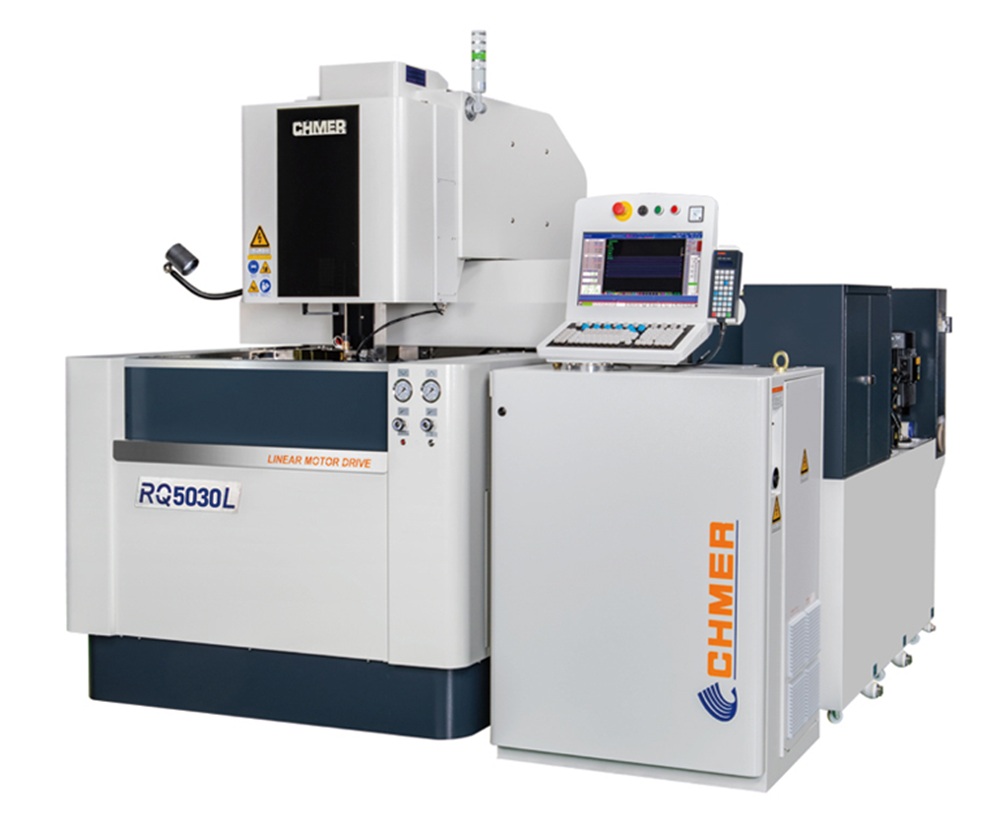
CHMER continues to expand in the European market through its partnership with Hoffmann-Metalcare in the Netherlands. The move further strengthens the market presence and brand visibility of CHMER wire and die-sink EDM solutions across the Netherlands and wider Flanders region. 

Committed to becoming a world-class leader in non-traditional machining technology solutions, CHMER leverages its expertise in precision machining, smart automation integration, flexible customisation, and energy-efficient manufacturing solutions to support industries including mould and die, aerospace, automotive, medical, semiconductor and precision component manufacturing.  

These capabilities help customers address growing demands for high-precision machining, process integration, and smart manufacturing. 

Through Hoffmann-Metalcare’s local sales consultation, equipment implementation support, and technical services, CHMER is able to stay closer to the European market and better understand customer needs. The partnership also enables more metalworking and manufacturing professionals in the region to discover CHMER’s technological capabilities and the value of its solutions. 

As a business, Hoffmann-Metalcare develops, supplies and maintains production lines with machining and non-machining machines for metalworking companies and the broader manufacturing industry. 

CHMER says it sincerely appreciates Hoffmann-Metalcare’s continued efforts in promoting its brand. Looking ahead, CHMER will continue to strengthen its collaboration with global partners and expand its international presence, providing customers worldwide with advanced, reliable and flexible precision machining equipment, non-traditional machining solutions and localised services. 

More information www.chmer.com 

Getting Closer to the Spark for a Smoother Surface Finish

Advances in microelectronics are improving die-sink EDM performance, with compact generators enabling faster machining, more precise spark control and improved surface finishes. 

Since the 1970s, semiconductor technology has transformed electronic devices, and similar progress is changing EDM. Early generators relied on analogue systems that could produce inconsistent sparks and required skilled operators to maintain precision. Modern systems use feedback-driven pulse management to control spark energy and intensity. 

Generator location is another factor in machining performance, explains Martin Spencer, managing director of United Machining UK: “By keeping generator modules cool and close, today’s die-sinking machines achieve a higher level of thermal and electrical stability.” 

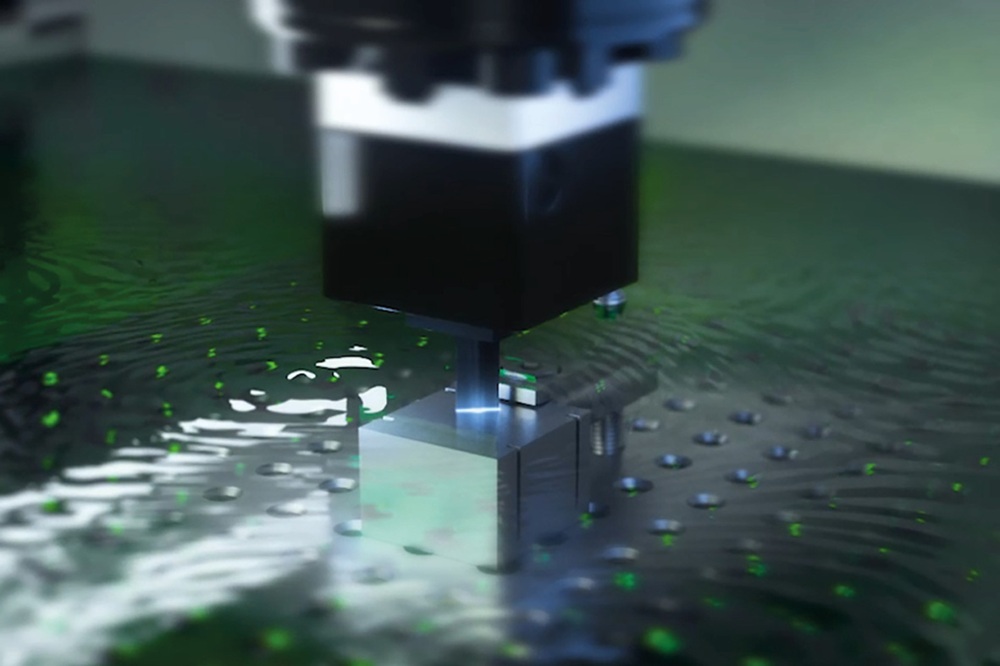
Traditionally, EDM generators were housed in separate cabinets, connected to the spark gap by several metres of cable. Modern, compact designs allow the generator to be positioned much closer to the electrode, shortening the electrical path and reducing inductance and capacitance. 

This enables faster, more precise voltage control, improving erosion rates while limiting heat transfer to the workpiece. The result is a smoother surface finish and a reduced heat-affected zone (HAZ). 

On patented die-sinking EDM platforms, compact, high-speed generators can be mounted directly on the Z axis or behind the rear wall of the work pan, just centimetres from the electrode. For mould manufacturers, this configuration can reduce cycle times by up to 20%, while helping preserve workpiece integrity during finishing operations. 

Further developments are likely to combine hardware advances with increasingly sophisticated control software. Artificial intelligence, digital twins, predictive algorithms and adaptive spark control could deliver further improvements in precision and productivity. 

Ultimately, bringing the generator closer to the spark helps manufacturers gain greater control over the EDM process, with benefits for machining speed, surface quality and dimensional accuracy. 

More information www.machining.com 

Tooling, Automation and Software Specialist Unveils New Website

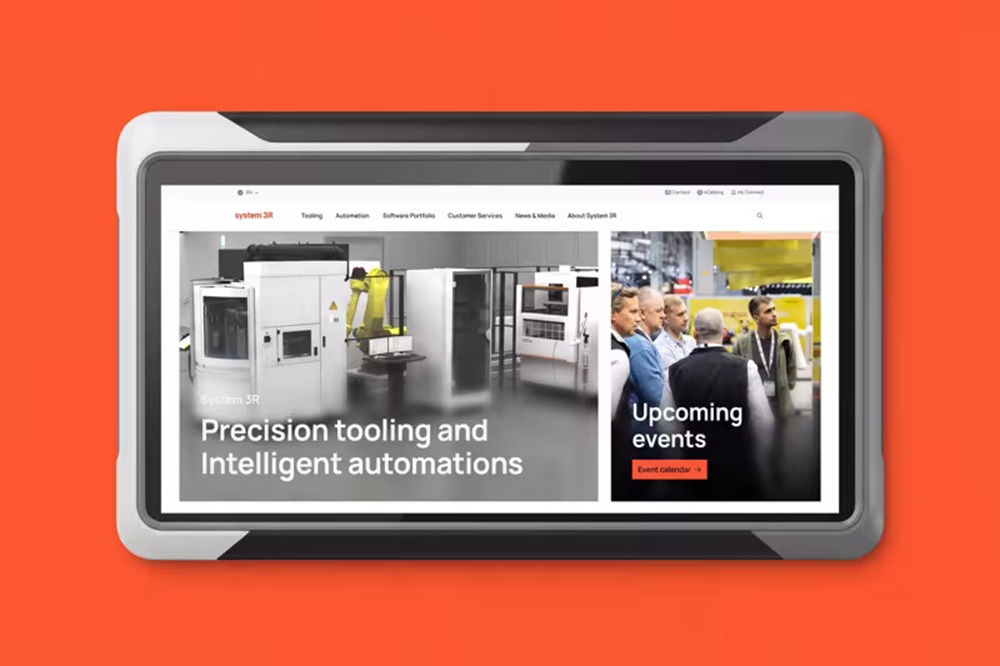
System 3R, which offers extensive solutions for EDM machine work holding and automation, has launched a new website as part of the United Machining Solutions brand strategy, giving each brand its own digital presence and providing access to its products, services and technical expertise. 

The redesigned site features updated navigation to help visitors find information across the System 3R portfolio, including work holding, tooling, automation and production software. 

The portfolio is presented as an integrated manufacturing solution. Notably, the Macro range provides sub-micron repeatability and fast clamping, while the WorkPartner series covers applications from single-machine tending to automated multi-cell production.  

System 3R’s software connects machines and automation systems, providing job management, real-time monitoring and cell communication. The solutions are compatible with machine tools from all manufacturers. 

The website also includes a worldwide locations directory, helping manufacturers in EDM, milling, grinding and additive manufacturing find their nearest System 3R contact, sales partner or service location. 

An events section provides details of upcoming trade shows, enabling visitors to plan attendance and arrange discussions with SYSTEM 3R specialists about work holding and automation technologies. 

Ultimately, the new website reflects System 3R’s focus on connected precision manufacturing, drawing on more than 50 years of experience in work-holding technology. It provides a central point for exploring the company’s solutions, finding local support and keeping up to date with its activities worldwide. 

More information www.system3r.com 

Practical Wire EDM Workshop Draws Notable Crowds

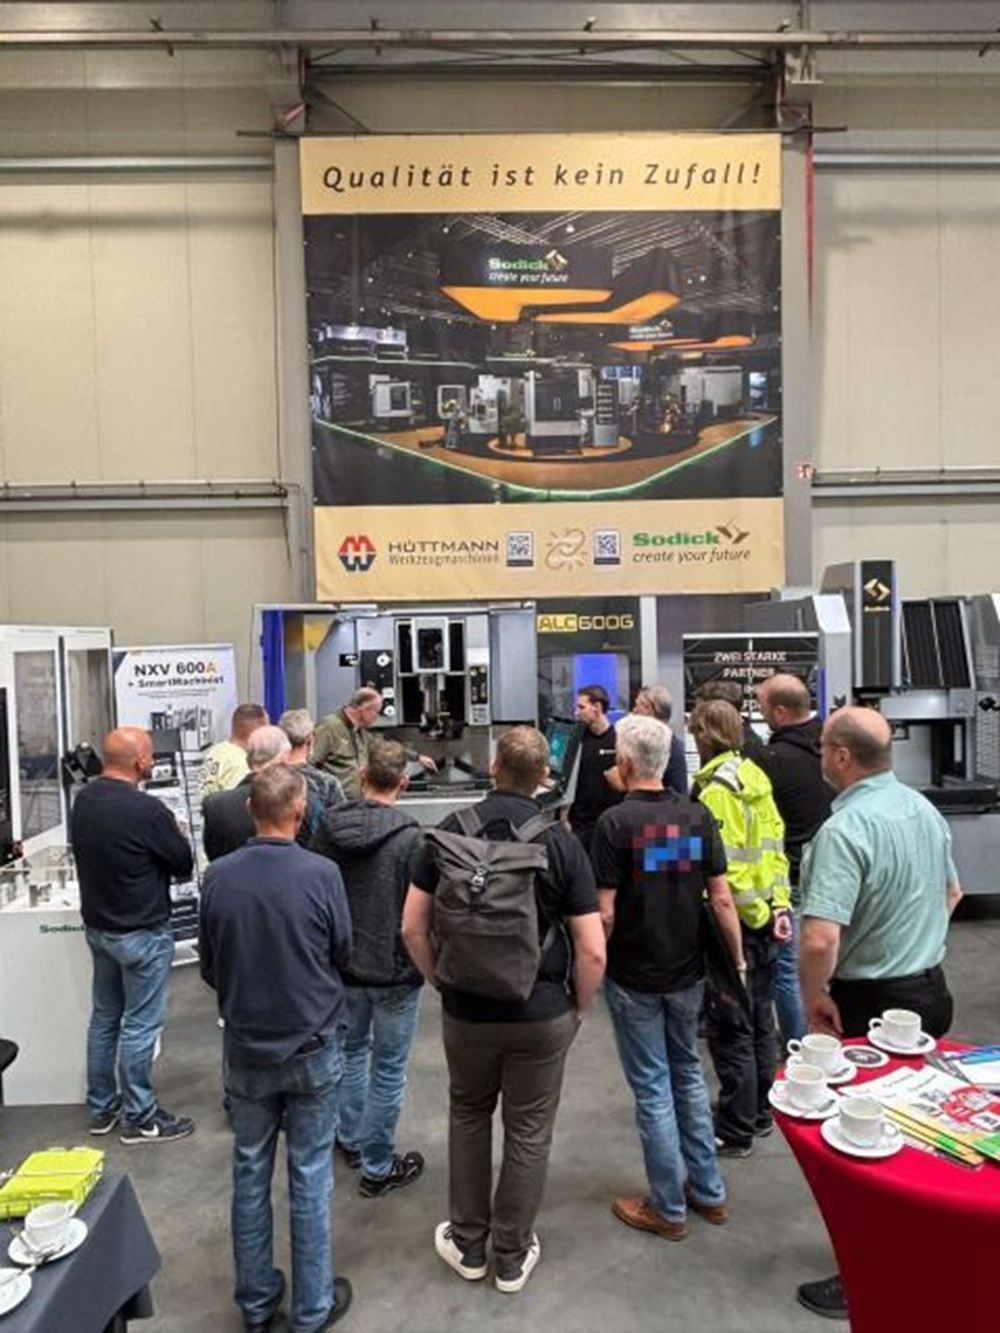
Hüttmann Werkzeugmaschinen GmbH recently hosted a practical wire EDM workshop in partnership with Sodick Deutschland, giving participants the opportunity to explore the technology directly at the machine. 

Concluding earlier this month, the workshop was designed to connect the fundamentals of wire EDM with everyday manufacturing applications. The programme included practical demonstrations, insights into precision and quality, and opportunities to discuss individual application questions with experts. 

In its update from the first day, Hüttmann thanked participants for the lively exchange and highlighted the value of demonstrating wire EDM’s capabilities on the machine itself. This practical approach helps engineers connect what they learn with the challenges and opportunities in their own production environments. 

Based in Soltau, Germany, Hüttmann supplies machine tools and automation solutions, supporting manufacturers in selecting equipment suited to their production requirements. Its range includes Sodick EDM technology, alongside machining and automation equipment.  

For Sodick Europe, events like this demonstrate the value of partners that invest in developing people’s knowledge as well as supplying technology. Introducing new users to wire EDM and helping experienced engineers deepen their understanding can build confidence, encourage questions and reveal new possibilities for manufacturing. 

The collaboration between Hüttmann and Sodick Deutschland brought together equipment, expertise and open discussion, creating a valuable environment for practical learning. 

Sodick Europe thanked both teams for their commitment to sharing knowledge, and all participants for their interest and contribution to the workshop. 

More information www.sodick.eu 

STARRAG S1250 HD SETS NEW BENCHMARK FOR HIGH-SPEED TITANIUM MILLING WITH RECORD METAL REMOVAL RATES

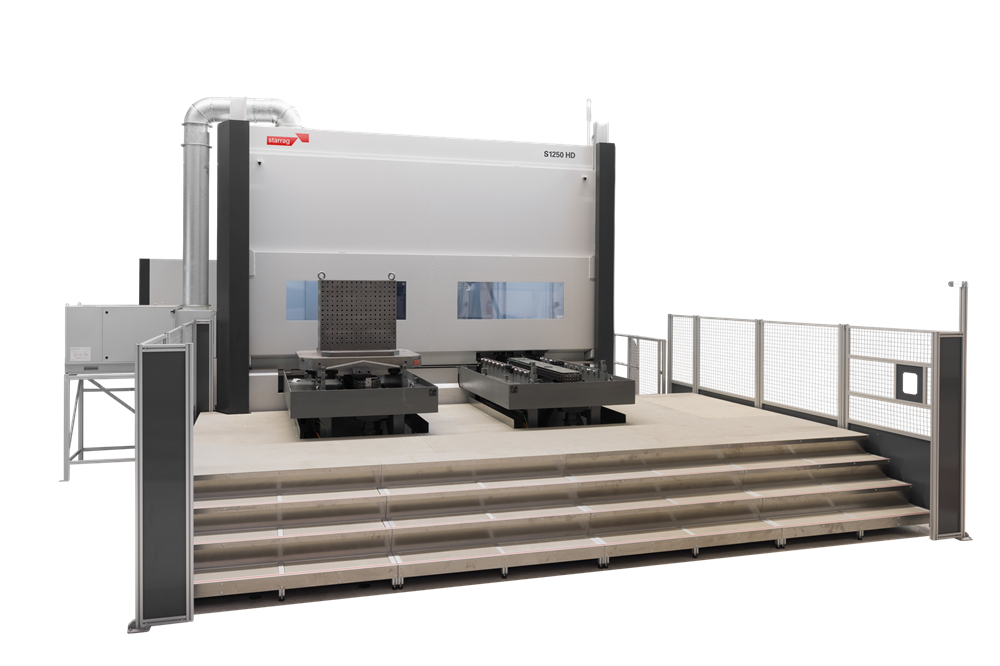
At the EMO 2023 exhibition, Starrag presented a prototype of its hydrostatically guided S1250 HD five-axis machining centre, demonstrating exceptional rigidity and damping that enabled record-breaking cutting parameters in titanium roughing. Initial tests of the current production model have raised the bar further, thanks to a stiffer machine structure, a new high-torque milling head and a geared rotary table. 

For years, Starrag’s STC series has set standards for machining titanium structural components. The material’s low thermal conductivity and poor machinability place heavy demands on cutting tools and limit cutting speeds. Effective roughing therefore relies on low speeds and high torque, requiring a machine with exceptional rigidity and damping. 

To meet these demands, Starrag developed a hydrostatically guided version of its horizontal STC 1250, subsequently named the S1250 HD. Its friction-free, wear-free linear guidance combines high rigidity with effective vibration damping, making the machine suitable for five-axis heavy-duty machining of titanium structures. Tests with the prototype achieved material removal rates up to three times those of the roller-bearing version, while its damping and dynamic performance also delivered precision and surface quality during finishing. 

Airbus recognised the potential after endurance testing the prototype at its Varel site in Germany, ordering five S1250 HD machines with specific modifications to suit its requirements. 

The main changes concerned the rotary table and milling head. “Our customers were impressed by the tests conducted two years ago,” says Alexander Fitz, sales director for aerospace and turbine at Starrag AG. “The Starrag S1250 HD promised considerably more efficient cutting of titanium structural components than ever before. To meet the special requirements of titanium cutting specialists, we decided to make some modifications to the series machine.” 

The standard STC 1250’s direct-drive rotary table was replaced with a geared version better suited to heavy-duty titanium machining. It delivers 25,000 Nm of torque and 32,000 Nm of clamping torque. 

The swivel milling head was also modified to accommodate a more powerful A axis, increasing torque by 50% to 12,000 Nm, with clamping torque of 20,000 Nm. Enlarging the head on one side created the necessary space without compromising workpiece accessibility or the ability to use short tools. 

The machine retains Starrag’s 53 kW geared spindle, which delivers 1600 Nm of torque at speeds up to 4500 rpm. A new HSK-B160 tool interface provides a 160 mm contact diameter to improve tool rigidity, particularly when machining at large cutting depths or with tools featuring substantial overhang. 

Starrag also strengthened the production machine’s structure beyond the prototype specification.  

“Our aim was first and foremost to further increase the possible removal rates and reduce tool wear,” says Rolando Senn, lead designer for hydrostatics. 

The machine beds and columns were reinforced, while the contact surfaces of the hydrostatic guides were enlarged to increase rigidity and damping. Starrag also introduced a mechanical solution to make the hydrostatic guide control system more robust and easier to maintain. 

Initial tests of the production machine have delivered promising results. During a performance cut witnessed by Airbus’s titanium specialists in Rorschacherberg, Switzerland, the machine roughed titanium using an 80 mm Igel milling cutter at a depth of 68 mm in a full cut, with a feed of 80 mm/min and a spindle speed of 160 rpm. The tool reached its capacity limit while the machine ran smoothly, with spindle power consumption at only 60-70%. 

Further tests using Ti6Al4V titanium alloy produced results that Starrag’s milling specialists believe represent a world record for titanium machining. Using a Starrag-developed 40 mm carbide cutter with 18 teeth, the team roughed a titanium block at a cutting speed of 120 m/min, a tooth feed of 0.45 mm, an axial cutting depth of 98 mm and a radial cutting depth of 2 mm. At 955 rpm, the spindle achieved a feed rate of 7735 mm/min and an average undeformed chip thickness of 0.101 mm. 

The resulting metal removal rate was 1516 cm³/min, demonstrating the productivity possible when the machine, tooling and cutting technology are optimised as a complete system. 

The tests also indicated that the cutting tool, rather than the machine, is currently the limiting factor. Starrag therefore plans further trials with its own tools and products from leading tool manufacturers to explore the potential for additional performance gains. 

Looking ahead, the company expects near-net-shape blanks to reduce the amount of roughing required in some applications. Machining complex, deep cavities with tools up to 500 mm long will then become increasingly important. Here, the rigidity provided by the HSK-B160 interface is particularly valuable. Initial tests indicate that vibration-damped tools significantly outperform monolithic alternatives. 

“The structure of our HD machine is also ideally suited to this type of machining,” says Markus Ess, director of technology at Starrag’s HPS business unit. “We’ve built an extremely rigid, high-quality titanium machine, with which we can perform excellent roughing and work in complex cavities with very long tools – a future-proof mix.” 

Reduced tool wear offers another significant benefit. Titanium machining places heavy demands on cutting edges, making tooling a major operating cost. Improved damping can extend tool life, even at higher cutting speeds, helping offset the additional investment in hydrostatic guidance. 

Ess also points to energy savings when measured against output. Although the S1250 HD may consume more power than other machines, shorter machining times can reduce energy use per component and lower the associated carbon footprint. Reduced operating time also cuts the energy consumed by auxiliary systems, including coolant delivery, hydraulics, pneumatics and cooling. 

More information www.starrag.com