FFG Showcases ‘Manufacturing Of Tomorrow’ At AMB 2026

Rising demands for productivity, flexibility and investment security, combined with a dynamic market environment, are creating new challenges for manufacturing companies. What is needed, is not only high-performance machinery, but partners that combine technology, automation and service into cost-effective, integrated solutions – and support manufacturing companies over the long term.   

This is precisely where the Fair Friend Group (FFG) came in at the AMB 2026 exhibition in Stuttgart last month. Under the slogan ‘Stopover’ FFG invited visitors to discover new perspectives for the manufacturing of tomorrow. The ‘Stopover’ represented an opportunity for companies to evaluate technological possibilities, gain new insights and strategically plan the next steps of their manufacturing strategy. 

As a global machine tool and turnkey solutions partner, FFG brings together specialised machine tool companies around the world, combining their technology expertise and know-how across multiple disciplines. Customers benefit from continuous technology transfer within the group as well as international support for delivery, commissioning and service.  

This network provides the foundation for high-performance manufacturing concepts and reliable support across national borders. At AMB, FFG demonstrated – through specific applications and several premieres – how this approach can make the manufacturing of tomorrow cost-effective, flexible and future-ready. 

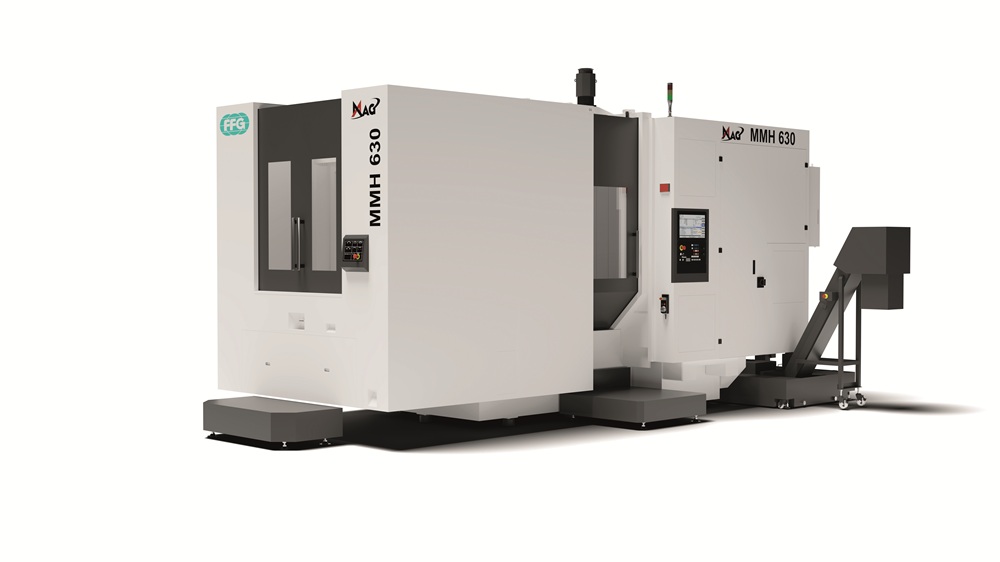
At the show, the new MAG MMH 630 represented a new development for demanding heavy-duty machining applications. Ahead of its official market launch, the company presented the first details of the new machine. 

The MAG MMH 630 was developed for the cost-effective machining of large, complex workpieces and combines high performance, precision and process stability, reports FFG. This blend makes it particularly well suited to applications in industries such as energy, commercial vehicle, heavy equipment and aerospace. 

More information www.ffg-ea.com/en 

Machine Investment Strengthens Plastic Machining Capability

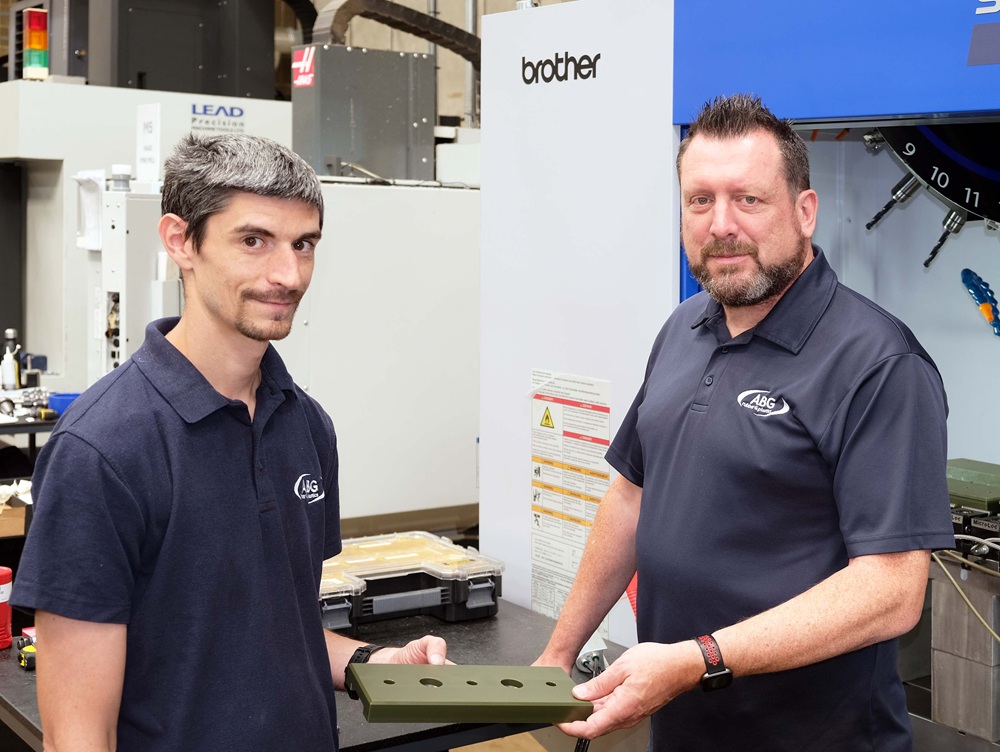
Northampton-based ABG Rubber & Plastics has improved productivity and increased machining capacity by replacing a BT40 vertical machining centre with a compact BT30 Brother Speedio S700Xd2, supplied by Whitehouse Machine Tools. 

The machine is producing precision plastic components for customers across sectors including water, food, rail, automotive and pharmaceuticals. Installed in a single afternoon, it entered full production after just two days of operator training. 

The Speedio’s rapid traverse rates, high acceleration and 1.4-second chip-to-chip tool-change time reduce non-cutting times. Moreover, the machine’s 16,000 rpm spindle also runs at twice the speed of nearly all other machines on ABG’s shop floor, enabling higher material removal rates. As a result, the tool spends around 30% more time cutting than on the previous BT40 machine. 

Early production runs have demonstrated substantial cycle-time reductions on both new and repeat orders, with further improvements expected as program are optimised. 

“The S700Xd2 is not only fast, but also accurate and holds tolerance well, which is primarily down to its rigidity and excellent coolant delivery to the cutting area,” says production manager Anthony Morbey. 

Machining plastics presents particular challenges because their coefficient of thermal expansion is typically around 10 times that of metals, making temperature control essential for maintaining dimensional accuracy. 

Despite its compact footprint, the machine offers a working envelope of 700 x 450 x 380 mm, fitting easily into the space vacated by its predecessor. It also consumes around one-third of the power required by a typical BT40 machining centre, while using less compressed air. 

ABG specialises in precision machining engineering plastics including nylon, acetal, PET, PEEK and PTFE. Its investment in the Speedio supports continued growth as the company prepares to move into a new 23,000 sq ft manufacturing facility. 

More information www.wmtcnc.com 

EXPERIENCING EVERYTHING FROM SIMULATION TO INNOVATION AT VUE 2026

The Vericut Users’ Exchange (VUE) returned to the UK last month and brought customers together for a day of technical insight, awareness, practical CNC machining solutions and knowledge sharing. Prominent among the highlights was a presentation by Stoneswood Precision Components on how Vericut is facilitating innovative processes like interpolation turning to push CNC machining capabilities beyond conventional limits. 

For CNC machine shops, the value of Vericut simulation extends well beyond identifying potential collisions. At VUE 2026, held at the Silverstone Museum adjacent to the world-famous Silverstone Formula 1 Circuit, around 60 attendees explored how Vericut software can support everything from production planning and tooling decisions to the development of advanced machining processes. 

Following breakfast and registration, attendees were welcomed by Gavin Powell, managing director of Vericut UK, before Gavin Bridger, applications engineering manager, opened the technical programme with a presentation entitled: ‘Feature, Future or Fiction: Vericut 9.6, 9.7 and Beyond’. 

An interactive format saw delegates use their phones to vote on whether Vericut capabilities presented by Bridger were current features, planned future developments or pure fiction. With a live leaderboard adding a competitive element, the session proved an entertaining approach. Many attendees were surprised to discover that capabilities such as Vericut Assistant, tool-tip caption pop-ups, verified coolant usage per tool, FANUC TP language support and bidirectional connectivity with Siemens’ Run MyVirtual Machine (RMVM) digital-twin platform, are already available. 

The presentation also offered a glimpse of potential future developments, including cloud-based Vericut, virtual reality (VR) for Vericut, and data management for Siemens’ Teamcenter PLM (Product Lifecycle Management) software platform. 

Jonathan Hollinworth, area sales manager for northern England and Scotland, followed with an overview of Vericut 9.7. He revealed the latest release delivers performance improvements of 10-40%, alongside expanded AI assistance, streamlined workflows and enhancements to tooling management. He also discussed future developments, including reading semantic PMI (Product Manufacturing Information), an embedded Mastercam interface, and direct Vericut connection to the CNC machine (eliminating the need for a third-party connection). 

The day’s keynote presentation came from Tom Whitbread, technical engineer at Cheshire-based Stoneswood Precision Components, part of Hyde Aero Products. Specialising primarily in aerostructures for civil and defence applications, Stoneswood’s programming workflow starts in hyperMILL CAM software, with Icam (part of the Vericut software suite and ecosystem) providing the post-processing before Vericut independently verifies the resulting NC code. 

“We want to show how we’re using Vericut for more than simply checking whether a toolpath is going to collide,” stated Whitbread. “For instance, the simulation provides useful information for production planning, tooling decisions and developing processes that aren’t necessarily supported by a conventional workflow.” 

One notable aspect of Stoneswood’s approach is that its Vericut sessions are built using the same documentation issued to shop-floor operators. Fixture selection, component position, work offsets, tooling assemblies and machine configuration are all checked against the set-up sheet. This strategy provides an independent check of more than the NC code. If the set up documented for the operator does not correspond with the Vericut session, the discrepancy can be investigated before the job reaches the machine. 

The company also uses Vericut’s cycle-time estimates to support production planning. After posting and verifying a program, the simulated manufacturing time is fed back to the planning department, helping inform production scheduling and machine capacity decisions.  

Whitbread highlighted another practical application: reviewing cutting flute engagement. Vericut’s graphical representation enables programmers to assess how much of a solid-carbide tool is engaged in the cut and evaluate changes to axial engagement as part of process development. The focus is on understanding tool engagement and verifying tooling decisions within the digital workflow. 

Stoneswood uses Icam to develop bespoke post-processing functionality for its machine tools. This activity includes controlling specific C-axis table orientations, enabling the company to reposition components and access machining areas that might otherwise exceed the available machine envelope. 

Whitbread illustrated the point with a component approximately 2.3 m long that required machining in a working envelope of around 1.6 m. By controlling table rotations through bespoke post-processing, the company could access the required length while working within the machine’s physical limitations. Vericut then independently simulated the resulting machine behaviour. It was close, but perfectly safe, providing complete peace of mind for Stoneswood. 

The presentation by Whitbread also covered the use of gear-driven and coolant-driven angled heads for hole-making, with Vericut representing the complete assemblies to verify access, orientation and collision risks. 

However, it was interpolation turning that provided the most striking example of Stoneswood’s efforts to extend its manufacturing capabilities. 

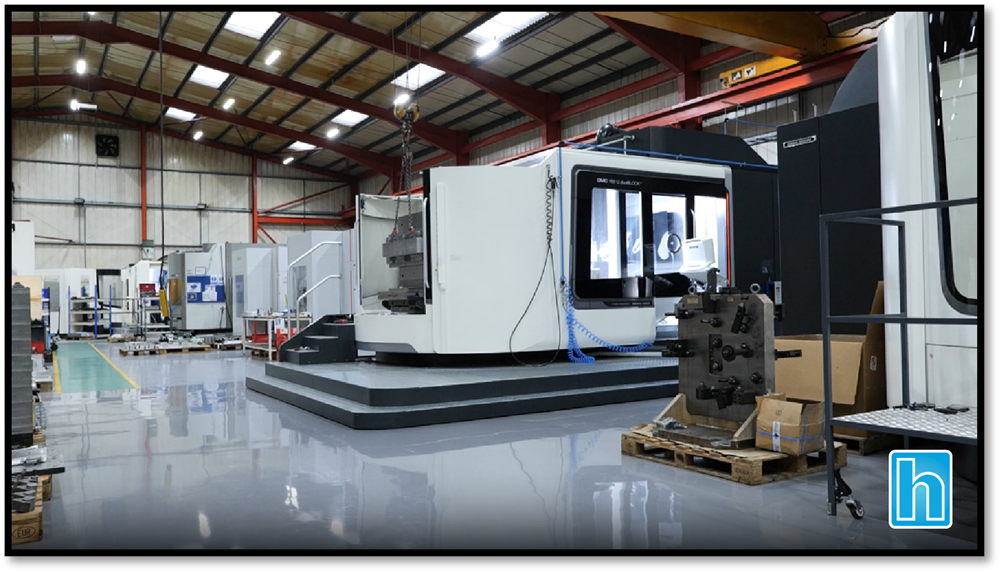
Available on the company’s DMG Mori DMC series machining centres, interpolation turning enables the production of turned features through co-ordinated machine movement, rather than transferring the component to a conventional turning operation. The challenge was not simply making the machines perform the process. Stoneswood wanted to integrate interpolation turning into the same controlled digital workflow used for its conventional machining operations. 

Said Whitbread: “It’s one thing to know that the machine can perform a particular function. It’s another to make sure we can program it, post-process it and independently verify what the machine’s going to do before we press start.” 

To achieve this, Stoneswood used hyperMILL’s general turning functionality to create the required toolpaths. Using Icam, the company then developed bespoke post-processing logic to translate the output and utilise DMG Mori’s CYCLE806 functionality, producing the machine-specific NC code. 

The next step was to develop the Vericut environment so it could interpret the posted code and accurately reproduce the interpolation turning process on both machine configurations. 

The result is a workflow that follows the same sequence as conventional machining. Rather than relying on the first physical machining cycle to confirm that the specialist functionality works as intended, Stoneswood can now evaluate the process digitally before it reaches the shop floor. 

“That’s the real outcome for us,” stated Whitbread. “We haven’t just made interpolation turning possible on the machine; we’ve brought it into a process where we can understand and prove the behaviour before manufacturing begins.” 

After lunch, attendees had the opportunity to tour the Silverstone Museum with a free pass courtesy of Vericut UK before returning for a demonstration of the latest Icam Post V27, delivered by Bridger. 

The latest release includes AI-powered assistance, regression testing and enhanced debugging tools designed to support post-processor development and validation. The demonstration highlighted how the software can help teams compare NC output, investigate changes and maintain reliable machine-specific code. 

Bridger also provided an informative Vericut ‘Tips & Tricks’ presentation, before the event concluded with round tables led by Vericut experts, providing attendees with an opportunity to discuss their own challenges and exchange practical knowledge. 

Ultimately, every VUE event is about bringing the Vericut community together to share experiences, explore possibilities and learn from industry peers. The Stoneswood presentation in particular was a great example of how customers are using Vericut in innovative ways, perhaps providing attendees with ideas they could take back to their own manufacturing operations. 

More information www.vericut.com/en-gb 
United Machining Unveils New Mikron Mill Machining Centre

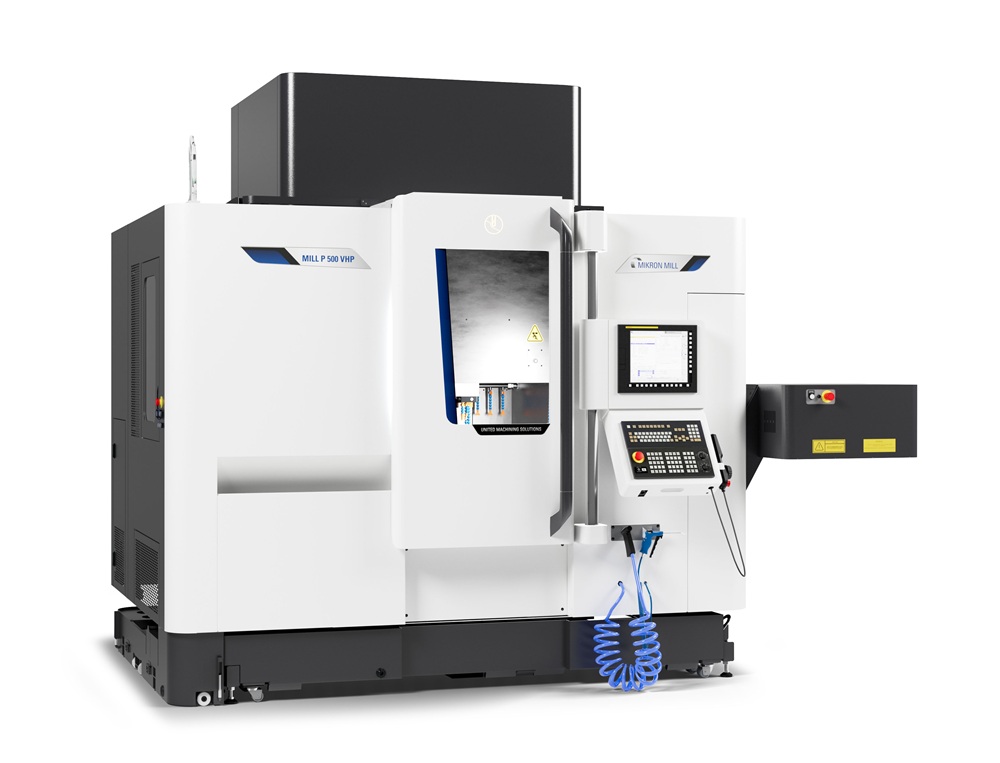
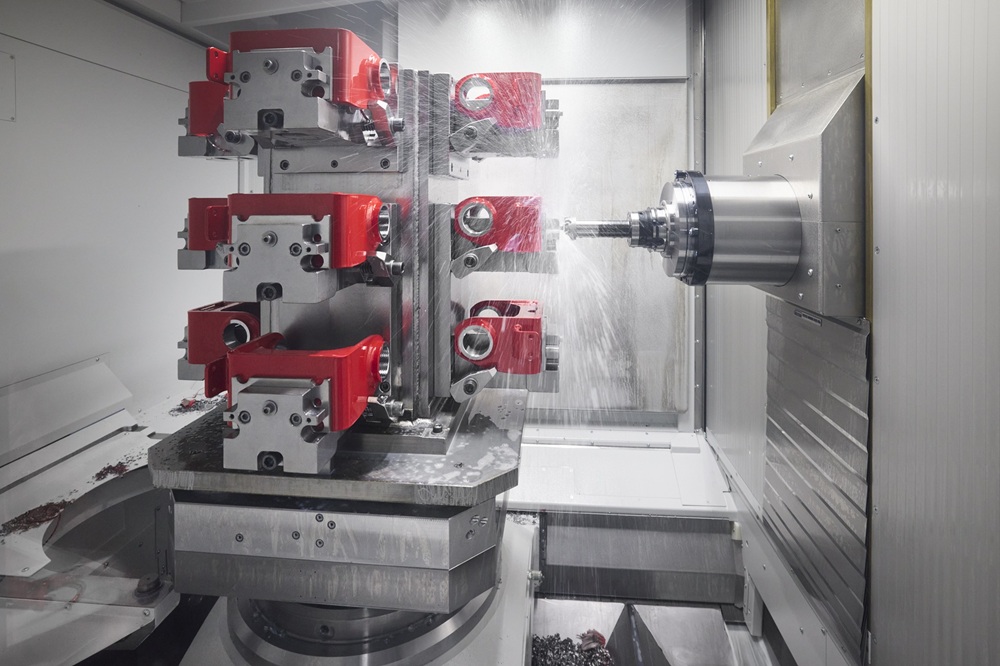
The new three-axis high-precision Mikron Mill P 500 VHP machining centre from United Machining is designed for demanding mould tool manufacturing. Thanks to its linear direct-drive design, the machine achieves accuracies critical for producing high-precision micro-components used typically in the information and communications technology (ICT) sector. 

Competing machines traditionally use ballscrew technology, which can negatively impact surface quality/surface finish due to backlash issues. The VHP’s polymer concrete machine bed, with its damping properties, reduces vibrations in support of high precision. 

Optimal force distribution and long-term thermal stability arrive courtesy of the machine’s symmetric portal design. Complementary smart technologies include Intelligent Thermal Control (ITC), Operator Support System (OSS) and Step-Tec Opticool/CoolCore spindles, which can operate at up to 42,000 rpm. Together, United Machining says these features guarantee high process reliability – essential for when the machine is operating continuously and subject to prolonged machining runs. 

The P 500 VHP’s precision and performance make it suited to the machining of high-quality mould inserts for lenses or connectors used in the ICT sector. However, applications extend to other industries: from reflector moulds for automotive or household appliances to fuel cell tools and medical device moulds. In fact, anywhere where extreme accuracies and superior surface finishes are required. 

“The intelligent automation concept with rear-loading enables significant productivity gains, while the machine’s compact footprint allows space-efficient integration into a range of different environments,” says Juan Martin, head of customer development at United Machining. 

According to United Machining, the Mikron Mill P 500 VHP offers exactly what modern manufacturers need to remain competitive: reliable precision combined with high productivity. 

More information www.machining.com

New Heckert H75 Production System Guarantees Productivity Edge

Agricultural machinery manufacturer Pöttinger has replaced an ageing flexible production system with four Heckert H75 horizontal machining centres from Starrag, integrated with automation from Promot. The complete system was installed and commissioned in just 12 weeks, while minimising disruption to ongoing operations. 

Based in Grieskirchen, Austria, Pöttinger manufactures equipment for grassland management, farming and digital agriculture. Its products are customised, making flexible manufacturing essential. Components range from small structural steel parts weighing around 300 g to gearbox housings weighing 27 kg, with some requiring micrometre-level accuracy. 

The company selected the Heckert H75 for its combination of precision, rigidity, energy efficiency and generous working envelope, despite a compact footprint. Promot integrated the four machines with a five-level, 134-position pallet storage system and a master computer linked to SAP. 

A key advantage is the shared tool management system. Each machine has a 260-position tool magazine, with Promot’s gantry loader enabling the exchange of tools between all four machines. This capability provides access to 1040 tools and allows production control to allocate components to whichever machine is available. 

Meeting the demanding 12-week installation deadline required extensive preparation. Starrag supplied digital twins of the machining centres, while Pimpel’s CHECKitB4 software enabled the simulation and checking of NC programs before installation. Pöttinger programmers also tested machining operations on the actual machines at Starrag’s Chemnitz factory in Germany. 

Further productivity gains came from moving workpiece cleaning outside the machine. While a completed component undergoes cleaning at a dedicated set-up station, machining can continue on the next part. This workflow saves at least one minute per pallet change, equivalent to almost 20% of the cycle time. 

Pöttinger can manage the four identical machines as a single production resource, allowing the flexible distribution of orders.  

More information www.starrag.com