Getting Closer to the Spark for a Smoother Surface Finish

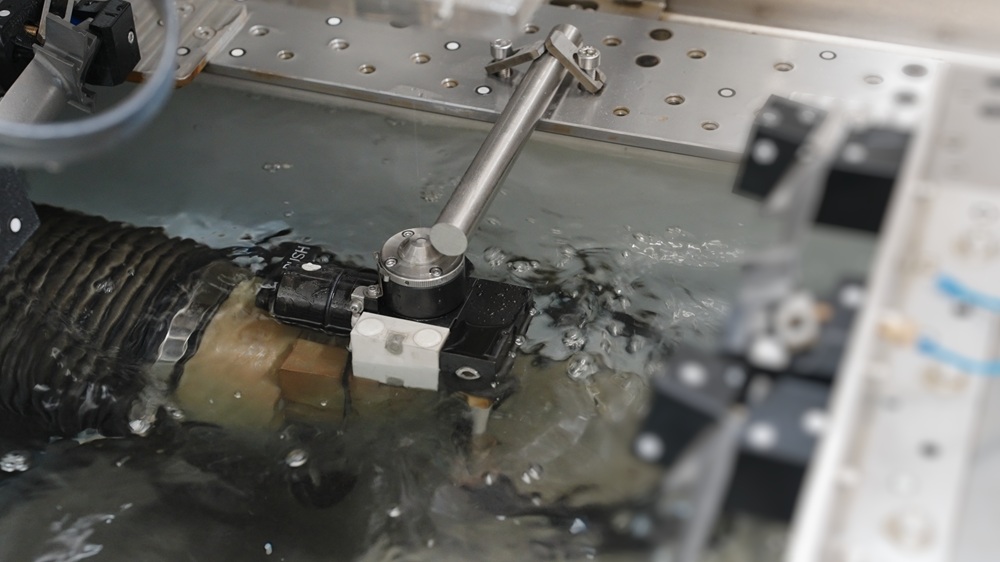
Advances in microelectronics are improving die-sink EDM performance, with compact generators enabling faster machining, more precise spark control and improved surface finishes. 

Since the 1970s, semiconductor technology has transformed electronic devices, and similar progress is changing EDM. Early generators relied on analogue systems that could produce inconsistent sparks and required skilled operators to maintain precision. Modern systems use feedback-driven pulse management to control spark energy and intensity. 

Generator location is another factor in machining performance, explains Martin Spencer, managing director of United Machining UK: “By keeping generator modules cool and close, today’s die-sinking machines achieve a higher level of thermal and electrical stability.” 

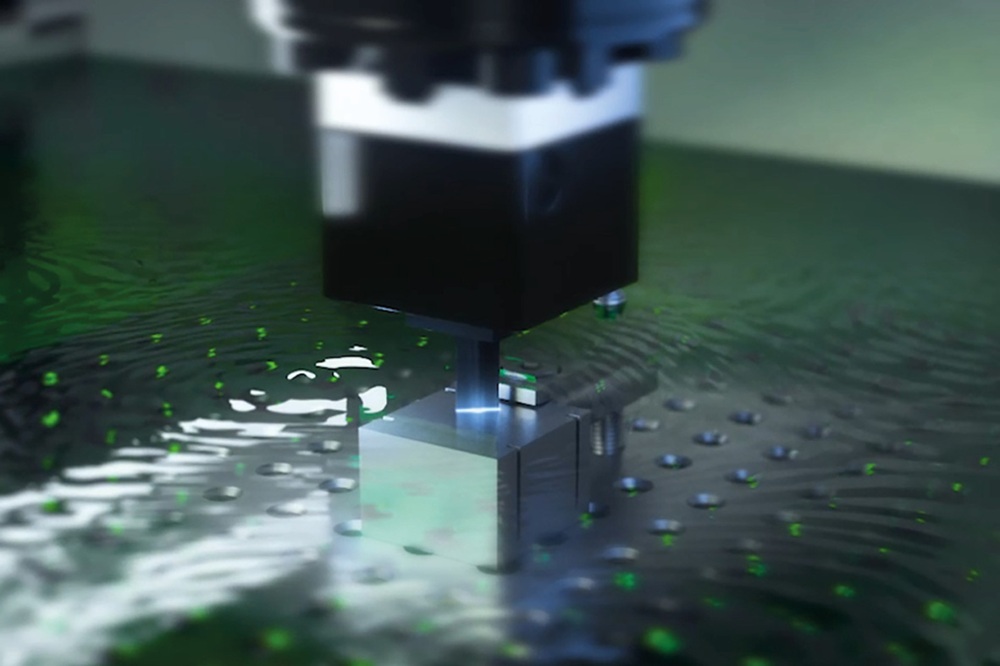
Traditionally, EDM generators were housed in separate cabinets, connected to the spark gap by several metres of cable. Modern, compact designs allow the generator to be positioned much closer to the electrode, shortening the electrical path and reducing inductance and capacitance. 

This enables faster, more precise voltage control, improving erosion rates while limiting heat transfer to the workpiece. The result is a smoother surface finish and a reduced heat-affected zone (HAZ). 

On patented die-sinking EDM platforms, compact, high-speed generators can be mounted directly on the Z axis or behind the rear wall of the work pan, just centimetres from the electrode. For mould manufacturers, this configuration can reduce cycle times by up to 20%, while helping preserve workpiece integrity during finishing operations. 

Further developments are likely to combine hardware advances with increasingly sophisticated control software. Artificial intelligence, digital twins, predictive algorithms and adaptive spark control could deliver further improvements in precision and productivity. 

Ultimately, bringing the generator closer to the spark helps manufacturers gain greater control over the EDM process, with benefits for machining speed, surface quality and dimensional accuracy. 

More information www.machining.com 
Tooling, Automation and Software Specialist Unveils New Website

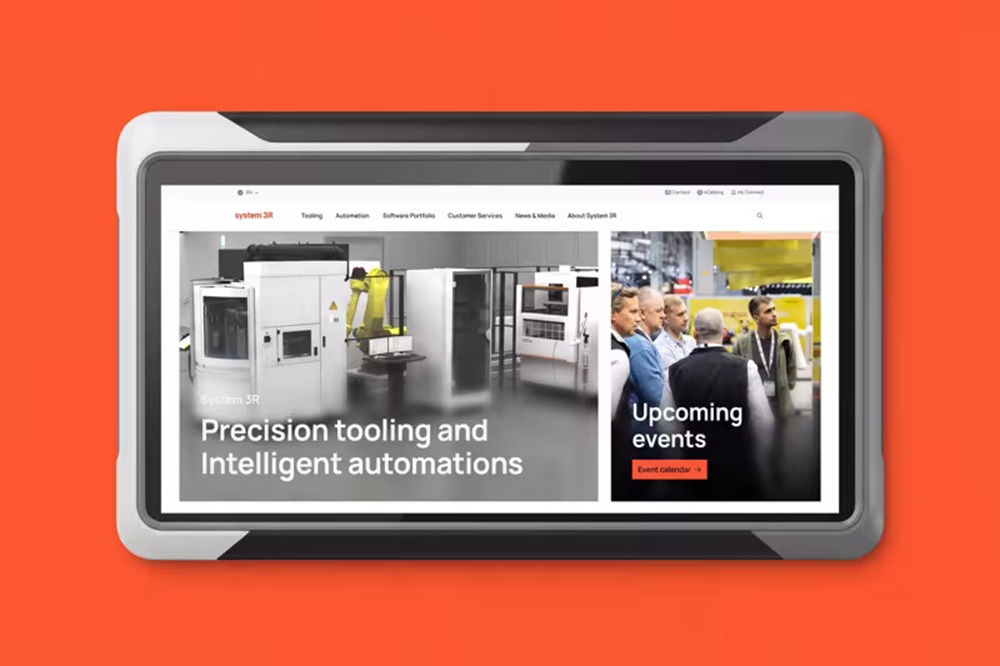
System 3R, which offers extensive solutions for EDM machine work holding and automation, has launched a new website as part of the United Machining Solutions brand strategy, giving each brand its own digital presence and providing access to its products, services and technical expertise. 

The redesigned site features updated navigation to help visitors find information across the System 3R portfolio, including work holding, tooling, automation and production software. 

The portfolio is presented as an integrated manufacturing solution. Notably, the Macro range provides sub-micron repeatability and fast clamping, while the WorkPartner series covers applications from single-machine tending to automated multi-cell production.  

System 3R’s software connects machines and automation systems, providing job management, real-time monitoring and cell communication. The solutions are compatible with machine tools from all manufacturers. 

The website also includes a worldwide locations directory, helping manufacturers in EDM, milling, grinding and additive manufacturing find their nearest System 3R contact, sales partner or service location. 

An events section provides details of upcoming trade shows, enabling visitors to plan attendance and arrange discussions with SYSTEM 3R specialists about work holding and automation technologies. 

Ultimately, the new website reflects System 3R’s focus on connected precision manufacturing, drawing on more than 50 years of experience in work-holding technology. It provides a central point for exploring the company’s solutions, finding local support and keeping up to date with its activities worldwide. 

More information www.system3r.com 

Excetek Wire EDM Offers Leap in productivity And Efficiency

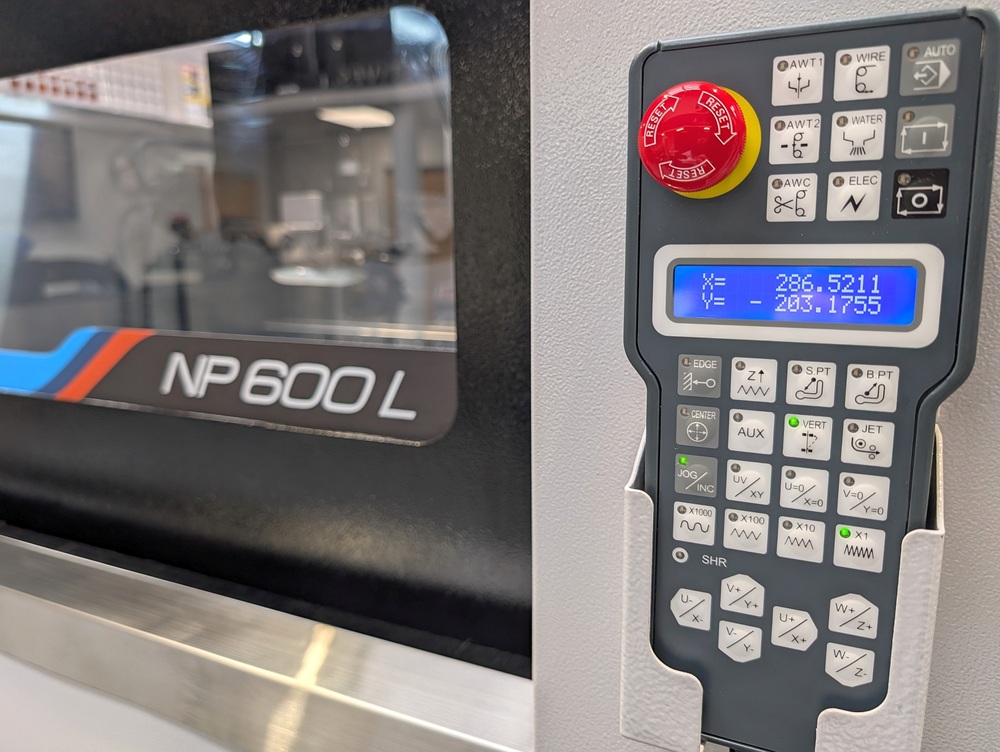
The new Excetek NP Plus series of CNC wire EDM machines, supplied exclusively in the UK by Warwick Machine Tools, combines energy-saving technology with faster machining and onboard power consumption monitoring. 

The machines feature high-precision linear motors, a ‘Green Sparking’ generator, low-energy pumps and an inverter-controlled water chiller. Together, these systems reduce power consumption by up to 35%, while increasing machining speed by up to 25%. 

The Green Sparking generator uses an energy recovery system and high-speed discharge pulses to improve efficiency. ‘ECO Mode’ optimises fine finishing, reducing the number of machining passes required while improving surface accuracy. The generator achieves surface finishes of Ra 0.5 in three cuts and Ra 0.3 in five, compared with Ra 0.7 and Ra 0.35 respectively for the previous generator. 

Automatic compensation for brass wire wear helps reduce wire consumption, while peripheral systems operate only when required to limit unnecessary energy use. 

“A 35% reduction in energy consumed adds up,” says Paul Barry, technical manager at Warwick Machine Tools. “Over a year it represents an annual carbon emissions reduction of 4310 kg and electricity saving of almost 9000 kWh.” 

An onboard monitoring system records real-time electrical data and provides daily and monthly consumption reports, carbon emissions calculations and energy trend charts. It also logs energy use for individual NC machining processes, converting consumption into cost data to help businesses assess operating costs. 

The NP600L Plus model features a fixed worktable, with the linear motors moving the gantry and wire feed. This configuration accommodate workpieces weighing up to 800 kg. According to Barry, cutting speed can be increased by 25% without compromising volumetric accuracy or repeatability, both specified at better than ±2 microns. 

More information www.warwickmachinetools.co.uk

Practical Wire EDM Workshop Draws Notable Crowds

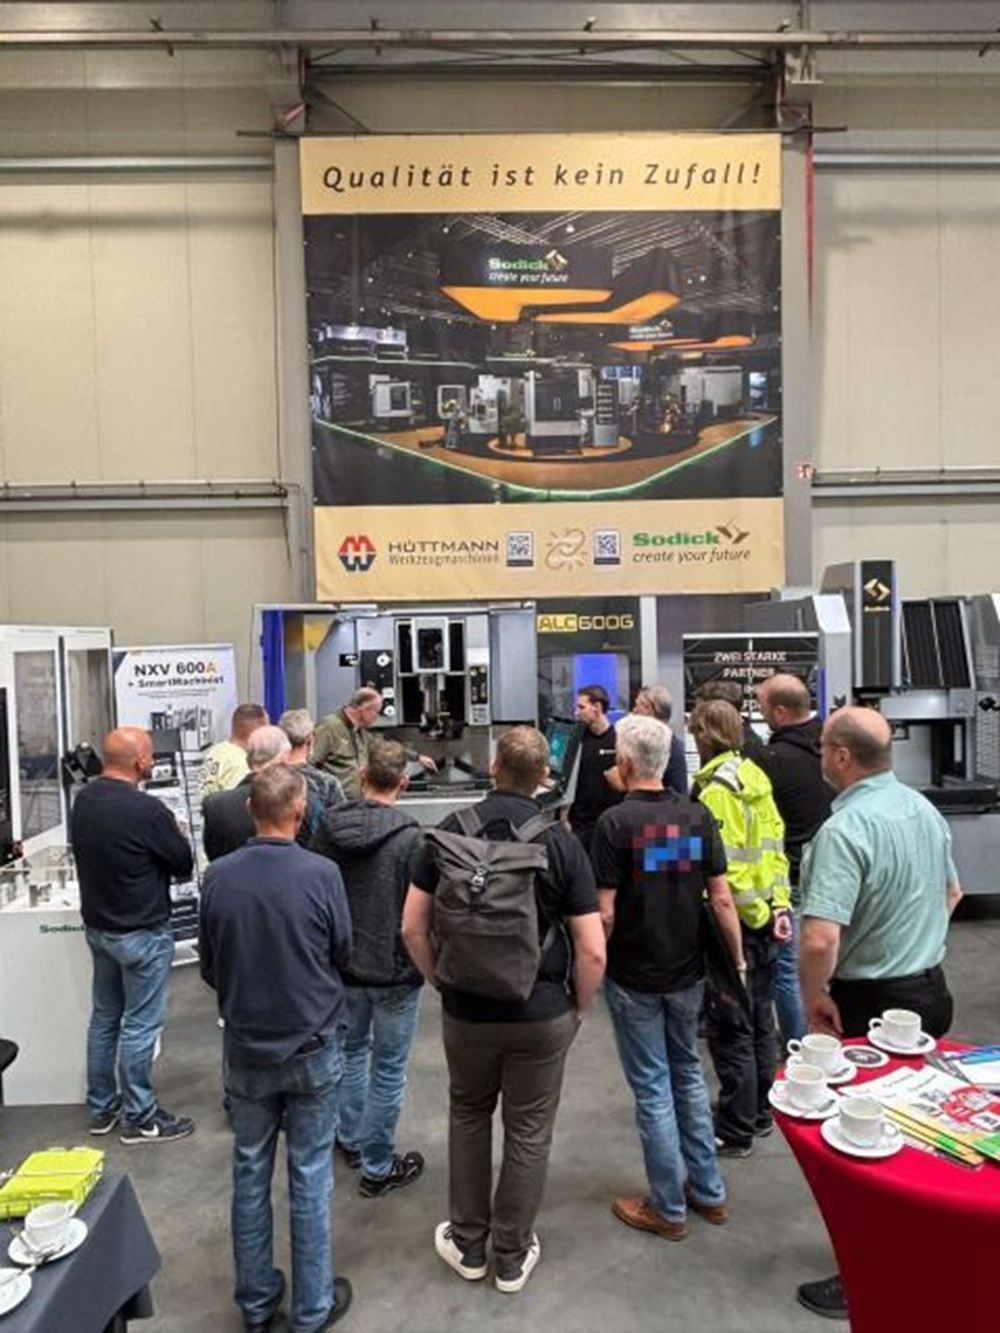
Hüttmann Werkzeugmaschinen GmbH recently hosted a practical wire EDM workshop in partnership with Sodick Deutschland, giving participants the opportunity to explore the technology directly at the machine. 

Concluding earlier this month, the workshop was designed to connect the fundamentals of wire EDM with everyday manufacturing applications. The programme included practical demonstrations, insights into precision and quality, and opportunities to discuss individual application questions with experts. 

In its update from the first day, Hüttmann thanked participants for the lively exchange and highlighted the value of demonstrating wire EDM’s capabilities on the machine itself. This practical approach helps engineers connect what they learn with the challenges and opportunities in their own production environments. 

Based in Soltau, Germany, Hüttmann supplies machine tools and automation solutions, supporting manufacturers in selecting equipment suited to their production requirements. Its range includes Sodick EDM technology, alongside machining and automation equipment.  

For Sodick Europe, events like this demonstrate the value of partners that invest in developing people’s knowledge as well as supplying technology. Introducing new users to wire EDM and helping experienced engineers deepen their understanding can build confidence, encourage questions and reveal new possibilities for manufacturing. 

The collaboration between Hüttmann and Sodick Deutschland brought together equipment, expertise and open discussion, creating a valuable environment for practical learning. 

Sodick Europe thanked both teams for their commitment to sharing knowledge, and all participants for their interest and contribution to the workshop. 

More information www.sodick.eu 

NCMT and Delta Redefine Metrology Capability With Makino EDM

Delta XD has expanded its metrology capabilities with a Makino U6 H.E.A.T. wire EDM supplied by NCMT, enabling the business to section complex aerospace components with minimal material loss and greater accuracy. 

The specialist inspection company needed a way to examine internal geometries and material integrity without compromising the features undergoing measurement. Previously, multiple cuts or outsourced processes could add time and complexity to inspections. 

“We had a very specific requirement to support a customer in sectioning some finely detailed turbine components for quality control purposes,” says Lee Griffiths, head of sales & business development at Delta XD. “The need to split parts very precisely, without losing material, was a key focus for us.” 

The Makino U6 H.E.A.T. combines cutting accuracy of 4 microns with the ability to use wire down to 0.1 mm in diameter, minimising kerf width and preserving material for analysis. Its larger working envelope accommodates both intricate components and larger castings, while high-energy pulse technology improves cutting efficiency, surface quality and wire life. 

The machine also enables Delta XD to combine 3D scanning with adaptive machining, creating complex 3D cutting paths to expose internal features for inspection.  

Installation was equally straightforward. With a machine already available at NCMT’s Coventry showroom, the period from purchase order to installation, including training, was around 10-15 days. 

The investment is already delivering results. High machine utilisation and growing enquiries reflect demand for the new service, while reducing multiple cuts to a single operation cuts reconstruction work and inspection times. 

“The overall time to complete inspections is much reduced, and the amount of data we can present is greater because we’re seeing more of the part in its original state,” reports Daniel Lainchbury, COO at Delta XD. 

More information www.ncmt.co.uk