ER HP Collet Chucks Elevate Standard For High-Speed Milling

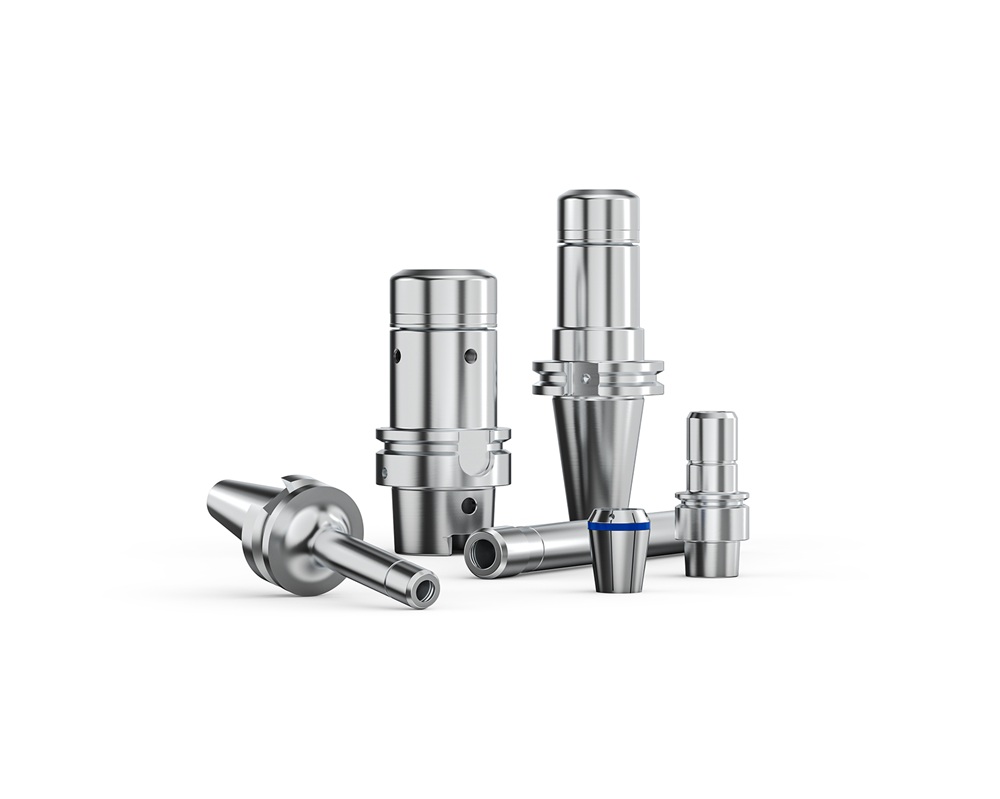
Engineered for high-speed milling and five-axis machining, Seco has enhanced the company’s ER HP collet chuck range. Now offering a finely balanced, rigid design, the ER HP delivers smoother finishes, longer tool life and unmatched reliability, reports Seco. 
 

With reference for tool clamping in demanding applications, the new ER HP collet chuck is designed to address the challenges of modern machining where tool slippage, vibration and unreliable clamping can lead to costly downtime and wasted material.  

With high levels of run-out accuracy and a robust, symmetrical build, Seco says its ER HP ensures consistent results, reduced tooling costs and faster cycle times. The high clamping force and secure grip of the collet chucks provide process security even during heavy-duty operations, while the intuitive roller key system makes setup quick, safe and accessible for every team member. 
 
Implementing the ER HP collet chuck is quick, safe and straightforward. Unlike complex tool-holder systems that require specialised training or risky set ups, the ER HP uses a simple roller key for installation, making changeovers fast for minimal downtime. 
 
“Our ER HP collet chuck is all about giving manufacturers the confidence to push their processes further without sacrificing precision or reliability,” explains Yves Heitz, global product manager for machine solutions at Seco. “By combining fine balancing, high clamping force and easy implementation, we’re helping our customers achieve smoother finishes, longer tool life and greater sustainability in their daily operations.”  

More information www.secotools.com 
One Set Up, Hours Saved, Using Nikken Rotary Table With Trunnion

Manufax Engineering is a UK precision engineering company specialising in high-quality CNC machining for demanding sectors including defence, aerospace, medical and industrial manufacturing. With expertise in complex components and precision machining, the company continually invests in advanced manufacturing technologies to improve quality and efficiency.  

For one defence application involving precision tube machining, Manufax relied on manually indexing components between operations. The process was time-consuming, introduced additional set ups, and increased the potential for scrap and material waste. The business wanted a solution that would improve accuracy, reduce set-up time and create greater manufacturing flexibility for future work.  

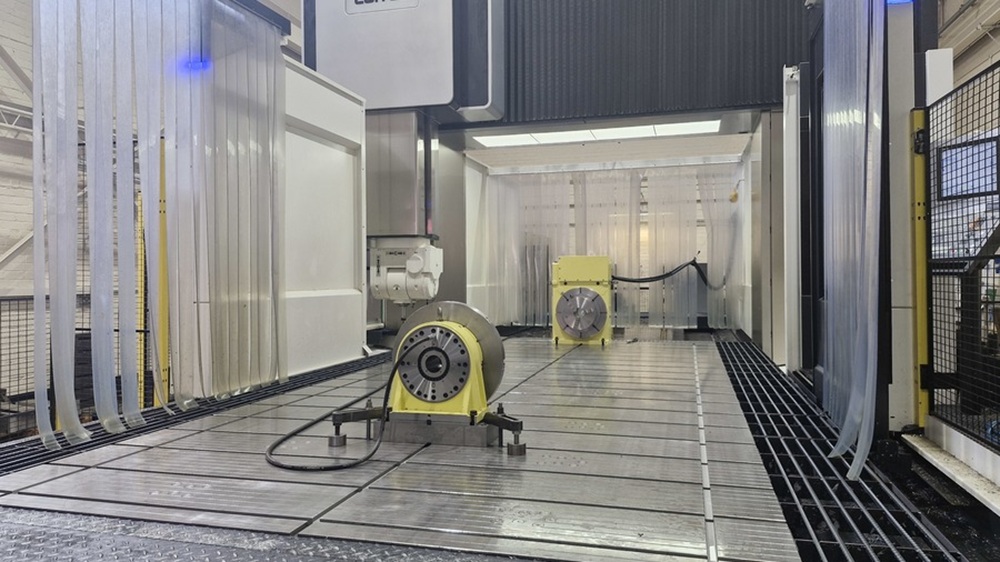
Manufax invested in a Nikken CNC501 rotary table with trunnion, enabling the completion of complex machining operations in a single set up, specifically for the company’s defence application. The improvements have transformed the machining process. Completing components in a single set up has improved accuracy and repeatability, while reducing scrap and raw material costs.  

Each operation now saves between eight and 10 hours of machining time, delivering substantial productivity gains and increasing manufacturing capacity. Beyond the immediate application, the additional fourth-axis capability has opened opportunities to secure new work while giving the business greater flexibility for future projects.  

Alongside the equipment itself, Manufax also highlights the support provided by the Nikken team.  

“Honesty is key, even when things don’t go fully to plan,” says a company representative. “The NIKKEN team has been fantastic throughout. The engineers know exactly what they’re doing, and whenever we need support, they’re there.”  

For Manufax, the combination of reliable technology, responsive support, and long-term partnership made Nikken the natural choice.  

More information www.nikken-world.co.uk 

Clever Work Holding Helps One Machinist Operate Many Mills

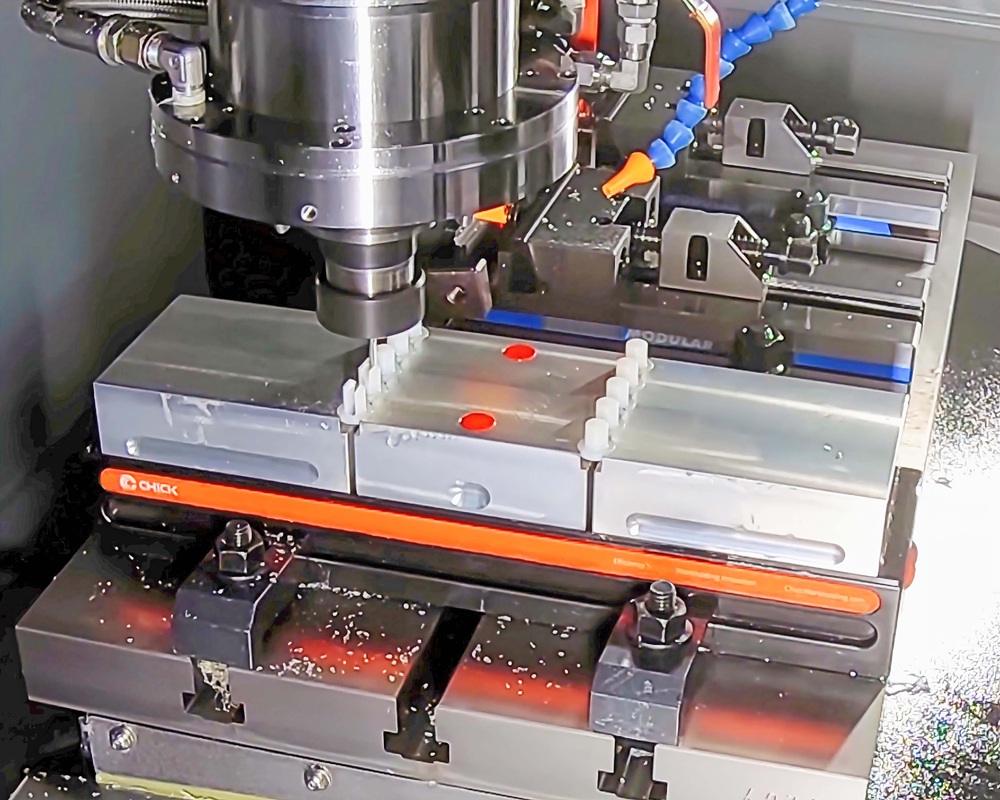
Wimborne-based RPH Manufacturing produces more than 45,000 components annually across 98 part varieties, with owner Richard Haim operating 14 machine tools single-handedly. Helping him maximise productivity are Chick QwikLOK twin-station clamps, supplied by UK distributor 1st Machine Tool Accessories. 

Typically, eight to 10 components are secured simultaneously using aluminium jaws machined to match their profiles. A single handle moves two jaws towards a central fixed jaw, balancing opposing forces and providing a consistent reference point. The jaws also generate a pull-down action for rigid work holding. 

“The best thing about these clamps is their repeatability of positioning to within 10 to 15 microns, better than the 20 microns that the US work-holding equipment manufacturer specifies in its literature,” says Haim. “So every part we machine comes off perfect.” 

By machining multiple components in one cycle, Haim reduces tool-change overheads and can leave machines running while undertaking other production tasks. Combined with the Patterns feature in Hurco’s MAX conversational control, the system makes programming repetitive operations straightforward. 

“For example, at the control I can program a slot mill to machine one part and then tell it to step and repeat the same operation across all of the components, simply by creating a Pattern block to define the X,Y location of each of them on a grid,” he explains. 

The clamps also accommodate larger individual components requiring high clamping forces, including a tapered cylindrical manifold held on just 3 mm of material. 

RPH uses Chick work holding to manufacture 14 of the metal and plastic components in its own 74-piece Parallel Lock kit, developed to keep parallels in position when closing a machine vice. 

More information www.1mta.com 

Vice Automation System From Schunk Lowers Barrier To Entry

Schunk has introduced a new vice automation system designed to make automated machine loading and unloading straightforward, cost-effective and reliable. Combining precise positioning and clamping with simple robot programming, the solution offers manufacturers an accessible entry point into automated machine tending, extending machine running times without additional staffing. 

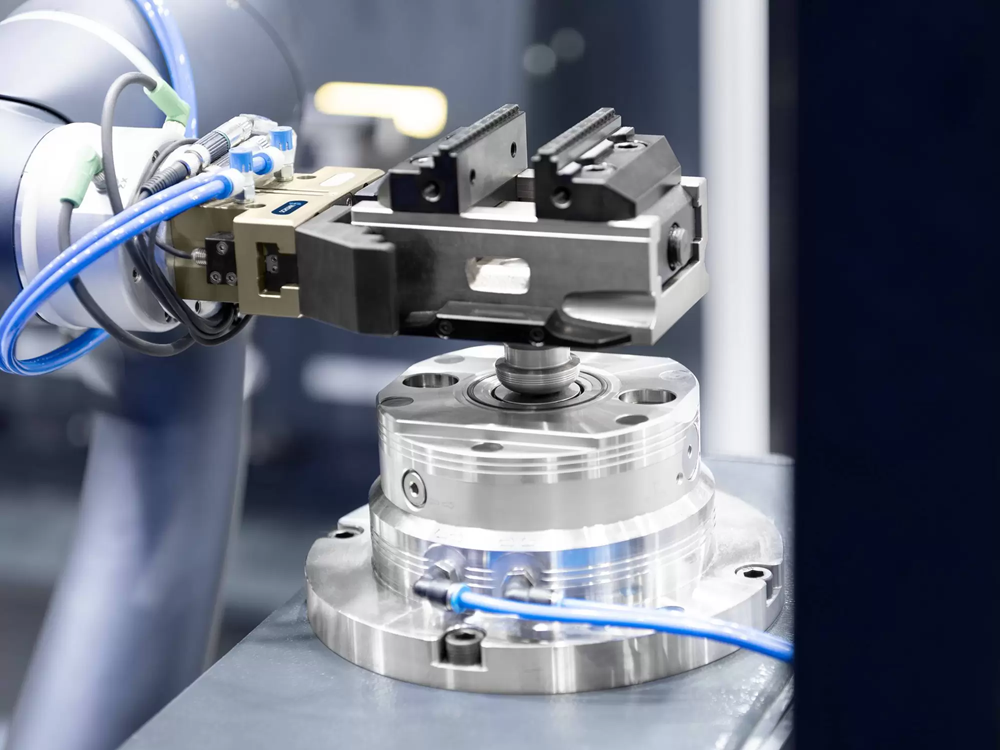
The system is based on a simple concept. Operators manually clamp workpieces into specially prepared vices outside the machine before placing them in a storage rack. A robot fitted with dedicated gripping fingers transfers each vice to a raised Schunk Vero-S 1-way clamping station on the machine table. After machining, it returns the vice and workpiece to the rack. Re-clamping for underside machining can take place inside or outside the storage area. 

At the heart of the system, the console-mounted Vero-S station provides a defined interface between the robot and machine tool. High pull-down forces and the quick-change pallet system’s precision interface ensure repeatable positioning and secure clamping in a single operation. The raised design also provides access for five-sided machining, while the clamping device covers the pallet module to prevent chip accumulation and maintain process reliability. 

Importantly, the operator retains control of the clamping process, while the robot handles the complete vice. Using a consistent interface and fixed positions simplifies programming to point-to-point movements, reducing integration complexity. With no requirement for a media supply on the machine side, the system can be used with virtually any machine tool. 

By preparing multiple vices before the end of a shift, operators can enable unattended machining beyond normal working hours. Standardised components, straightforward integration and relatively low capital expenditure make the system an attractive option for manufacturers looking to increase productivity through automation. 

More information www.schunk.com 

Automated Jaw Opening For Autonomous, High-Mix Machining

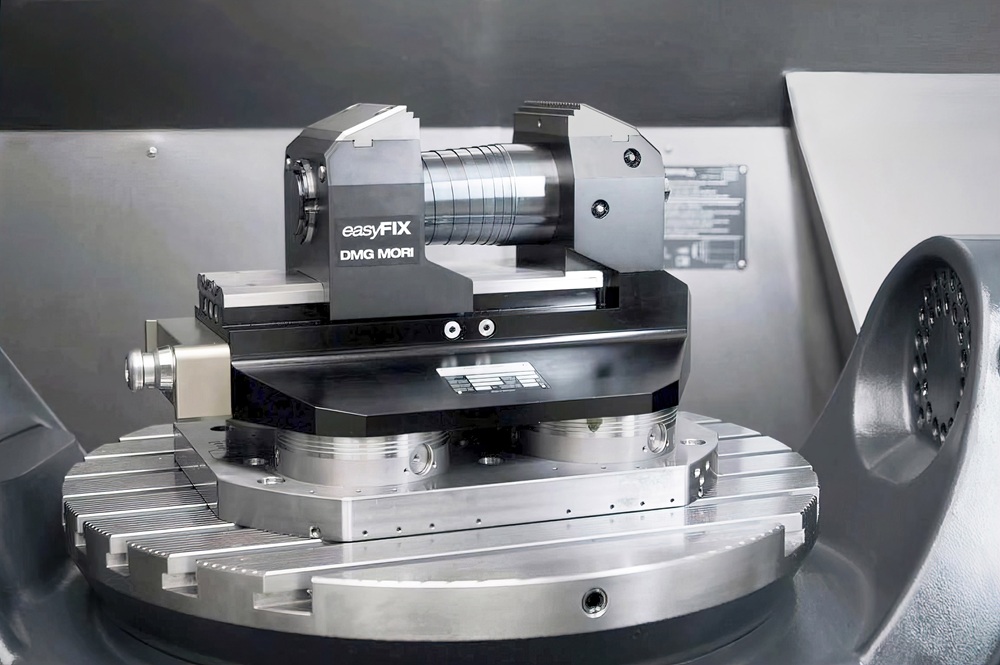
DMG Mori has introduced easyFIX, an automatically actuated vice designed for use with its Matris WPH pallet and workpiece handling system, Robo2Go and WH Cell automation solutions. The vice enables the movable jaw to be repositioned automatically for different workpiece sizes, reducing manual intervention when changing production batches. 

Available in two sizes, easyFIX mounts directly on the machining centre table when used with Robo2Go or WH Cell. The WPH version incorporates a Schunk interface for zero-point clamping and rapid fixture changeover. 

Although the movable jaw has a 4.5 mm clamping stroke, its position can be adjusted to accommodate larger changes in workpiece dimensions. A special device, automatically exchanged from the tool magazine into the spindle, moves the jaw along its linear axis to the programmed position. Alternatively, adjustment can be performed manually. 

A spindle-mounted probe first determines the vice’s position and then checks the new jaw location before the robot loads the first component. The machining centre control subsequently initiates pneumatic or hydraulic clamping. Once milling and drilling are complete, the robot removes the finished workpiece and loads the next. 

The easyFIX 100 uses pneumatic actuation to deliver 30 kN of clamping force. Standard jaws accommodate workpieces up to 110 x 150 x 190 mm, with optional jaws increasing the maximum length from 150 to 175 mm. 

The larger easyFIX 210 operates pneumatically at 10 bar or hydraulically at 80 bar, providing clamping forces of 45 kN and 50 kN respectively. It accommodates workpieces measuring up to 230 x 200 x 150 mm. 

For additional flexibility, configurations include a pyramid arrangement accommodating two vices and workpieces, and a dual-station version for larger components. All designs promote chip evacuation and simplify cleaning, supporting reliable automated production. 

More information www.dmgmori.com