Foundry installs £1.8m machining cell

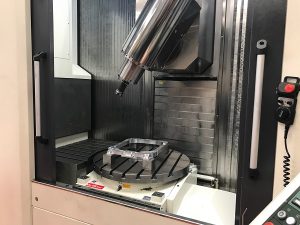
A £1.8m investment in a custom-built finish machining facility at the Walsall factory of Chamberlin & Hill Castings Ltd will see the installation of three high specification Chiron Scherer Feinbau automated mill-turn centres, helping the company become the UK’s only fully integrated supplier of grey iron bearing housings for engine turbochargers.
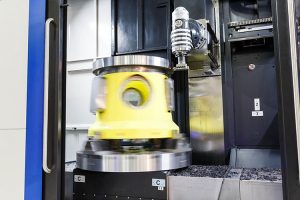
Supplied by the Engineering Technology Group (ETG), the modular machining centres offer a fully integrated machining solution combining a Scherer Feinbau twin-spindle VDZ100 vertical lathe operating in tandem (via a robot and conveyor system) with a Chiron DZ15W twin-spindle, twin-pallet milling centre.
A major, long-standing customer is Borg Warner, which had earlier advised Chamberlin & Hill that it was seeking an “integrated supply” in order to streamline the company’s supply chain.
“Without investing in machining capacity, the customer made it clear that it would have to review Chamberlin & Hill’s position as a supplier,” states chief executive Kevin Nolan. “In contrast, if we did make the investment, we were probably going to become the most significant supplier of turbo bearing housings in Europe.”
The Chiron cells were chosen for two reasons: firstly, Borg Warner already had around 60 Chiron machines producing similar parts, thus lowering the risk. Secondly, having cast the net far and wide, the company discovered that Chiron machines were one of very few which were both cost-effective and capable of producing the parts in the required cycle times.
Three Chiron machining cells were ordered, two of which were commissioned in February 2017, with a third scheduled to arrive in November this year. The capacity provided by these three machines has already been sold, bringing about additional revenue worth several million pounds per year.
For further information
www.engtechgroup.com

Cennox installs first machining centre

Banking and retail support services specialist, Camberley-based Cennox Plc,
is at the forefront in the battle against card skimming at cashpoints, developing components and systems that help banks stay one step ahead of the criminals. To maintain its lead, Cennox has an active R&D programme that requires numerous parts to be machined against relatively short lead-times. In addition, the company also has production parts to manufacture in order to back-up the service it provides to banks in repairing damaged cashpoints.
In the past, all of this machining work was outsourced, but as demand grew the cost and delays that this created was impacting on productivity, so the decision was taken to bring machining in-house. After investigating the market, Cennox chose Matchmaker CNC to supply the machine it required, as well as provide extra support in pulling together a tooling and CADCAM package (Sharp CAM). The selected machine was a Matchmaker VMC 1020 vertical machining centre with 1100 x
560 mm table that allows multiple set-ups to be in place at the
same time.

Typical savings against subcontracting these parts is running at around 75% per component. With initial batches running at 400-off, and ongoing at 20-30 off, this is a major saving.
“Considering that our starting point was of no machining experience whatsoever, we were probably a unique proposition for any machine tool company; we therefore had to place a lot of trust in Matchmaker,” says technical and operations support manager Iain Ferguson. “That trust was well placed as we now have a machining facility in which we are confident can produce anything that our design department comes up with.”
For further information
www.matchmakercnc.co.uk

Subcontractor takes off with five-axis VMC

When McGreevy Engineering made a strategic decision to move into the aerospace industry, the company realised it needed to take its first step into five-axis machining. The machine of choice was a Vcenter AX800 from Victor CNC.
Works manager Tommy Hanna says: “The reason we bought the AX800 was because it has a bigger capacity than most of its competitors, with 1.6 m in the X-axis. This capacity allows us to use it as a large-bed three-axis machine, as well as a versatile five-axis. The machine also has a 15,000 rpm spindle, which means we are conducting high-speed machining on a lot of our work. Providing jobs are set-up correctly, we can hit all five sides of the workpiece at high speed, which is making a huge saving for our business.”

The company has a variety of three-axis machining centres, but with the five-axis AX800 McGreevy needed more tool positions, as Hanna recalls: “Obviously, with five-axis we need more tool stations to hit the job from all directions, and the AX800 has 40 tool positions.”
The machine installed at McGreevy was specified with the through-coolant facility and swarf conveyor system, which supports large-capacity machining, as Hanna explains: “With 700 mm in the Y axis and 1600 mm in the X axis, plus the 800 mm rotary table, we can machine some particularly large parts. This is especially the case with the rotary table as we can machine one side of a long part and then rotate it to do the other side.”
For further information
www.victorcnc.com

HSM with OptiCool spindle technology

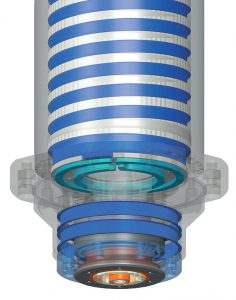
GF Machining Solutions’ Mikron MILL S600U five-axis machining centre for mould and die makers is now equipped with new HVC140 (StepTec) spindles. The StepTec Opticool spindle system, with its enhanced polar thermal balance, controls the temperature of the machine’s spindle and spindle bearings to improve part accuracies and surface finishes.

StepTec’s HVC140 spindles deliver high power and speed (13.5 kW/42,000 rpm), and feature proven OptiCool technology. Also contributing to the spindle’s performance is an all-new bearing design using ceramic hybrid bearings. As a result of their incorporation, radial and lateral stiffness are increased by 16% and 60% respectively. Furthermore, radial and axial run-out, as well as repeatability, of less than 2 µm
is achieved at the tool interface.
The machining centres, with their rigid base construction, combine high dynamic direct-drive technology with a range of design and build features and integrated ‘Smart’ software modules. These include: Ambient Robust, which monitors and regulates thermal variation detected in the machine’s base and drives; OSS (Operator Support System), which helps customers optimise their machining processes based on workpiece specifications/dimensions and their specific machining priorities – speed, accuracy and surface finish; and ITC/ITC 5AX (intelligent Thermal Control), which eliminates the need for, or reduces the time required for warm-up cycles.
For further information www.gfms.com

Industry 4.0 developments from Soraluce

That the Industry 4.0 integrated information initiative holds great benefit for machine tool users is patently clear to Soraluce – and will be to its worldwide customer base.

“The developments we are instigating now with machines and automated manufacturing systems are just scratching the surface of the possible rewards that users could harness from 30 years or more of advances in IT and computer technologies,” says Xabier Medizabal, R&D director at Soraluce, which is represented in the UK by TW Ward CNC Machinery (Ward CNC). “The correct use of these technologies holds the key to information gathering in automated machining scenarios that will enable users to not only boost production output but also help guarantee machining quality and consistency. These solutions are not expensive and they are available now. But the real challenge is being able to gather the information efficiently, then to trust and utilise that data and make objective decisions in order to gain real benefits.”
Reinforcing Mendizabal’s comments, Soraluce’s new ‘Smart Machine’ technology highlights how real-time machine status from smart sensors can be viewed and harnessed.
Based on cloud computing, the system captures and records all relevant information on overall machining cycle performance and energy consumption, as well as temperature, tooling usage/wear, energy consumption and downtime. It also, for example, produces alarms (including by email) of key process signs/preventative maintenance requirements. All data is accessible via PC and mobile devices as well as the internet.
For further information www.wardcnc.com