MANUFACTURERS URGED TO BE BOLD, NOT BOWLED OVER, BY ARTIFICIAL INTELLIGENCE 

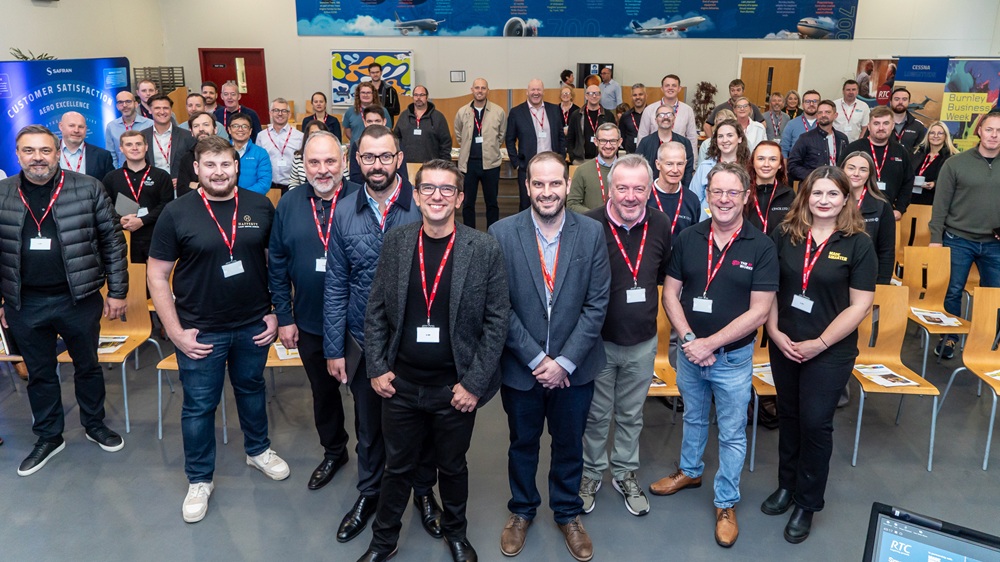
Manufacturers are being urged to harness the huge potential of AI without getting lost in the hype. The rallying call emerged from a major gathering of northwest manufacturers and technology experts hosted by Safran Nacelles in Burnley. An honest debate explored the opportunities, barriers and real-world impact of one of the fastest-moving technologies facing industry. 

The event, entitled ‘Smarter Manufacturing: Using AI to Improve Productivity and Performance’, was organised by RTC North, Made Smarter North West and Burnley Council, as part of Burnley Business Week and to mark the recent Make UK’s National Manufacturing Day. 

Almost 50 delegates attended the event, including manufacturers from sectors spanning aerospace, automotive and machinery to plastics and printing, with attendees travelling from across the northwest and as far afield as Yorkshire, London and the southwest. 

Business leaders shared how they are already using AI to save time, cut costs and improve productivity, but also spoke candidly about ‘AI fatigue’, a lack of time and specialist skills, concerns around data and security, and the challenge of keeping pace with the technology. 

The message was to be brave enough to experiment, but sceptical enough to question the results. Businesses were encouraged to start small, focus on genuine problems and keep human judgement firmly in the loop. 

Steve Wilkinson, of innovation and business support consultancy RTC North, said manufacturers should not be put off by the “noise” surrounding AI or feel under pressure to make a giant leap: “There’s a lot of dabbling and playing going on, and that’s a good thing. It’s part of technology adoption. What matters is finding justified, meaningful applications that help people in manufacturing make better decisions faster.” 

Ronan Hafferty, founder of Salford-based Hafferty Interiors, is already putting that approach into practice. With support from Made Smarter North West – the Government-backed programme helping SME manufacturers adopt digital technologies through expert advice, skills development, internships and grant funding – his company has deployed a digital intern to develop an AI strategy and explore applications from quality through to manufacturing. 

“AI has already made a real difference, particularly in design where it has saved us a huge amount of time and cost,” he said. “It’s blowing our minds every week with how quickly it’s developing. But you can’t be lazy with it. You can’t get rid of common sense and the human element.” 

That mix of excitement and healthy scepticism ran throughout the event. Judson Smythe, MD of Blackburn-based MGS Plastics, warned against ignoring AI’s potential or handing over too much control, urging fellow makers to “use AI as a tool, but don’t be the tool that AI is using”. 

Firms struggling to find the specialist skills or time to explore AI were also encouraged to look within their own organisations. Mike Riding, MD of Burnley-based Process Instruments, discovered an unexpected pool of knowledge and enthusiasm among his workforce after setting up an internal group to explore where AI could benefit the business. 

Safran Nacelles – which designs, builds and services jet engine housings known as nacelles for commercial, regional and business airplanes – offered a different perspective from a major manufacturer already well into its digital transformation journey. The 750-strong Burnley operation is exploring AI alongside technologies including manufacturing execution systems, connected machinery, simulation and automated inspection. 

Michelle Hubel, head of digital transformation, said the key for any business was to focus on the fundamentals of good data, the right skills, strong governance and security, and people able to question and verify what the technology produces. She said: “We all think we’ve got good data until we actually start looking at it.” 

A second panel featuring experts from Made Smarter North West, marketing agency Door4, IT and cyber security specialist Seriun and training consultancy The AI Works focused on how manufacturers can move from curiosity to practical applications. 

Mark Edwards of Seriun challenged the idea that AI needs to be sophisticated to make an impact, highlighting real-world examples of simple applications already delivering significant bottom-line gains for businesses. 

“Don’t worry about the stuff that AI can’t fix or can’t help,” he stated. “Use it to fix the things you can today to make your business quicker, faster, better.” 

Kevin Smith, lead technology adoption specialist for Made Smarter North West, urged manufacturers to start with the business problem rather than the technology: “AI doesn’t automate jobs, it automates tasks. Look at what takes up people’s time, what frustrates them and where AI could make a difference. 

“Then start small, get some quick wins and build confidence and skills,” he added. “Keep people at the heart of it and make sure you’re solving a genuine business problem. The opportunity is huge, but ultimately AI has to deliver value for your business.” 

The event concluded with a guided tour of Safran Nacelles’ Burnley manufacturing operations, giving delegates an opportunity to see its sheet-metal and nacelle production, and learn more about the aerospace manufacturer’s own digital transformation journey. 

More information www.madesmarter.uk
TTL INVESTS IN HECKERT X50 FROM STARRAG FOR HIGH-VALUE AERO-ENGINE WORK 

For a company that has built its reputation entirely on software, ordering a Starrag Heckert X50 five-axis machining centre might seem like a change of direction. For TTL, a Buckinghamshire specialist in adaptive machining and digital manufacturing, it is the logical next step for a business whose customers now trust it with projects where components can be worth six figures apiece. 

Founded in 1987 and based near Aylesbury, TTL has spent almost 40 years solving the problems between a CAD model and a finished part. It develops customised CAD/CAM/CNC solutions built around Siemens technology, specialising in adaptive machining, digital twins and in-process control for aerospace, defence, nuclear, medical and precision manufacturers worldwide. Around 85% of its customers are outside the UK. 

TTL has been owned by the Starrag/Tornos Group for more than 15 years, but operates as a standalone business unit with its own structure and IT systems. 

“TTL is an independent business unit which deals solely with software, and our solutions are all around Siemens NX and dealing with adaptive machining,” explains Simon Rogers, vice president at TTL. 

In December, the company will take delivery of a Starrag Heckert X50 five-axis horizontal mill/turn centre, the sixth machine at its Haddenham facility and the first TTL has bought from its parent group. 

Adds Rogers: “Jet engine components, repairing HPC blades, repairing blisks: that’s something we’re deeply embedded in, so we needed to invest in the best technology available. Our choice was a machine from the Starrag Group. It wasn’t purchased because we’re part of the Starrag Group. It was acquired on its technical attributes and the fact that a lot of our global customer base has invested in Starrag technology.” 

The driver is the changing value and complexity of the components that TTL’s customers are asking it to process. Automating the repair of a single blade is one business case; an integrated bladed rotor (IBR), or blisk, is another. 

“A complex integrated bladed rotor or blisk component, could be $50,000 to $150,000,” reveals Paul Whistance, finance director at TTL. “To automate the repair of those components with our technology and the Starrag Heckert X50 is a significant commercial advantage.” 

A major factor in the purchasing decision was a multi-machine adaptive machining requirement for a major US defence programme, on which TTL is working alongside Starrag as its process and software partner. The programme has made a significant long-term investment in the Heckert X50, so having the same machine at Haddenham allows TTL to develop, prove and optimise customer processes locally rather than at sites around the world. 

TTL’s five existing machines are small to medium-sized five-axis platforms, acquired from outside the group to suit lower value repair work. The business also runs a mixture of CNC control systems. As components have become more valuable and complex, however, that installed base has reached its limits. 

“We’ve historically opted for non-group machines because our customers required a lower-cost, entry-level multi-axis machine,” says Rogers. “A $500 part repair is a different business case from remanufacturing or manufacturing higher-value components. This is where our interest in Starrag machines has sparked.” 

The Heckert X50 is a horizontal machining centre with a trunnion table, providing short force paths, high structural rigidity and complete five-sided machining from a single set-up, alongside turning capability. For TTL, the trunnion arrangement is particularly important. 

“Have a trunnion gives us the ability to move components, which is huge for us in terms of dynamic capability,” he says. “The speed at which we can keep the tool tip in contact with a component, such as an aerofoil, is significantly improved. Additionally, the diameters we can reach are nearly twice those of other platforms on site.” 

The machine also provides considerably greater component height, opening up the mid-sized casings TTL previously could not accommodate, including the flanges and ports involved in casing remanufacture. 

“It has an 18,000 rpm motor spindle, five-axis milling and turning capability, the ability to mount an angle head, and the security of hybrid bearings. The machine also offers very high precision, incredible resonance control and unparalleled dynamics. That’s why we selected it.” 

TTL’s work typically falls into two areas. The first is new-part manufacture from castings and forgings, where the challenge is best-fit alignment in six degrees of freedom. The second is MRO (maintenance, repair & overhaul), where a component may no longer match the model from which it was originally manufactured. 

“Components in service are obviously not the shape they once were,” explains Rogers. “This is where we have to adjust for deviation or shape change caused by stress or heat deformation using an automatic measurement workflow that can scan and utilise probing data.” 

By measuring the component, TTL can automatically calculate a new CAD model, generate revised tool paths and post-processor code, simulate the process, and produce new G code. The ultimate objective is to eliminate manual finishing. 

“Very simply, you can machine so far and then you have to stop; otherwise you’re going to scrap the component. So you have to leave some stock, and that means high blends or high stock levels. Then you need a manual hand blending or die-grinding process, and that can lead to RSI [repetitive strain injury]. The health and safety challenges present a particular risk with Inconel or titanium polishing and grinding processes. 

“We have some customers that have applied the technology and no longer need hand finishing processes for their product to get back into service. This is a significant benefit.” 

The X50 is the smallest machine in the Heckert X series, which makes it a good fit for TTL’s development and turnkey operation rather than a conventional subcontract machining environment. 

“We have a geographical limit with our building, so we typically use small to medium-sized machines,” he says. “The X50 is a large machine for our facility, and it allows us to handle a medium-sized gas turbine component as it has a big swing with certain configurations. When it comes to a customer programme, we can align very quickly with an X70 or an X90 for the larger component types.” 

That scalability is important because processes proven on the X50 at Haddenham can be transferred to larger machines in the same family at customer sites. The machine will also provide a test bed for machining hard metals. 

“It’s a decision not made just by TTL; it’s a decision made by customers,” he states. “We like to follow what the end users choose. They’ve chosen Starrag for reasons based on cutting trials, assessments and specifications, and I agree with them in this case.” 

The order also reflects a broader shift in TTL’s relationship with its parent group.  

“Five years ago, 95%+ of our business was outside of the Starrag Group, now it’s 50%.” 

Adds Rogers: “We use our skills, our experience and our engineering knowledge to solve problems that others cannot solve. By having access to these machines locally, we can increase the capability both for us and the wider group, taking business to the next level.” 

More information www.starrag.com 

SUCCESSFUL TECHNOLOGY PARTNERSHIPS MEAN GOING THE EXTRA MILE

The outbreak of a devastating fire in April 2025 could have spelt curtains for Western Pegasus, a Birmingham-based precision engineering company specialising in high-accuracy and customised spline gauges, master gears and spline-related inspection gauging. 

Instead, through the leadership and dogged determination of company president Andy Wincel, the dedication of its 40-strong workforce, immediate financial support from its bank and strong business partnerships – most notably with United Machining – the company was back up and running within three months. 

United Machining, a manufacturer and supplier of EDM, milling, additive manufacturing and laser texturing machine tools – as well as automation, software and tooling systems – recently supplied Western Pegasus with three new AgieCharmilles wire EDM machines. 

The machines, a CUT 2000 and two CUT 1000 models, are now in situ at Western Pegasus’ new Kitts Green facility. The company relocated there following the major fire, which destroyed its original Tyseley plant of 40 years. 

The three machines, funded in part through an £850,000 overdraft facility followed by a £1.2m funding package from HSBC UK, have replaced AgieCharmilles EDM machines rendered unusable by the Easter Sunday fire. 

“Supporting Western Pegasus through such challenging times has been a highly rewarding experience,” says Steve Eames, relationship manager at HSBC UK. “We acted quickly to support the company’s recovery, and the resilience shown by the team was remarkable. It’s fantastic to see the business thriving.” 

Western Pegasus has built strong relationships with United Machining, previously GF Machining Solutions, over many years, with the company investing regularly in high-end wire EDM technology to increase capacity and capability. 

Says Wincel: “These machines are renowned for delivering consistent and repeatable high accuracies and superior surface finishes, making them our technology of choice.” 

The gauge and gear inspection equipment manufactured by Western Pegasus is specified globally by the automotive, aerospace, marine and agricultural industries. The equipment measures the dimensional accuracy and geometric tolerances of gear teeth, including tooth profiles, pitch deviations, thickness and size, lead and helix angles, and runout. 

Accuracy is non-negotiable, with gear tooth flanges and profiles requiring tolerances better than ±2 µm. This is why Western Pegasus has continued to invest in AgieCharmilles wire EDM technology. Featuring technologies including Intelligent Spark Protection (ISPS), iWire, the Uniqua iHMI interface and Automatic Wire Change (AWC), the machines combine high precision with fast processing speeds, flexibility and reliability. 

Armed with advanced machine tool technology, proven manufacturing processes and an experienced workforce, Western Pegasus was geared up for further growth. Then the fire started in an adjacent factory. 

“One of the most advanced wire EDM facilities in the UK was destroyed,” declares Wincel. 

The situation was made even more difficult by the fact that the fire broke out on Easter Sunday, disrupting communications, while Wincel was thousands of miles away at home in Australia. 

“You wouldn’t wish it on your worst enemy,” he says. “Dealing with loss adjusters, assessors and insurance claims is one thing, but when you add a workforce understandably wondering whether they still have jobs, as well as customers asking about the status of their work, the situation was fraught, to put it mildly. 

“We lost a lot. Our servers and IT equipment went up in smoke. Our machine tools and ancillary technologies were severely compromised. All our records, documentation and work in progress were gone too.” 

Despite the devastation, Wincel decided not to call it quits and instead began planning the rebirth of Western Pegasus. A warehouse facility he had previously acquired at Kitts Green, around 16 miles from the damaged Tyseley factory, was selected as the company’s new home. 

“We wanted to become operational as soon as possible,” he remarks. “However, it was important that we did things methodically and clinically.” 

The transformation was substantial. As well as assessing and removing what equipment could be salvaged from the old site, the Kitts Green premises required complete modernisation. The work included cleaning and clearing the building, upgrading electrics and plumbing, installing new floors and a roof, creating offices and toilets, designing a temperature-controlled machine shop and constructing an accredited inspection laboratory. It was a monumental undertaking, made even more challenging by the tight timescale. 

“I contacted United Machining UK’s managing director, Martin Spencer, to see if he could assist us in acquiring a number of advanced wire EDM machines in double-quick time.” 

Western Pegasus had previously acquired 10 AgieCharmilles wire EDM machines and two System 3R automation systems from United Machining. The fire had left the equipment unfit for purpose. 

“United Machining was our first port of call and fortunately the company mobilised its resources to help us out.” 

Adds Spencer: “First and foremost, we wanted to help. Western Pegasus is a loyal customer and we believed that Andy and his team, with the right support, could turn it around and make a success of things. 

“Having spoken to Andy about his immediate requirements, we identified the type and number of new AgieCharmilles wire EDM machines needed to restart machining operations: a CUT 2000 and two CUT 1000 models.” 

However, there was a problem. Machines such as the CUT 1000 and CUT 2000 are built to order rather than held in stock. The urgency of Western Pegasus’ situation therefore triggered an international response, with AgieCharmilles’ manufacturing facility in Zandone, Switzerland, marshalling its resources to build the three replacement machines in record time. 

“It was a real collaborative effort,” says Spencer. “It demonstrated how United Machining is able and willing to pull out all the stops for its customers.” 

Starting in June, the three wire EDM machines were delivered and installed individually at Western Pegasus’ new facility over a period of just six weeks. This rapid response enabled production to resume while the wider relocation and building programme continued. 

“When you’re up against it, you really find out who your partners are,” says Wincel. “United Machining pulled out all the stops for us. They helped us clear the old site, arrange safe storage of equipment, identify where and how we could acquire three new machines, and organise delivery and installation around our building schedule. 

“They also provided expert applications and logistics advice and support, enabling us to hit the ground running. The fire completely took out our manufacturing operations, but in just 10 weeks we were back in business. We simply could not have achieved this without United Machining and its suppliers. That’s what a real partnership is all about.” 

More information www.gfms.com/uk 

WES GAINS COMPLETE CONFIDENCE IN COMPLEX MACHINING WITH VERICUT

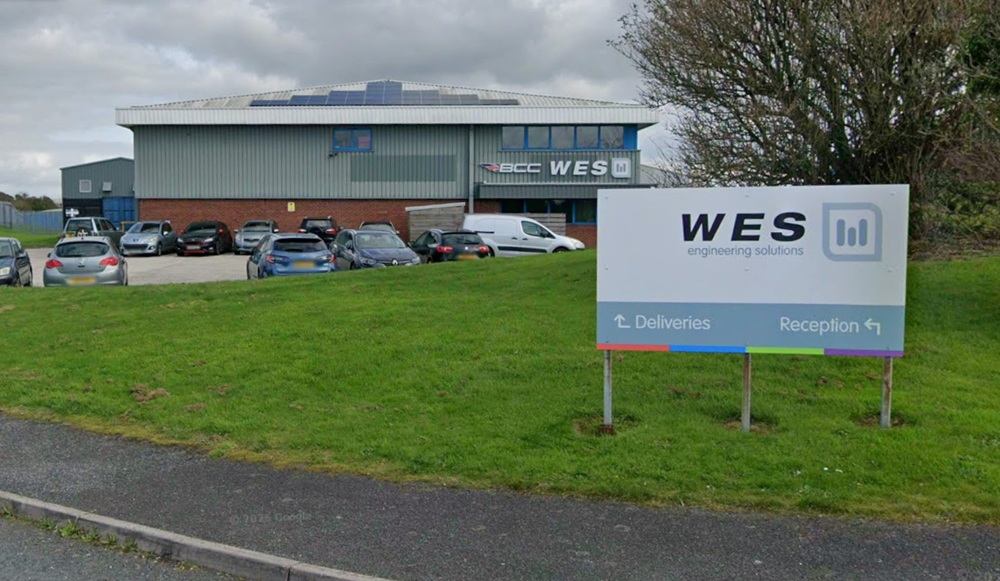
For precision subcontract machinist WES Engineering Solutions, confidence is fundamental to every machining operation. Manufacturing complex components for demanding industries that include aerospace, defence, nuclear and oil & gas demands absolute faith in every CNC program before the first chip is cut. By integrating Vericut simulation, verification and analysis software into its programming workflow, the Redruth-based company is verifying all four- and five-axis CNC programs before they reach the machine, safeguarding expensive equipment while enabling productive unattended machining.

WES Engineering Solutions employs around 40 people across three specialist divisions. Alongside its subcontract machining business, the company operates a hard metal engineering division specialising in grinding and EDM, together with British Classic Car Performance Braking, which manufactures high-performance brake calipers for classic vehicles. Everything from Austin, Daimler, Ford, Hillman and Jaguar, to Jensen, Land Rover, MG, Morgan, Sunbeam and Triumph.

Across its business divisions, WES machines materials that extend from plastics and copper to stainless steel, titanium and Inconel, machining complex, high-precision components to tolerances as tight as 10 μm, even lower in the case of hard-metal parts undergoing grinding or EDM.

Supporting these demands is an ongoing investment programme in advanced manufacturing technology. Since 2022, WES has boosted its subcontract offer by installing a trio of palletised Matsuura CNC machining centres. An H.Plus-300 four-axis horizontal model with 15 pallets was the first to arrive, followed by two five-axis vertical models, namely an MX-520 with four pallets in 2024 and an MX-330 with 10 pallets in 2026. The extensive pallet capacity provided by these high-performance machines allows the company to maximise lights-out production while increasing flexibility and throughput.

“We found the first Matsuura machine held tolerances exceptionally well, so when we needed additional five-axis capacity it made sense to invest in Matsuura again,” explains James Humphrey, Production Engineer at WES Engineering Solutions. “The latest MX-330 further increases our unattended machining capability, which is becoming increasingly important as customer demand continues to grow.”

Alongside investment in machine tools came investment in Vericut simulation, verification and analysis software. WES currently has one Vericut licence, supporting its Matsuura machining centres. Using Autodesk Fusion 360 CAM software, programmers generate the machining strategy before transferring the job directly into Vericut via its integrated Fusion interface.

“When a new job arrives, we decide on the tooling, fixturing and most appropriate machine before creating the tool paths in Fusion,” explains Humphrey. “Moving the project into Vericut is incredibly straightforward – just a couple of clicks.”

Using Vericut’s Verification, Multi-Axis and Machine Simulation modules, WES simulates every machining process against digital models of its Matsuura machining centres, checking for collisions, over-travel and other potential issues before releasing programs to production. Vericut’s Auto-Diff module provides an additional layer of confidence by comparing the machined component with the original CAD model, highlighting any remaining stock or potential gouges.

“Vericut gives us complete confidence that the machine isn’t going to do something different to what we’ve programmed,” states Humphrey. “We’ve had occasions where the job looked fine in the CAM graphics, but Vericut highlighted something different. It prompted me to go back into Fusion, make a few changes, repost the code and check it again before sending it to the machine.”

For WES Engineering Solutions, independent verification is invaluable. The company regularly manufactures high-value components using equally expensive cutters and machines. Even a minor programming error can result in broken tooling, scrapped workpieces or even machine damage.

“We’ve all heard the stories of programming mistakes causing expensive collisions,” he notes. “Repairing or replacing a spindle on a five-axis machining centre wouldn’t be cheap. Every programmer, however experienced, worries about making that one tiny mistake. Vericut goes a long way towards mitigating that concern.”

The software also transforms and expedites the proving-out process on the shop floor. Rather than operators cautiously monitoring every program with a finger poised over the feed-hold button, they can approach new jobs with considerably more confidence.

“It saves time. What’s more, operators can confidently get on with other work instead of standing there waiting to see whether something goes wrong.”

This confidence becomes even more valuable when programming changes are made late in the working day before machines continue running unattended overnight.

“Confidence is everything,” reasserts Humphrey. “With Vericut, if I make a programming change at the end of the shift, I know I can ask the team to run it overnight without worrying about collisions.”

Before selecting Vericut, WES evaluated several alternatives. Alongside the software’s proven capability, access to UK-based technical support proved an important consideration. Following a trial period that included deliberately introducing programming errors, the decision quickly became clear.

“We wanted reassurance that the software would correctly identify problems before they reach the machine,” he remarks. “During the trial, Vericut detected everything we expected it to. Since then, the ongoing support has been very responsive whenever we’ve needed assistance.”

Although the financial return is difficult to quantify precisely, Humphrey believes the investment continues to deliver value every day by preventing problems before they occur: “The nature of Vericut means you never really know what it’s saved because the incidents simply don’t happen. It could be a broken cutter, a scrapped component or avoiding serious machine damage. In my opinion, more important is the complete peace of mind it provides, allowing us to concentrate on producing high-quality parts and meeting the delivery expectations of customers.”

Quality is everything at WES, which is why software like Vericut is so important to its operations. The company is committed to continuous improvement, investment in systems and automation, long-term capability development, and supporting customers in regulated and safety-critical industries.

WES Engineering Solutions carries accreditations for ISO9001 and the AS9100 quality management system standard for the aerospace industry. In addition, the company holds Fit For Nuclear (F4N), a nationally recognised programme that assesses a company’s capability to operate within the UK nuclear supply chain, and JOSCAR registration, the collaborative accreditation system used by major aerospace, defence and security organisations. WES also complies with Cyber Essentials Plus, a government-backed certification that verifies the effectiveness of cybersecurity controls through independent technical testing.

As WES Engineering Solutions continues expanding into increasingly complex, higher-value manufacturing sectors, confidence remains central to its future growth. With its investment in advanced machine tools and automated production, Vericut provides the assurance that every program has been thoroughly simulated and verified before manufacturing begins. The result? Safe, efficient and reliable machining for the benefit of both WES and its customers.

More information www.vericut.com/en-gb

TALKING DATA: HOW MITSUBISHI ELECTRIC AUTOMOTIVE CZECH TRANSITIONED TO DATA-DRIVE DECISION MAKING

In modern production environments, competitive advantage is increasingly determined by how effectively a manufacturer can capture, connect and act on data. At Mitsubishi Electric Automotive Czech (MEAC), located in Slaný, data has become a strategic asset.

The facility, which supplies electrical automotive components including integrated starter generators to manufacturers across Europe, first opened in 2001. It now employs over 500 people and has evolved from a traditional production environment into a highly connected factory where millions of data points are transformed into real-time operational insight, as it looks to support the automotive industry’s transition towards electrification and smart manufacturing.

Crucially, rather than pursuing digitalisation through wholesale equipment replacement, MEAC has adopted a pragmatic approach that combines proven production assets with connected automation technologies, facilitated by its long-term automation equipment supplier, Mitsubishi Electric Factory Automation. The result is a factory that has made significant improvements to its output, quality, uptime, environmental impact and employee wellbeing.

One of the most striking aspects of MEAC’s digital transformation is its approach to existing infrastructure. While many manufacturers would have pursued a strategy of replacing existing machinery and control systems, for MEAC, the focus has been on extracting greater value from equipment that continues to perform.

“On the production side, we keep what works,” explains Jan Kabát, manufacturing engineering manager. “Our Q-Series control units have been operating reliably for more than 10 years, while modernisation is achieved through a data layer using MES interfaces to connect machines and generate operational insights without disrupting output.”

He continues: “We do not modernise machines simply for the sake of it. The stable Q-Series control remains in place, while connectivity and data capabilities are added where they deliver measurable gains: less downtime, better visibility and faster troubleshooting.”

Such an approach has enabled MEAC to connect more than 100 machines through Mitsubishi Electric’s e-F@ctory architecture. This has created a digital layer that provides visibility into plant performance without incurring significant CapEx costs.

The data generated now forms the basis of day-to-day decision making throughout the factory. It enables engineers to create custom reports and deploy additional sensors where greater process visibility is required.

However, for MEAC, the real value of connectivity lies in the ability to continuously improve manufacturing performance. Digital tools and analytics provide detailed visibility into processes, allowing teams to quickly identify issues and implement corrective actions before they affect production quality or customer deliveries.

For Dalimil Bartoň, general manager, data has become central to the company’s continuous improvement strategy: “We use data to drive continuous improvement in both process and product quality. By analysing detailed manufacturing data, we can identify defect patterns, optimize processes and reduce scrap. The result is more consistent quality for customers and lower manufacturing costs for the business.

“The point isn’t about using technology for technology’s sake. It’s knowing how to deploy systems so they genuinely support production within a true PDCA cycle. By using Mitsubishi Electric FA’s portfolio in a pragmatic way, the team continues to raise automation levels, protect quality, and deliver measurable results on the shop floor.”

While digital transformation is often associated with plant equipment, MEAC has also applied data-driven techniques to improve working conditions for employees. The company uses RFID technology and workstation data to understand how work is performed across the facility and identify opportunities to reduce physical strain.

Petr Soukup, manufacturing senior manager, explains: “We use RFID technology to identify operators and understand where they are working, combining this information with muscle-load and workstation-level data. This helps us plan job rotations and organize work more effectively to reduce ergonomic strain. As a result, we’ve achieved more consistent performance across shifts.”

With MEAC also understanding the impact of environmental conditions on production performance, the facility represents a comprehensive software-defined building based on Mitsubishi Electric iQ‑R PLCs and ICONICS GENESIS64 software.

According to Milan Koňarik, facility manager, the system provides a single view of critical facility infrastructure. “Our software-defined building is built on ICONICS and GENESIS64, with Mitsubishi Electric iQ-R PLCs. This allows us to actively manage the plant environment and its impact on production.”

He adds: “We monitor HVAC, the data centre, pre-cooling systems, UPS and other technical utilities, with over 3000 measurement points feeding a single data view for faster decision-making. The system can trigger SMS and email alarms, support smarter energy purchasing and help our energy-saving team act quickly. We see it as a practical tool for reducing energy costs and operational risk while keeping our carbon neutrality ambitions on track.”

Ultimately, as automotive manufacturers continue to face pressure to improve efficiency, quality and sustainability, MEAC shows how effective digital transformation can be achieved without disrupting established production processes.

With improved visibility of key data points, reduced downtime, enhanced product quality, lower energy consumption and a more sustainable working environment, MEAC has truly managed to get its data talking.

More information https://emea-fa.mitsubishielectric.com/fa/