TaeguTec Grows TS-Thread Solid-Carbide Thread Mill Range

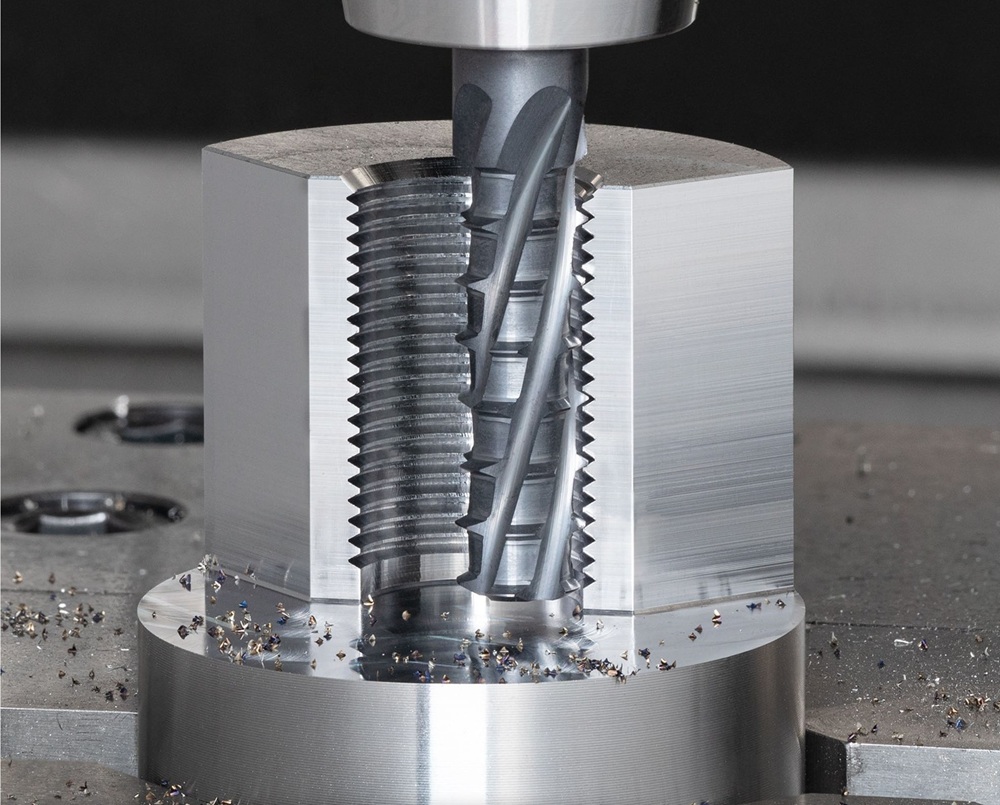
TaeguTec has expanded its TS-Thread solid-carbide thread milling range with four new tools: MTECBF, MTECH, MTECM and MTECK. Each addresses specific requirements in everyday and specialist threading applications. 

The TS-Thread series uses circular interpolation to produce threads in a single helical pass. A single tool can produce multiple thread sizes, while controlled entry conditions reduce radial cutting forces and the risk of tool breakage in difficult materials. 

The MTECBF features seven or eight flutes, depending on diameter, and is available from 12 to 24 TPI. Its geometry is optimised for blind-hole threading, while the high flute count enables higher feed rates. Combined with through-tool coolant, this capability supports efficient chip evacuation and reduced cycle times in high-volume production. 

For hardened steels and other difficult-to-cut materials, the MTECH combines threading and 45° chamfering in a single operation. Manufactured from solid carbide in TT5515 grade, it eliminates a separate chamfering process while maintaining accuracy and repeatability. It is available in ISO and UN standards, including M5, M6, M8 and M12, and UNC #6 to ½ inch. 

The MTECM and MTECK use multi-lead geometries for deep-hole threading. Notably, the MTECM has a triple-lead design, providing three times the thread pitch per revolution, while the MTECK uses a double-lead design. Both reduce cutting load per tooth and incorporate central coolant for chip evacuation and high-feed cutting. Both are available in ISO and UN standards. 

All four tools are available from stock, priced within the GAL system and manufactured to TaeguTec’s TS-Thread quality standards. Cutting data covers ISO material groups including steels, stainless steels, high-temperature alloys and non-ferrous materials. 

More information www.taegutec.com
Interchangeable-head PCD Mill Reduces Machining Costs

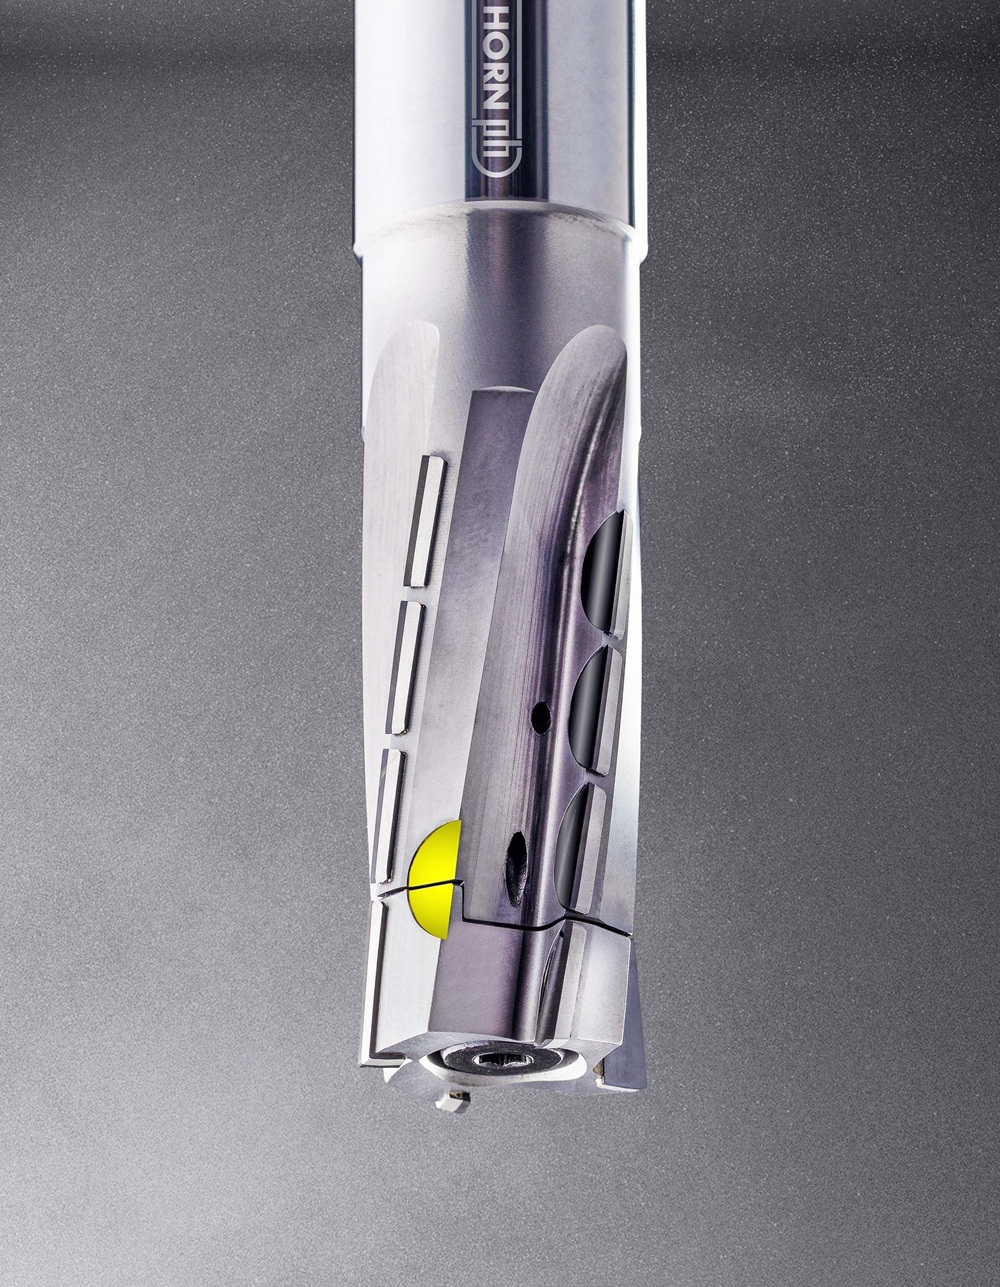
Cutting tool manufacturer Horn has introduced a modular range of PCD (polycrystalline diamond) end mills for machining aluminium, plastics and other materials in groups N (non-ferrous) and O (non-metallic). The system combines a reusable, solid-carbide shank and a PCD-tipped, interchangeable steel head. Availability in the UK and Ireland is through Horn Cutting Tools. 
 
Horn has designed the DM40 system to conserve resources and ensure cost-effective machining. The end cutting edges of the mill are among the main wear zones, while peripheral cutting edges longer than twice the tool diameter are susceptible to high lateral cutting forces, vibration and chipping. Notably, the ability to change just the head reduces follow-on costs compared with conventional monobloc tools, especially as the worn, brazed-on, PCD tips can be resharpened up to twice. 
 
By designing the cutter with a separate shank and head, Horn has ensured that the consumable cost is not only lower but also more predictable, making the tool system suitable for series production runs and automated lines. Users can quickly replace the head module on-site, so the tool is rapidly back into service, maximising spindle uptime. 
 
The head is attached to the shank via a central clamping screw that provides both a force-fit and a form-fit connection. Colour coding facilitates the identification of components, while a poka-yoke principle prevents assembly errors. The rigidity of the interface ensures precise machining, whether using a new or a resharpened tool, and the large axial rake angle enables smooth cutting and produces a smooth surface finish. 

More information www.horn-group.com 

Walter Launches Two New Tiger·tec Gold Turning Grades

Whether for offshore applications, oil and gas production, food manufacturing or the defence, chemical or energy sectors, the new Tiger·tec Gold MT-TiCN-CVD turning grades WMP20G and WMP30G can make a difference. With this product line, Walter is responding to growing global demand for stainless steel components. 

The WMP20G universal grade is now Walter’s first choice for traditional applications involving ISO M materials. Thanks to its hardness, it is suited to high cutting speeds and mass production. The grade is designed to deliver maximum productivity and long tool life when machining austenitic, ferritic, martensitic and duplex materials up to ISO P.  

Walter’s tougher WMP30G grade is a problem-solver, particularly for large and expensive components and in single-part manufacture, where maximum reliability is paramount. The company cites turning weld seams in armour plating as a typical example that demonstrates its durability. 

The most significant special feature is the new gradient substrate. Thanks to localised cobalt insertions, it is particularly tough at the cutting edge yet hard at the core. Such a design protects the cutting edge from chip impact and helps minimise fractures. A double post-treatment of the cutting edge further reduces friction.  

This completely new type of indexable insert design is rounded off by a Tiger·tec Gold coating specially adapted for ISO M machining, as well as the stable RM7 roughing geometry.  

The coating is particularly suitable for machining forged parts or for standard geometries that are prone to fracture when turning against a shoulder. Together, they form a solution package that Walter says is unique on the market to date, offering high levels of reliability and wear resistance, and suitability for the entire range of stainless steels. 

More information www.walter-tools.com 

MAPAL Unveils Technological Breakthrough in Fine Boring

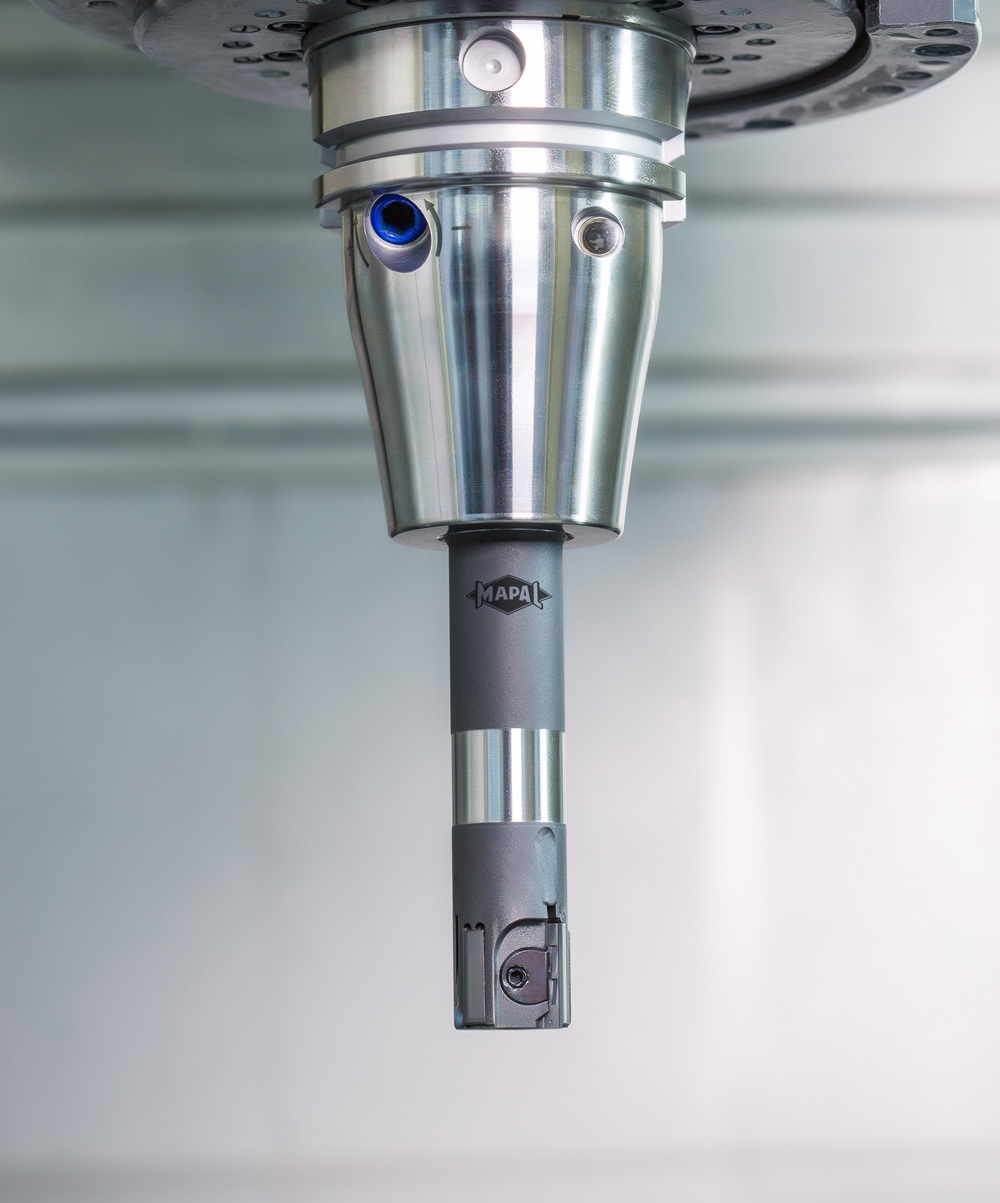
According to MAPAL, the company’s new EA-Performance-System sets a new benchmark in fine boring, bringing one-screw setting to the demanding 10 to 19 mm diameter range for the first time. The system reduces setting effort while maintaining high precision, surface quality and process reliability. 

Conventional fine-boring tools use two adjustment elements to set diameter and cutting-edge taper, making the process sensitive and dependent on operator expertise. MAPAL’s EasyAdjust-System, previously available from 20 mm diameter, simplifies this process with a single adjustment screw for diameter and a back taper permanently integrated into the cartridge system. 

MAPAL has now transferred this principle to the 10 to 19 mm range, using a new design configuration suitable for a broad spectrum of materials. The stable insert fixation required at these small diameters places high demands on system design, manufacturing precision and stability. MAPAL has addressed this by adapting the connection between the indexable insert and clamping system. 

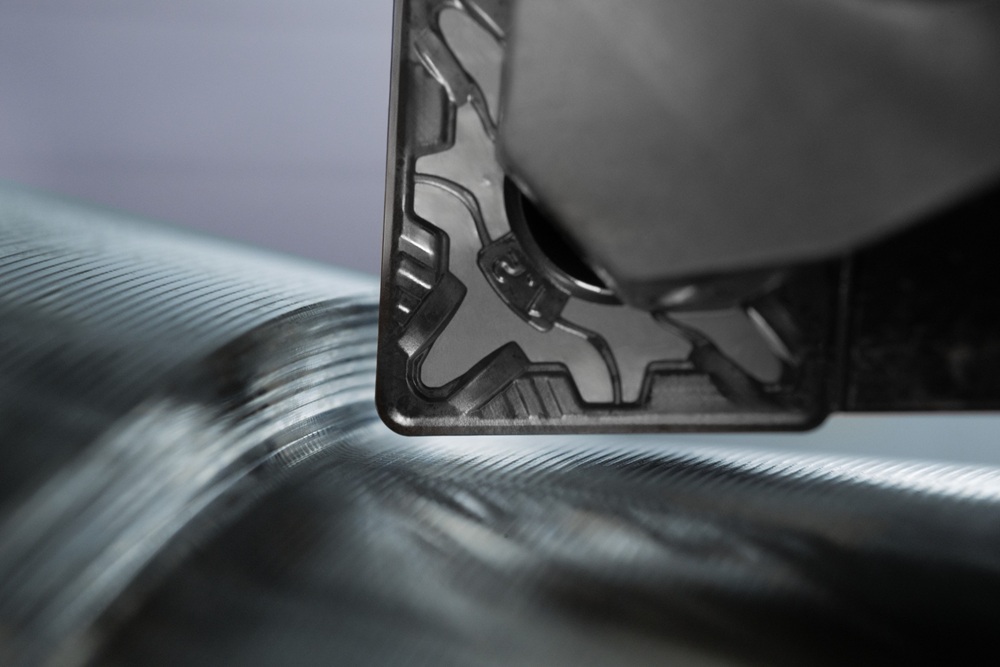
At the heart of the EA-Performance-System is a newly developed indexable insert with defined contact geometry. Combined with a matching clamping jaw, this provides positive-locking, reproducible insert positioning. The clamping mechanism transfers the setting movement precisely while maintaining secure fixation under process load. 

The system enables micrometre-precise setting with simplified handling, helping to minimise correction effort and reject rates while supporting stable machining processes. This capability makes it suitable for applications including high-precision fit and bearing bores in transmission housings, cylinders, crankshafts and camshafts. 

MAPAL’s EA-Performance-System is already in use at selected customers, with ongoing production confirming stable setting behaviour and reproducible machining results. 

More information www.mapal.com

Introducing the CoroMill MR20 for Controlled Profile Milling

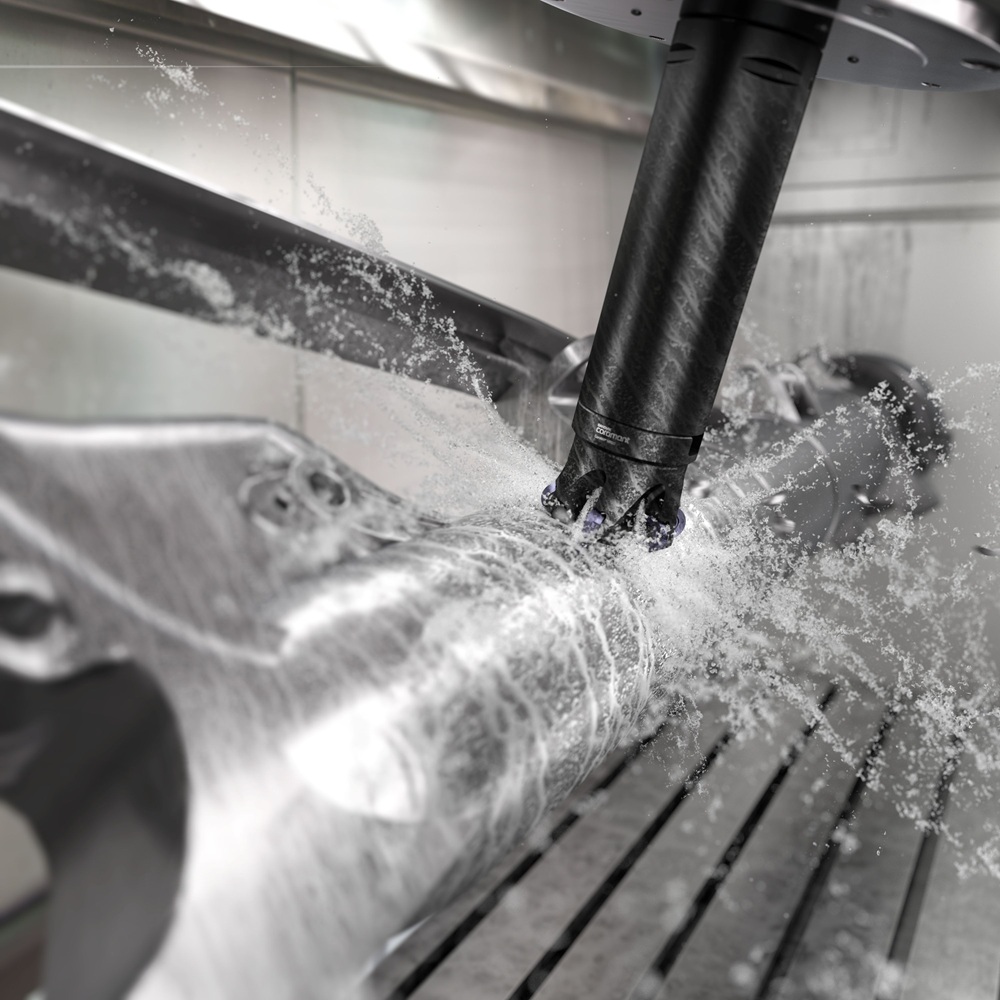
Sandvik Coromant says its new indexable milling concept combines stability, predictable performance and high metal removal rates across demanding materials and applications. CoroMill MR20 is a single-sided round-insert milling concept developed for secure, high-performance profiling and face milling. Optimised for ISO M, ISO S and ISO P materials, it is suited to pocketing and complex profiling in titanium and other HRSA materials. 

CoroMill MR20 also provides reliable roughing and semi-finishing in ISO P die and mould applications, while its high metal removal capability makes it suitable for pump and valve components in ISO M materials. 

“Our goal while developing CoroMill MR20 was to create a polyvalent cutter that offers the highest level of process security,” reveals Alvaro Ruiz, global product application specialist at Sandvik Coromant. “Customers machining high-value components need predictable, repeatable performance, and CoroMill MR20 delivers exactly that.” 

The cutter features an optimised insert seat with a large contact area between the insert and cutter body, minimising micro-movement for greater stability. An advanced cutter body design provides resistance to fatigue and deformation, while an integrated under-coolant system supports performance in long-chipping and difficult-to-machine materials. 

The six-edged insert has a thick, robust body for high bulk strength and edge-line security. Tight manufacturing tolerances promote gradual, predictable wear, supporting unmanned production, reduced scrap and high uptime. 

CoroMill MR20 can also contribute to more sustainable machining. Higher feed-per-tooth capability can reduce machining energy requirements, while long tool life means fewer inserts are consumed, reducing waste and associated carbon emissions. 

“Increasing feed capability while extending tool life means fewer resources used and less waste generated,” adds Ruiz. “It’s a win for productivity and for sustainability.” 

More information www.sandvik.coromant.com