Guhring UK Responds to the Industry’s Carbide Crisis

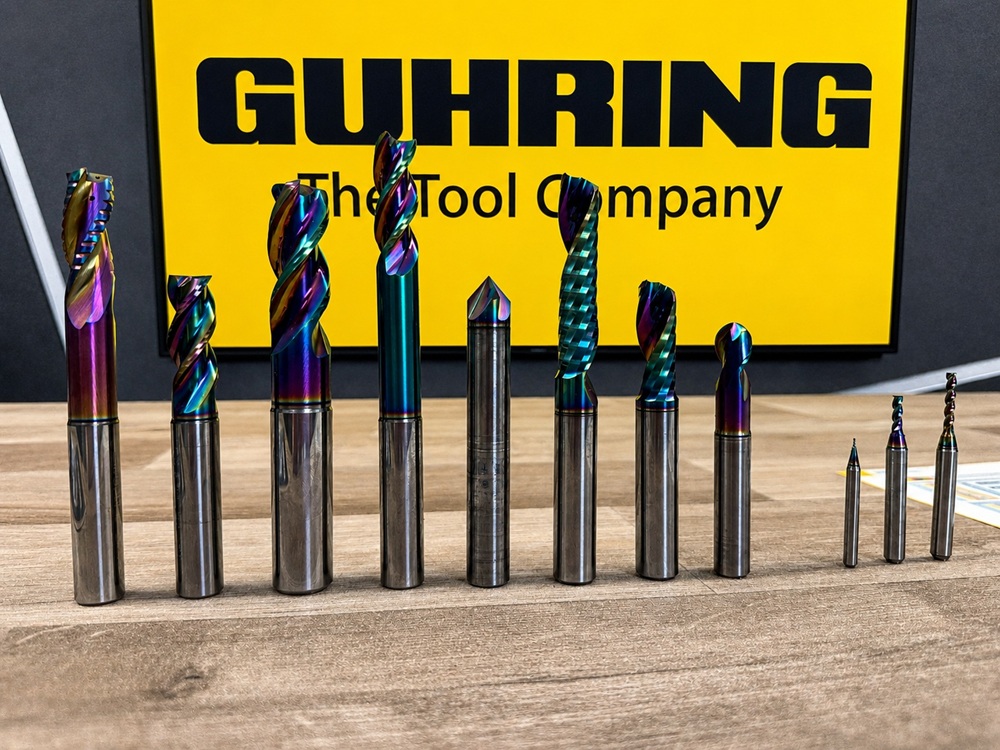
With carbide prices climbing and uncertainty over where they will settle, tooling specialist Guhring is urging manufacturers to take a closer look at regrinding. Guhring UK’s national sales manager Chris Bush explains how the company restores worn tools to new-tool performance at its UK facility. 

“It’s something people need to focus on a bit more given the current carbide crisis. We do it all in our UK facility, including in-house coating and de-coating. We regrind tools on the same machines used to manufacture new tools.” 

Guhring’s Birmingham facility houses 20 CNC cutter grinders and can regrind both Guhring and third-party tools, from gun drills, twist drills and thread mills to end mills and PCD tools. Small mixed batches are also accommodated, with a minimum order of three identical tools to justify machine set-up. 

The service includes stripping the original coating before regrinding and applying an application-specific replacement from a choice of 10 coatings. 

“Depending on what was on the new tool, we mirror that on the regrind. Crucially, the team strips the old coating before regrinding rather than simply layering over it. An excess build-up of layers becomes unstable and gives a difference in performance that will prevent the tool from performing ‘as-new’.” 

Re-ground tools undergo the same manufacturing and inspection processes as new tools, maintaining quality, performance and repeatability. The financial benefit is particularly significant at a time of rising carbide prices.  

“Once you’ve bought the new tool and paid for the carbide, the regrinding cost is independent of whether the carbide cost goes up or down,” says Chris. “So you can extend your tool lifecycle and use it two, three or more times.” 

More information www.guhring.co.uk 
Tooling Solutions for Modern Manufacturing at AMB 2026 

At the recent AMB 2026 exhibition in Stuttgart, Kyocera Unimerco presented tooling solutions designed to help manufacturers address production challenges including increasing productivity demands, rising costs and the need for greater process transparency. Its presence focused on applications for the automotive, fluid technology and general engineering sectors, combining machining expertise with intelligent tool management and advanced coating technologies. 

A key focus was the transformation of automotive production. As OEMs increasingly adopted large structural castings and expanded high-volume manufacturing, requirements for productivity, precision and cost control continued to grow. Kyocera Unimerco demonstrated tooling concepts developed to support these evolving requirements and improve machining performance in demanding production environments. 

For the fluid industry, Kyocera presented its drill reamer, a combination tool that performs drilling and reaming in a single operation. The solution is designed to produce H7 tolerance holes in selected steel and cast iron grades under defined machining conditions. By replacing dedicated drilling and reaming tools, it can reduce tooling complexity, shorten cycle times and improve process security. 

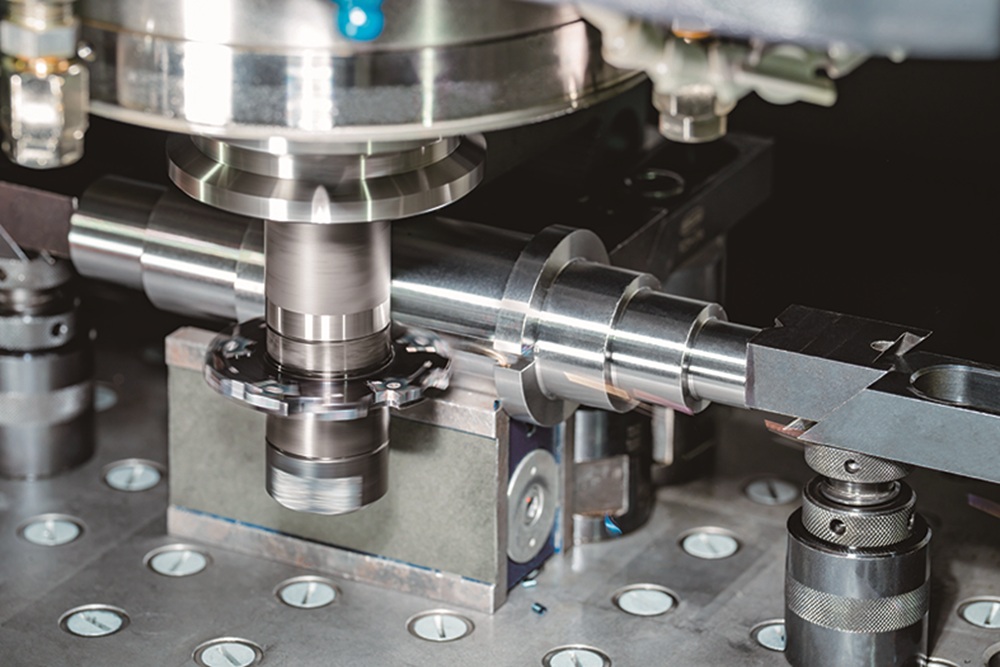
Other tooling on display included the KGX grooving and cut-off tool, featuring an advanced clamping design and common insert platform for external, internal and face grooving; the ME90 helical end mill for titanium and other difficult-to-machine materials, using double-sided eight-edge inserts and the PM335S grade; and the MG90B slot milling cutter (pictured), which combines rigid insert clamping, reduced cutting forces and six-edge inserts for efficient material removal. 

Kyocera Unimerco also showcased high-performance cermet inserts, the MFH Micro high-feed milling cutter and DRA MagicDrill indexable drills as alternatives to dedicated solid-carbide solutions. 

Alongside cutting tools, the company demonstrated its CC945 intelligent tool management solution, providing greater visibility of tooling operations, inventory and availability. 

More information www.kyocera-unimerco.com 

One Drill Body, Many Applications with X Tip Drill 

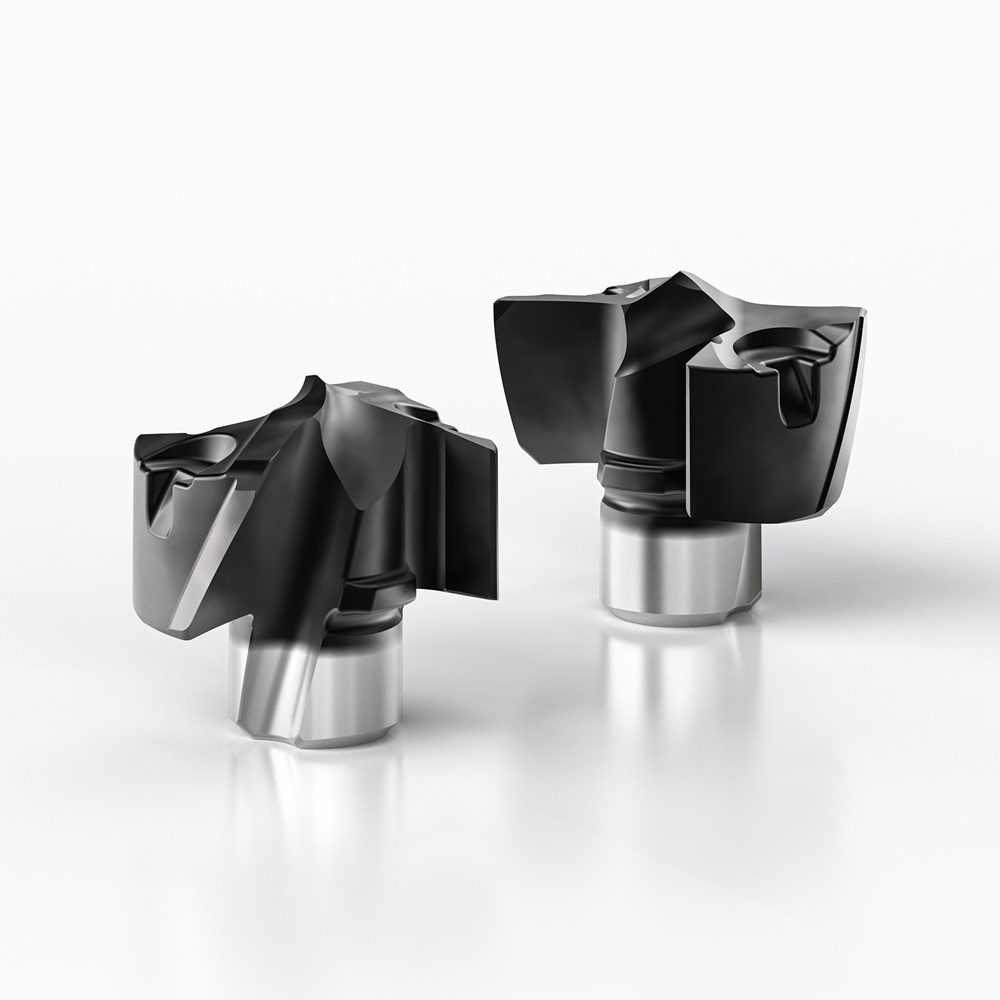
The Seco® X Tip Drill simplifies hole-making with one modular drill body and multiple, exchangeable carbide tips that perform across steel, stainless steel, cast iron and more. The result? Reduced tool inventory, higher productivity and consistent, high-quality results. 
  

Designed for mixed production environments, the Seco X Tip Drill adapts easily to changing materials and drilling depths. With one drill body covering 3xD, 5xD and 8xD applications, manufacturers can streamline workflows, lower the risk of errors and reduce set-up time without compromising performance, reports Seco. 
 
A patented pre-tensioned interface enables fast tip changes. A double-sided key supplied with each drill body allows quick, secure tip replacement, while the axial lock ensures accuracy and repeatability even after multiple changes. 
 
Application-specific geometries facilitate predictable performance across demanding materials. ISO P and M tips provide reliable drilling in steels and stainless steels; ISO K geometry delivers stable cutting in abrasive cast iron; and the Flat-Bottom geometry produces flat-bottom holes in a single operation, eliminating secondary machining steps. All geometries are compatible with the same X Tip drill body. 
 
“The Seco X Tip Drill gives manufacturers a smarter way to manage complexity,” says Ricky Payling, global product manager for solid round tools (drilling) at Seco. “One drill body, multiple applications, less waste and consistent performance. It’s designed for flexibility on today’s shop floor.” 
 
High-feed capability, optimised chip evacuation and self-centring geometry deliver fast cycle times, excellent hole quality and low cost per hole. The reusable drill body and replaceable, recyclable carbide tips also support more sustainable manufacturing. 

More information www.secotools.com 

TaeguTec Grows TS-Thread Solid-Carbide Thread Mill Range

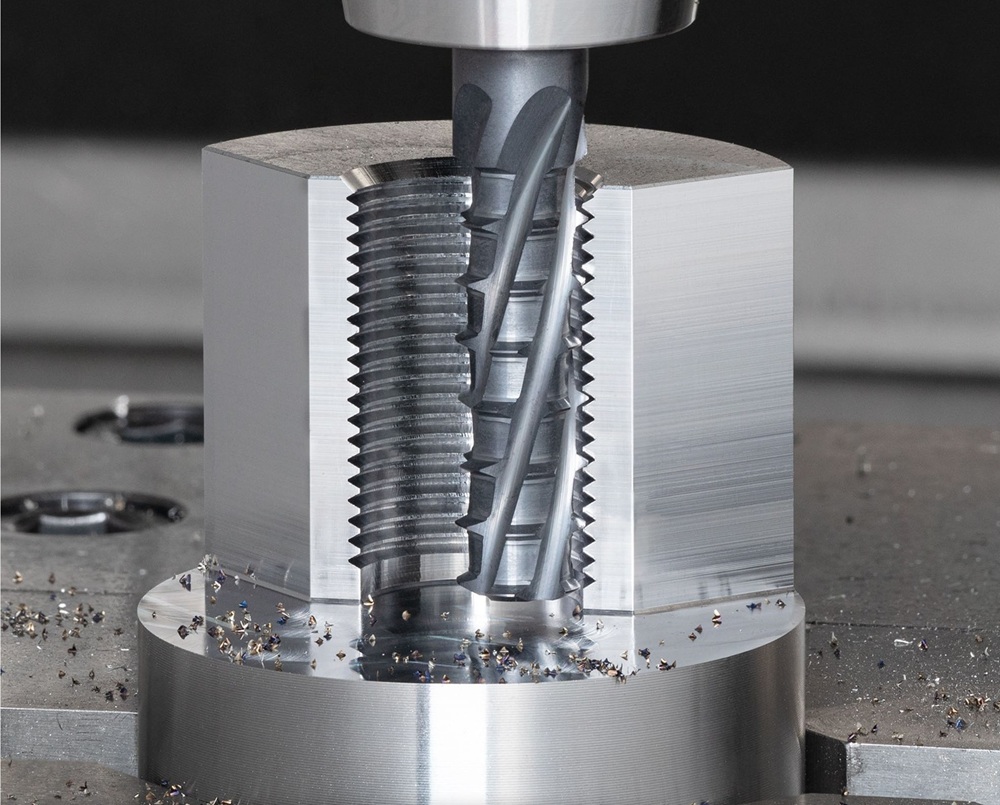
TaeguTec has expanded its TS-Thread solid-carbide thread milling range with four new tools: MTECBF, MTECH, MTECM and MTECK. Each addresses specific requirements in everyday and specialist threading applications. 

The TS-Thread series uses circular interpolation to produce threads in a single helical pass. A single tool can produce multiple thread sizes, while controlled entry conditions reduce radial cutting forces and the risk of tool breakage in difficult materials. 

The MTECBF features seven or eight flutes, depending on diameter, and is available from 12 to 24 TPI. Its geometry is optimised for blind-hole threading, while the high flute count enables higher feed rates. Combined with through-tool coolant, this capability supports efficient chip evacuation and reduced cycle times in high-volume production. 

For hardened steels and other difficult-to-cut materials, the MTECH combines threading and 45° chamfering in a single operation. Manufactured from solid carbide in TT5515 grade, it eliminates a separate chamfering process while maintaining accuracy and repeatability. It is available in ISO and UN standards, including M5, M6, M8 and M12, and UNC #6 to ½ inch. 

The MTECM and MTECK use multi-lead geometries for deep-hole threading. Notably, the MTECM has a triple-lead design, providing three times the thread pitch per revolution, while the MTECK uses a double-lead design. Both reduce cutting load per tooth and incorporate central coolant for chip evacuation and high-feed cutting. Both are available in ISO and UN standards. 

All four tools are available from stock, priced within the GAL system and manufactured to TaeguTec’s TS-Thread quality standards. Cutting data covers ISO material groups including steels, stainless steels, high-temperature alloys and non-ferrous materials. 

More information www.taegutec.com

Interchangeable-head PCD Mill Reduces Machining Costs

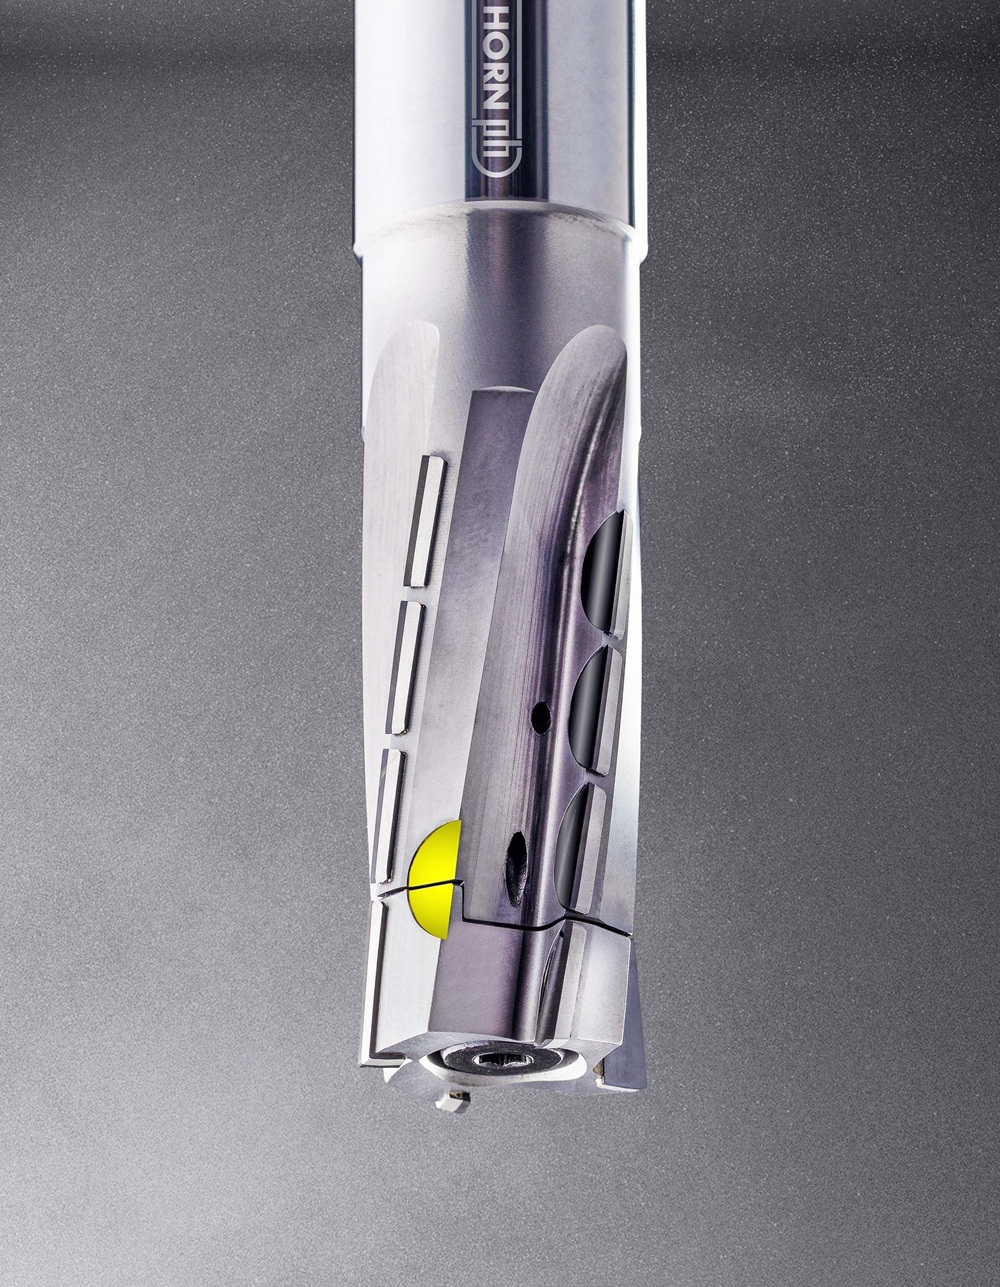
Cutting tool manufacturer Horn has introduced a modular range of PCD (polycrystalline diamond) end mills for machining aluminium, plastics and other materials in groups N (non-ferrous) and O (non-metallic). The system combines a reusable, solid-carbide shank and a PCD-tipped, interchangeable steel head. Availability in the UK and Ireland is through Horn Cutting Tools. 
 
Horn has designed the DM40 system to conserve resources and ensure cost-effective machining. The end cutting edges of the mill are among the main wear zones, while peripheral cutting edges longer than twice the tool diameter are susceptible to high lateral cutting forces, vibration and chipping. Notably, the ability to change just the head reduces follow-on costs compared with conventional monobloc tools, especially as the worn, brazed-on, PCD tips can be resharpened up to twice. 
 
By designing the cutter with a separate shank and head, Horn has ensured that the consumable cost is not only lower but also more predictable, making the tool system suitable for series production runs and automated lines. Users can quickly replace the head module on-site, so the tool is rapidly back into service, maximising spindle uptime. 
 
The head is attached to the shank via a central clamping screw that provides both a force-fit and a form-fit connection. Colour coding facilitates the identification of components, while a poka-yoke principle prevents assembly errors. The rigidity of the interface ensures precise machining, whether using a new or a resharpened tool, and the large axial rake angle enables smooth cutting and produces a smooth surface finish. 

More information www.horn-group.com