Harrison Silverdale Boosts Productivity with MecWash Duo

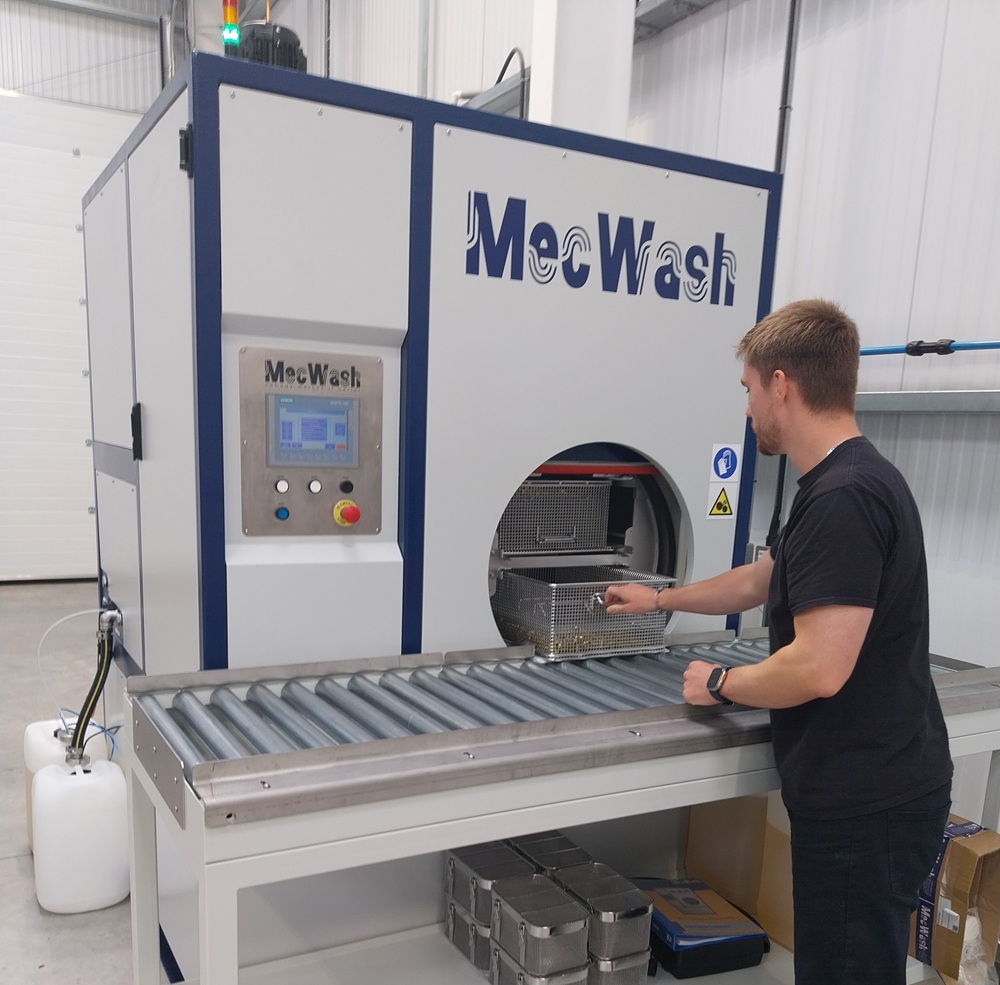
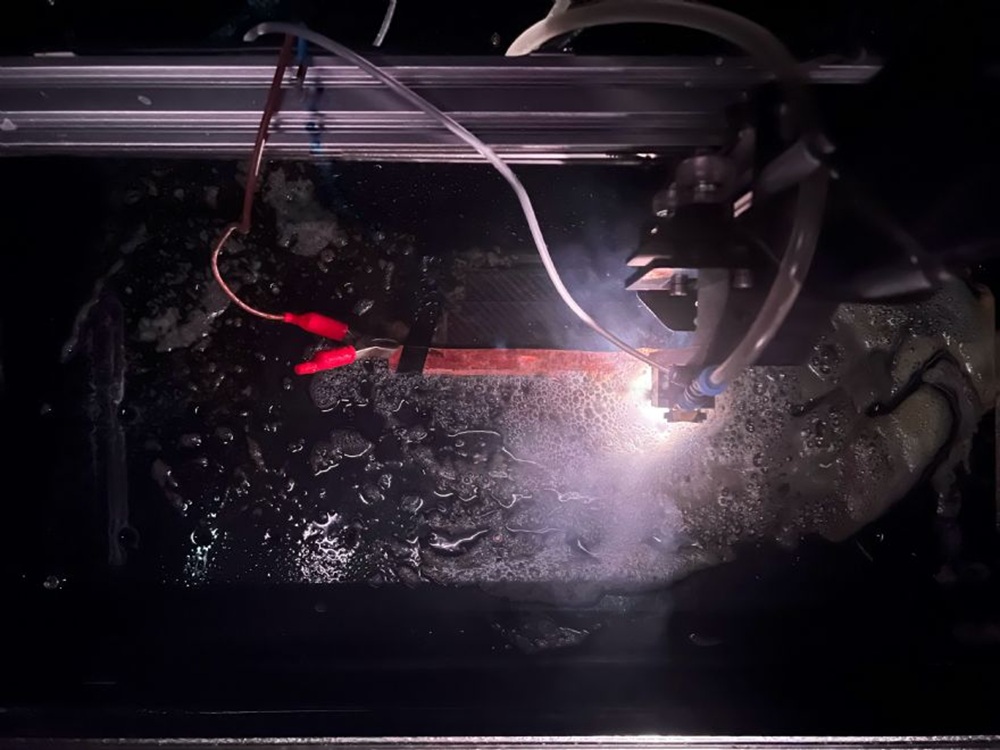
MecWash Systems has installed a Duo 400 parts washing system at fastener specialist Harrison Silverdale, providing additional cleaning capacity following investment in new manufacturing equipment. 

Harrison Silverdale has supplied engineered fastening solutions since 1982 and dispatches around 10 million parts each month to customers across more than 37 countries. Its design service also develops bespoke fasteners for customer applications, supported by three CAD engineers and on-site rapid prototyping. 

Following the purchase of a new Star sliding-head lathe, the company contacted MecWash to increase its cleaning capacity and ensure its specialist components could be cleaned to the required standards. 

“Our bespoke parts require absolute accuracy, so they must be cleaned to a high standard,” says Mark Harrison, managing director of Harrison Silverdale. “MecWash has a reputation for delivering extremely detailed component cleaning, so I contacted the team to discuss our requirements.” 

MecWash conducted trials to establish the most suitable solution before recommending the Duo 400. Installed at Harrison Silverdale’s newly built factory extension in Dronfield, the system is designed for cleaning high volumes of small turned parts. 

States Alan Atkinson, sales manager at MecWash. “The Duo 400’s combination of flood and spray washing, spray rinsing and hot-air drying provides thorough cleaning while handling dense baskets of components.” 

With a 400 x 450 x 600 mm wash chamber and 100 kg maximum load capacity, the system is helping Harrison Silverdale respond to growing demand from OEMs and distributors across Europe, the USA and Australasia. 

“The MecWash team has provided first-class support throughout the process,” concludes Harrison. “The Duo 400 has enabled us to fulfil growing customer demand while maintaining the speed of service that is critical to our offering.” 

More information www.mecwash.com 

UK Manufacturing is Growing. Now is The Time to Build on It

UK manufacturing entered autumn with another month of growth, strengthening the case for renewed investment in Britain’s industrial base. The S&P Global manufacturing Purchasing Managers’ Index rose to 51.9 in September from 51.7 in August, marking an 11th consecutive month of expansion. A reading above 50 indicates growth. 

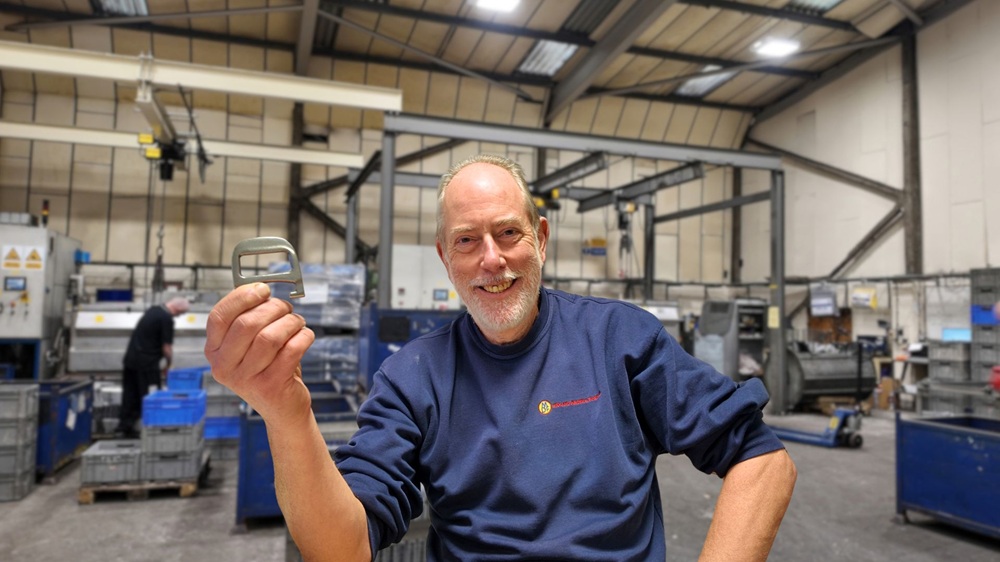
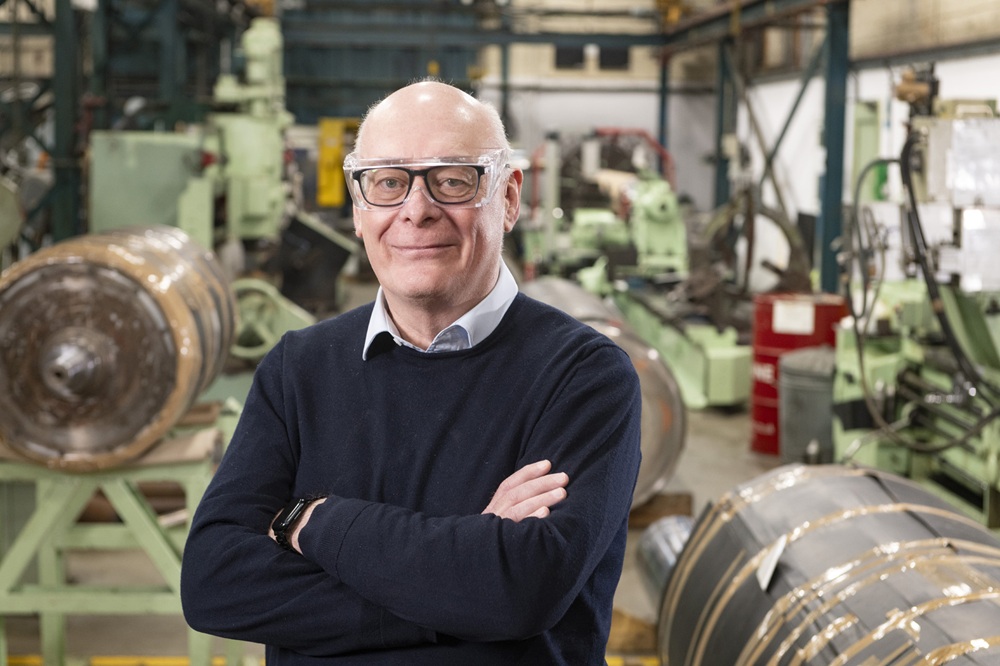
For Midland Deburr managing director Chris Arrowsmith (pictured), the figures highlight an opportunity to build capacity across the wider manufacturing supply chain: “Eleven months of manufacturing growth tells us something important. There’s work out there, companies are investing and there’s still tremendous engineering capability in Britain.  

While manufacturing growth is often measured through factory output, every finished component depends on a network of specialist suppliers. From its West Midlands facility, Midland Deburr provides vibratory deburring, component cleaning, solvent degreasing and vapour degreasing for manufacturers producing pressings, castings and machined components. 

“When customers become busier, that work travels through the supply chain,” Arrowsmith explains. “Machining creates components that need finishing, while pressings and castings require deburring and cleaning. Increased production ultimately means increased demand across specialist processes.” 

September’s survey recorded continued growth in new orders and exports, alongside longer supplier delivery times and higher input costs. Arrowsmith believes investment throughout the supply chain will be essential if manufacturers are to respond to rising demand. 

“If Britain wants higher manufacturing output, we have to think about capacity all the way through the supply chain,” he says. “That means machinery, skills, energy, premises, logistics and the specialist processes that keep components moving.” 

He adds: “Britain knows how to manufacture. We have the people, the engineering heritage and an extraordinary base of specialist companies. This is the time to use it, invest in it and give it every opportunity to grow.” 

More information www.midlanddeburrandfinish.co.uk 

LENS MANUFACTURER SEES CLEAR ADVANTAGES WITH TOOLING FROM TAEGUTEC

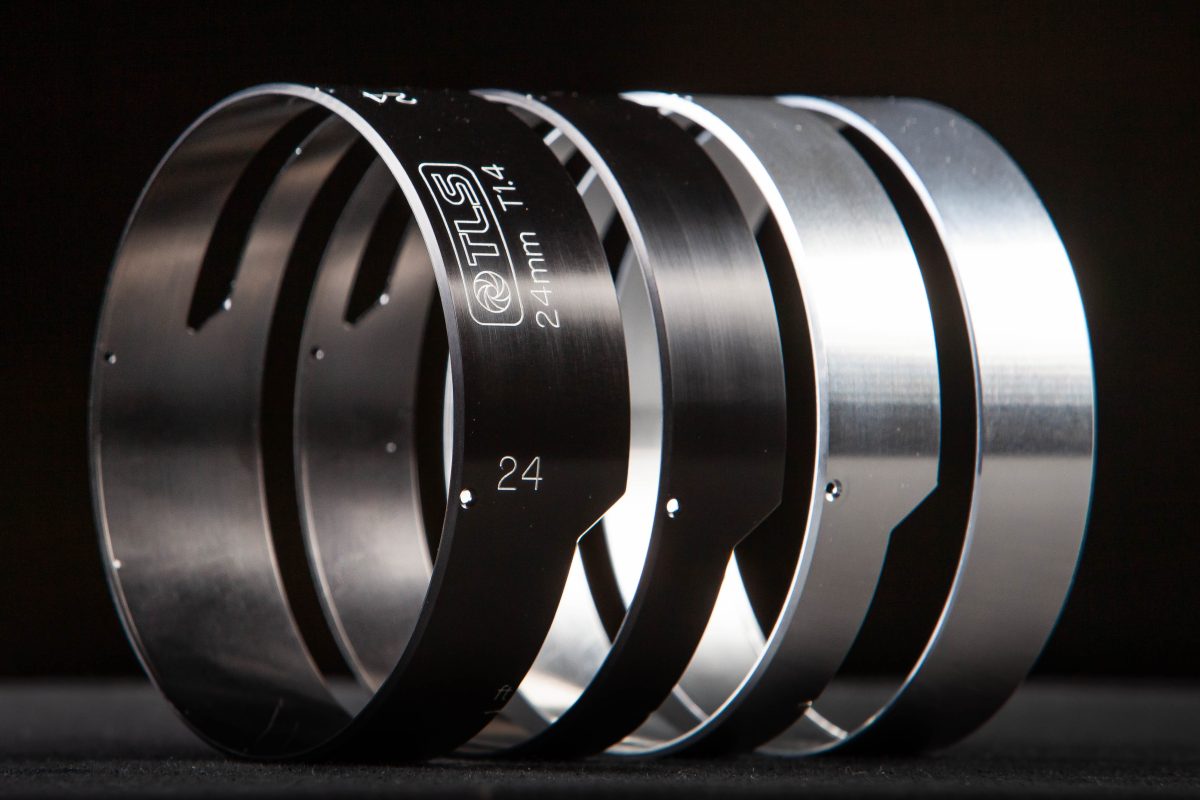
A Leicestershire cine lens specialist turned to TaeguTec’s aluminium turning grade to protect the mirror finish its camera housings demand and discovers an unplanned tool-life benefit along the way. Barwell-based True Lens Services adopted TaeguTec’s TTA101-grade VCGT 110304 FL turning insert after a trial addressed the hand-polishing bottleneck that had been adding time and labour to the production of its aluminium camera lens housings. 

True Lens designs, engineers and rehouses professional cinema lenses, converting vintage stills optics into modern cine tools used by filmmakers around the world, alongside lens servicing, repair and custom mechanical work carried out entirely in-house. The company supplies an international client base, and its engineering team won the Bert Easey Technical Award from the British Society of Cinematographers in 2025, recognition of the precision behind every lens leaving its workshop. 

Much of what True Lens machines is aluminium, produced on a pair of Nakamura-Tome AS200 turning centres in batches ranging from 50 to 500 pieces, depending on the job. Because the finished components are anodised, any mark or inconsistency left on the surface by the cutting tool is magnified, making a high-quality finish essential. 

TaeguTec technical sales engineer Brandon Kane had, in a previous role, helped install the pair of Nakamura-Tome AS200 machines already on the shop floor at True Lens Services. A conversation about that earlier work led the company to ask whether Brandon could take a look at a finishing problem on its aluminium parts. 

Working with an existing supplier’s uncoated turning insert, parts coming off the AS200s were failing visual inspection at a rate that meant roughly half of every batch had to be picked out and hand-polished before anodising. Every mark or burr had to be caught by eye by operators experienced enough to spot imperfections invisible to anyone else. Left unresolved, that meant additional manpower and time on every batch, a cost that never appeared as scrap or a cycle-time problem but sat quietly behind every job. 

The initial diagnosis pointed towards the machines themselves and a lack of rigidity in the process. Brandon had previously worked as a service engineer supporting Nakamura-Tome turning centres, so he was confident that was not the real cause. Aluminium finishing problems this consistent were more likely to be down to the insert than the machine. 

TaeguTec’s TTA101 grade, one of the first new products released since Kane joined the company, was proposed as a targeted trial rather than a wholesale tooling change. The VCGT 110304 FL insert would be introduced purely for the cosmetic outside-diameter finishing pass, with the existing tooling retained for roughing and general machining. 

TaeguTec’s TTA101 is a ta-C coated grade, applied at a thickness of less than 0.5 microns to preserve the sharpness of the cutting edge rather than rounding it off. With a hardness rating of HV5000 or higher, it also provides strong resistance to abrasive wear. Engineered specifically to resist the built-up edge that is a persistent problem when machining aluminium, the inserts rapidly made an impact. 

The trial insert was run on one Nakamura AS200 at a cutting speed of 525 m/min, a feed rate of 0.07 mm/rev and a depth of cut of 0.4 mm on the finishing pass. Feeds and speeds were fine-tuned specifically for surface quality rather than cycle time and slowed slightly from where they might otherwise have been. It was a trade-off True Lens Services was entirely comfortable with: getting the aesthetics and surface finish correct was the priority, not reducing cycle times. 

The formal trial report, compiled by True Lens Services and reviewed by TaeguTec, recorded a significant improvement in surface finish based on the customer’s own visual assessment. The more significant result, however, was tool life. With the previous insert, edges typically needed replacing after five to 10 parts. The TTA101 trial edge was still producing high-quality parts a month after the trial began and had not required changing. 

As the insert remains in service well beyond the initial trial period, this substantial improvement has yet to be benchmarked against its predecessor. With no insert failures to date, True Lens and TaeguTec still cannot quantify the tool-life gain. However, fewer insert changes, less operator intervention and more consistent production between tool changes have enabled True Lens Services to meet its surface finish requirements without switching machines, changing processes or resorting to excessive post-machining hand-finishing. 

The results were enough to move True Lens Services from trial to purchase. The company placed its first order, a box of 10 TTA101 inserts, and extended use of the TaeguTec grade from the single trial machine to both AS200s.  

Mark Lightbown, workshop supervisor at True Lens Services, says: “The TaeguTec inserts have made a massive difference, and we now run the TTA101 inserts on both machines. Whilst still early days, the savings from eliminating hand finishing are considerable. Equally important is process stability, with no need to tweak the process and full confidence that the surface finish on a batch run will not diminish. This is a huge benefit to our highly skilled machinists.” 

Parts finished with the TTA101 insert are now coming off the machine ready for anodising, removing the secondary hand-polishing step. For a business where every part is inspected, and where every imperfection is magnified by anodising, that translates into less labour, less handling and a more predictable route from machine to finished lens. 

With the trial proving a huge success, the next step for TaeguTec’s Brandon Kane is to identify further areas where the company’s cutting tools can deliver additional process and productivity improvements. 

More information www.taegutec.com 
£130k Grant 

TextureJet has been awarded a £130,000 Innovate UK grant to accelerate the development of ArcSlice, the company’s new and disruptive surface-finishing technology platform for composite and polymer surfaces. Awarded through Innovate UK’s ‘Advanced Manufacturing Supply Chains: Potential High Growth SMEs’ competition, the funding will support an intensive nine-month project designed to move ArcSlice another significant step towards commercial deployment. The ambition is clear: to help manufacturers improve process consistency and product quality while reducing waste, time and cost.  

More information www.tinyurl.com/33tysxey 

Defence Surge Exposes Gaps in Specialist Engineering Supply Chain

Engineering specialist BEP Surface Technologies is seeing a new wave of defence-related enquiries and RFQs for specialist grinding and hard chrome plating, highlighting vulnerabilities in the UK engineering supply chain as the government increases defence spending with SMEs. 

Andrew McClusky (pictured), managing director of BEP Surface Technologies, says: “We’re seeing a marked increase in defence enquiries. Defence manufacturers need specialist capabilities, but the supplier base they have relied upon has reduced. Capacity cannot simply be recreated when demand suddenly increases.” 

BEP’s experience echoes research it conducted earlier this year, which found that the number of independent electroplating businesses in the UK had fallen from 80 in 2015 to 67 in 2025 – a decline of more than 16%. At least seven of those remaining were already insolvent or winding down when the research was conducted. 

“When we published that research, our concern was that the UK was steadily losing specialist surface engineering capacity,” explains McClusky. “The enquiries we’re now receiving from defence reinforce why that matters. Grinding, plating and other specialist processes may sit several tiers down a supply chain, but they can be critical to manufacturing, refurbishing and maintaining high-value components.” 

McClusky believes increased defence expenditure represents a significant opportunity for British SMEs, but warns that scaling capacity will require investment in machinery and skills. 

“For an SME, increasing capacity requires considerable investment before the work is delivered. You need equipment, people and technical expertise, but also confidence in the long-term pipeline to justify that investment. Greater visibility of future defence demand would allow businesses to make those decisions earlier.” 

The MOD’s SME Action Plan, published in July 2026, aims to improve SME access to defence opportunities and increase supply-chain resilience. For 2027/28, the MOD is targeting £2bn in direct SME spend and £5.5bn indirectly through its supply chain. 

“The opportunity for British manufacturing is significant,” concludes McClusky. “Success should be measured not simply by how much defence expenditure reaches SMEs, but by whether it leaves Britain with more engineering capability, skilled people and stronger domestic supply chains.” 

More information www.bep-st.com