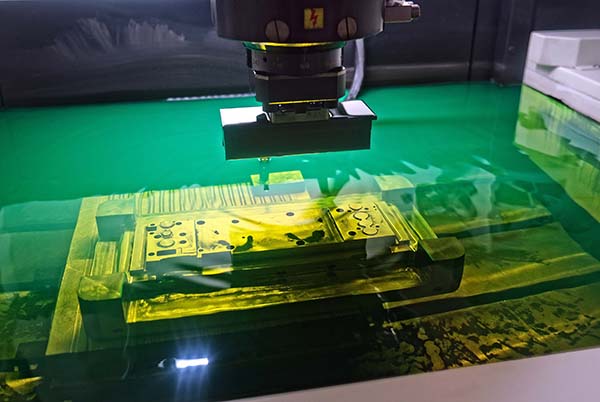
Second Makino die-sink EDM at BM

Although recent years have seen the increasing prevalence of hard milling at Whitchurch-based toolmaker and plastic injection moulding specialist BM Injection, there will always be a place in its tool room for EDM technology, with both die-sink and wire-erosion machines in use.

To take advantage of the latest EDM capabilities, the company recently decided to introduce a second spark-erosion machine, ordering a Makino EDAF3 HEAT from UK agent NCMT, which at the same time supplied a Makino five-axis machining centre.
“Our latest Makino die sinker is compact and 100% reliable, even on demanding jobs,” states director Tim Combes. “Furthermore, the machine is capable of producing parts to accuracies measured in low single-figure microns. The level of intelligence built into the machine means that one toolmaker can operate both of our die-sink machines and the Makino five-axis machining centre. Deep ribs can be produced quickly, reliably and with low wear on graphite electrodes. Constant attendance for manual intervention to avoid the onset of arcing, for example, is not required due to the spark gap monitoring and arc prevention circuitry.”
BM Injection’s machine was supplied with Makino’s optional high energy applied technology (HEAT), which incorporates dual high pressure capability, digitally controlled flush pumps and a large capacity, four-step filtration system to provide fast machining speeds and accuracy, even under poor or difficult flushing conditions, says NCMT.
Offering capacity of 450 by 351 by 351 in the X, Y and Z axis respectively, the latest EDAF includes a newly developed flushing control and increased feed rates up to 5000 mm/min in X and Y.
For further information www.ncmt.co.uk
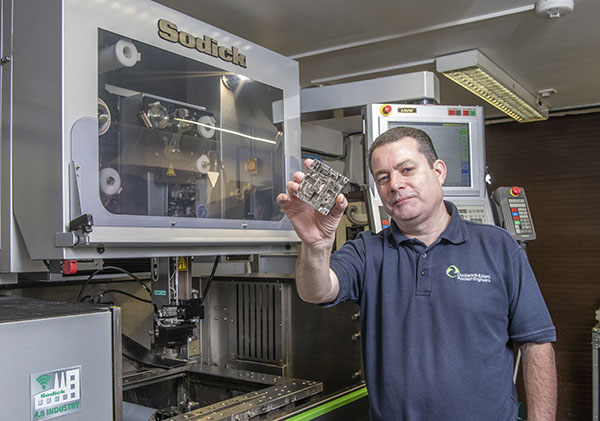
Sodick wire EDM reduces set-ups

A precision machining subcontractor has invested in its first Sodick wire-erosion machine, a VL600Q model supplied by Sodi-Tech EDM.

Berkshire-based Duckworth & Kent (Reading) Ltd, is using the machine to advance its wire-erosion capabilities, reduce the number of set-ups required, improve quality and repeatability, and introduce unmanned overnight operations.
“Our speciality is low-volume, high-quality precision components, often manufactured from a variety of difficult materials and with complex shapes that few others want to attempt,” explains sales director Stuart Gleeson.
The 15-employee business has relied on wire EDM for many years. However, when one of the company’s three wire EDMs recently required replacement, the company decided to evaluate a range of potential suppliers.
Reviewing three wire EDM machines, Gleeson quickly settled on the Sodick VL600Q, which seemed “a natural fit with the type of work” undertaken at the company.
“Unlike certain other machines, the generator on the Sodick model featured state-of-the-art technology,” he says. “In addition, we liked the rotary axis, which knew would help with complex parts. For instance, it’s already making light work of a lifting rod for the defence industry that is made from toughened steel. The rod features a series of diameters and squares that have to be concentric and straight to one another. There is also a thread and a yoke at the top for lifting. The rod is about 150 mm long and we recently produced a batch of 58 in a single set-up. Previously, this part would have required two EDM operations, or one EDM operation followed by milling and/or grinding. Saving a set-up probably equates to a cycle time reduction of one hour per part. So that’s 58 hours saved on one job alone, plus the quality is better as we avoid picking up the component and re-setting.”
For further information www.sodick.org

Hirschmann becomes Carl Hirschmann

Fluorn-Winzeln-based Hirschmann GmbH has reworked its corporate identity and become Carl Hirschmann GmbH, which is an expression of brand values and based on the name of the company’s founder. Carl Hirschmann GmbH develops and produces rotary tables and clamping systems that allow precise and efficient workpiece machining on EDM machines, as well as other machine tool types. The company recently concluded its financial year, increasing sales to more than €29 million.

“Confusion and a profile that does not do justice to the performance; that was too often the feedback from customers, staff and applicants, which in turn was the reason for our decision to completely rework the corporate identity of our company,” explains Rainer Harter, managing director and CTO.
The brand is a new interpretation and a tribute to the birth of the company in Stuttgart in 1957, which was founded by Carl Hirschmann. Since 1961, the company has been located in Fluorn-Winzeln.
“Today we go back to our roots,” says Andreas Jesek, managing director and CFO of the company. “As one of the top innovators in Germany, we needed a unique name that would create a high degree of recognition all over the world.”
All of the company’s products are high precision and developed and manufactured based on customer requirements. The emphasis to be the world leader can be found in Carl Hirschmann’s new motto “the precision benchmark in bearings, indexing and clamping solutions.”
For further information www.carlhirschmann.de

Sodick took best-of-breed EDMs to EMO

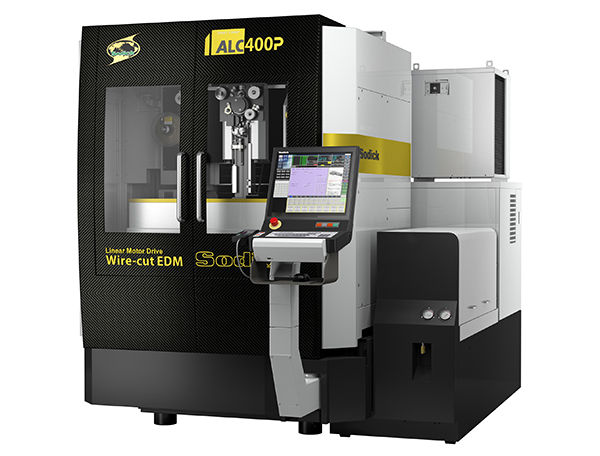
From its largest ever stand at EMO, Sodick said it took best-of-breed technology to the exhibition, with European debuts for the ACL400P high accuracy wire EDM and the ALC800G large-capacity premium wire machine. These newcomers were accompanied on the stand by two of Sodick’s most advanced EDM ‘big beasts’, the AG80L die sink and ALC800G wire machine, while automation options were demonstrated by the AG60L die sinker with robot.

The new ALC400P ultra-high-precision wire EDM incorporates as standard an inverter-type dielectric chiller which monitors and maintains the dielectric temperature to within ±1°, minimising the thermal effect inside the work area. An additional thermal sensor is installed inside the work tank for even more accurate temperature control.
As a further benefit, the CNC controller incorporates 2D pitch compensating software which automatically compensates pitch error in positioning every square of 10 x 10 mm. In addition, cross-type roller guides help provide high rigidity, high accuracy and longer life.
Elsewhere on the stand was the new ALC800G large-capacity premium wire EDM, which becomes the largest standard machine in the range with its 1250 x 1020 mm work tank and maximum workpiece weight of 3000 kg.
Incorporating the latest digital innovations in generator technologies and the use of advanced electrode materials, the ALC range provides major advances in cutting speed, accuracy and surface finish – made possible through Sodick’s in-house development and manufacture of all critical technologies, including linear motors, discharge power supply, NC unit, motion controller and ceramics.
For further information www.sodick.org

EDM with less electrode wear

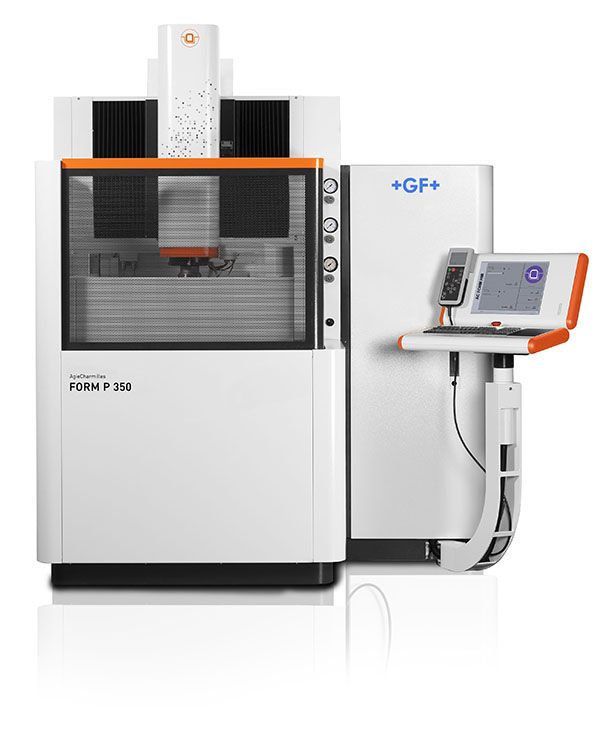
The Form P 350 die-sink EDMs from GF Machining Solutions feature precision-enhancing qualities and integrated technologies that are said to boost productivity and profitability.

Featuring a compact C-axis construction, fixed table and cast-iron frame, offers stability and force reduction to maintain a precise spark gap between the part and electrode. Regardless of part weight or dielectric volume, the machines deliver consistently high accuracies and surface finishes of Ra 0.1. Furthermore, integrated glass scales preserve repeatability and eliminate the need for recalibration and errors due to backlash and wear.
GFMS Form P 350 machines are equipped with the company’s intelligent power generator and Tecform module, which optimises each pulse to reduce electrode wear and generate high-quality surface finishes. Segment-dedicated technology eliminates the need to adjust the generator’s parameters.
The company’s iQ technologies control the erosion of graphite and copper electrodes, and help reduce costs. Real-time spark characteristic analysis and setting adjustment for pulse efficiency ensure wear-free spark erosion, precision, efficiency and greater control over the cost of the electrode, says the company.
Of note, the console’s AC Form HMI is based on Windows. Interactive graphics illustrate operations such as measurement and machining cycles for ease of use, while providing descriptions of machining targets, automatic selection of optimal technologies and dynamic parameter adaption.
GFMS Form P 350 machines are supplied with a four-position linear tool changer for System 3R macro tooling. An optional rotary tool changer can be specified that increases the number of electrodes to 160. The machines can also be paired with a System 3R WorkPartner 1+ robot for unattended night and weekend operations.
Offering X-, Y- and Z-axis travels of 350 x 250 x 300 mm, the machine accommodates workpieces up to 700 x 460 x 275 mm in size.
For further information www.gfms.com/uk