FANUC unveils latest-generation ROBOCUT

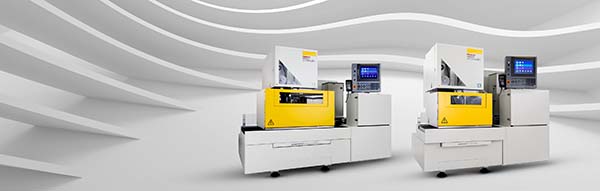
Thanks to a number of breakthroughs, FANUC says that its new ROBOCUT α-CiC series of wire EDM machines offers even higher levels of reliability, cutting speed, surface finish and dimensional precision. The many customer-centric enhancements include an entirely new mechanical structure, pitch error compensation across the complete work surface, a simplification in taper cutting adjustment and a hardened table as standard.

FANUC’s new ROBOCUT α-CiC provides users with a major accuracy boost thanks to the introduction of a high-precision pitch error compensation function. A special factory-calibrated compensation grid ensures pitch error correction over the entire X-Y table area – rather than a single central point – delivering a significant advantage in workpiece accuracy. It no longer matters where the workpiece is located on the work surface, the same level of optimum precision will result.

Improvements in taper cutting performance and ease of adjustment represent another notable advance. The traditionally complex operation of setting and adjusting the wire taper is now straightforward thanks to the use of a basic jig guided by on-screen instructions.

FANUC appreciates that process control is paramount to success in wire EDM operations. ROBOCUT control enhancements via the latest feature-rich FANUC iH Pro user interface focus on leveraging the advantages of the new mechanical structure to cut more efficiently. The new and improved user interface with its 15’’ widescreen, multi-touch LCD means that more intuitive operation is a further advancement, even for those relatively new to wire EDM.

Two model sizes are available: the ROBOCUT α-C400iC and ROBOCUT α-C600iC. Users can load workpieces with dimensions up to 1050 x 775 x 400 mm in the X, Y and Z axis respectively, with a maximum weight of 1000 kg.

For further information
www.fanuc.eu
CAMWorks adds wire EDM module

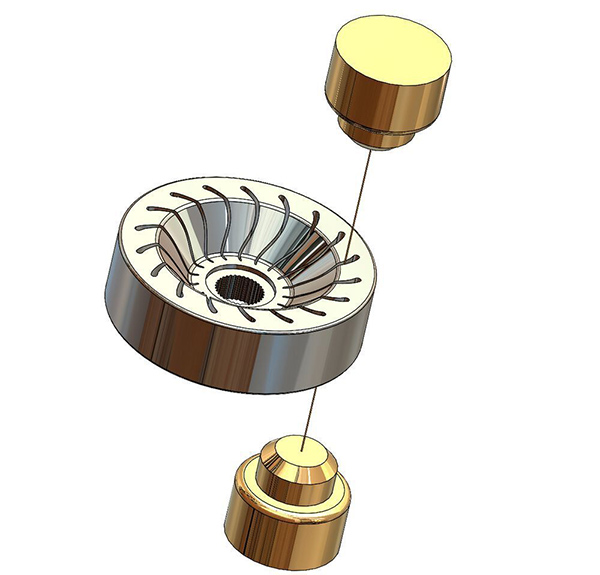
HCL Technologies has launched a wire EDM module for its CAMWorks suite of CADCAM software. The wire EDM module includes new functionality that takes the design model to G-code in one click. Once the user clicks the ‘Solid to G-code’ button, the system automatically searches the part for machineable features, identifies them, generates all the operations with the user’s preferences and settings (including tool offsets, cutting conditions and start holes), creates the toolpaths, and posts the G-code. Using the new wire EDM module, even complex two-axis parts, two-axis parts with tapers, and full four-axis wire EDM parts are now programmable in a single click.

The new CAMWorks wire EDM module also includes enhanced feature recognition for non-planar geometry. Instead of the user needing to project the geometry for the top and bottom of the part and create 2D sketches, the new wire EDM software uses geometry directly from the solid model to construct and create the correct top and bottom profiles automatically.

Additional highlights include automatic angular wire threading, support for SOLIDWORKS patterns, and automation based on face colours.

Automatic angular wire threading analyses the part and automatically recognises when angular threading would be required. It then creates the tool paths necessary to allow for angular threading of the wire and to machine the part.

Support for SOLIDWORKS patterns simplifies the NC code and streamlines the programming process by automatically identifying the patterns and utilising them to simplify the CNC program.

The technology based on face colours allows the user to easily identify and manage features that require programming, as well as the machining required.

For further information
www.camworks.com

Toolmaker puts trust in Vollmer

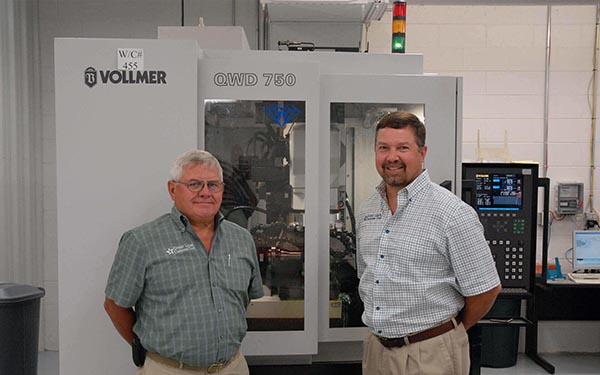
The name of US company Great Lakes Custom Tool Manufacturing (GLCT) says it all: GLCT produces special tools from its base on the shores of Lake Michigan, one of North America’s five Great Lakes. In order to machine tools and circular saws tipped with carbide or PCD, the toolmaker relies on 19 Vollmer machines. Recently, Vollmer supplied GLCT with a VPulse 500 wire erosion machine and a QR 270 disc erosion machine, among others.

“We have developed from a local sharpening service into an international manufacturer of special tools for woodworking and metalworking,” says GLCT CEO Ray Martin. “Our combination of products, services and support, along with a company culture of investment and innovation, is the reason behind our success both on the American market and globally.”

When GLCT expanded its business premises to almost 10,000 sq m in 2018, five new Vollmer machines arrived at the factory, including a VPulse 500 wire erosion machine with an external loading system for up to 16 tools. This successor to the QWD range can sharpen significantly faster than its predecessor thanks to a new type of generator technology for PCD cutting edges.

“With the VPulse generator, the new machine is at least 20% more productive than our previous QWD machines,” says Martin. “What’s more, the surface quality of the cutting tools is better than ever, and the VPulse 500 has the latest Vollmer programming system, which offers an intuitive user interface. This means that we not only save production time, but avoid machining errors.”

Even in 2020, a year when Covid-19 was wreaking havoc across the world, a new Vollmer machine reached Lake Michigan: a QR 270 disc erosion machine that can sharpen the tooth tops of PCD-tipped circular saw blades.

For further information
www.vollmer-group.com

EDM reduces electrode use by 40%

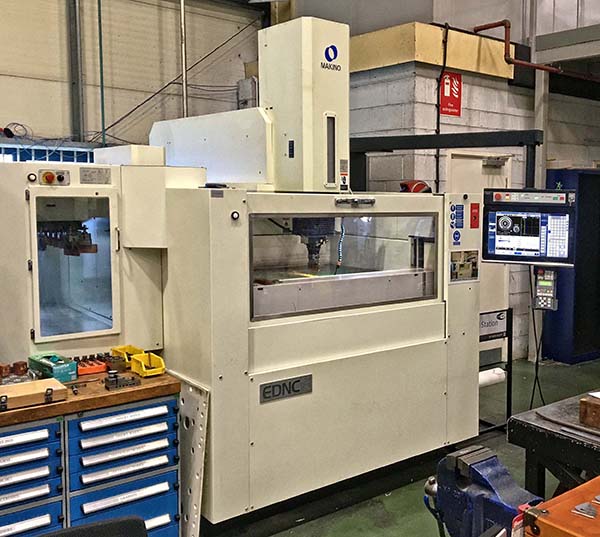
NCMT has supplied a Japanese-built Makino spark erosion machine to the tool-room facility of cable management products solutions provider HellermannTyton, where it is now busy producing plastic injection moulds. The company’s tool-room engineer, Rob Pickup, who has 20 years’ EDM experience, says that the super-low wear rate of the copper electrodes using the Makino has cut their usage by around two-fifths, lowering production costs and speeding mould manufacture through the need for fewer electrode changes.

HellermannTyton’s tool room in Manchester supplies multi-cavitation injection moulds produced mainly from 52 HRc Stavax to meet the demands of the local production operation. The cable ties, fir trees, clips and other cable management solutions produced in the UK factory serve most end-user markets.

Spark erosion is inherently a slow manufacturing process and the tool room is keen to avoid a bottleneck developing as demand for the company’s cable management products continues to rise.

“We wanted to increase sinking capacity, not so much for our higher speed applications, but more for producing very high accuracy moulds,” says Pickup. “The radius on the peak of the tooth form is less than 50 µm, so we needed a die-sink EDM on which electrode wear rate is super-low. We found that performance in the Makino EDNC6, which probably has the best generator on the market.

“An average job here uses up to 15 electrodes on one of our other die-sinking machines, but on the Makino we can rely on that number being reduced to nine,” he continues. “It represents a big saving in their manufacture, as well as in the copper used and the number of tool changes. Moreover the result is more repeatable, so there is never any rework.”

For further information
www.ncmt.co.uk

Growth prompts new investment

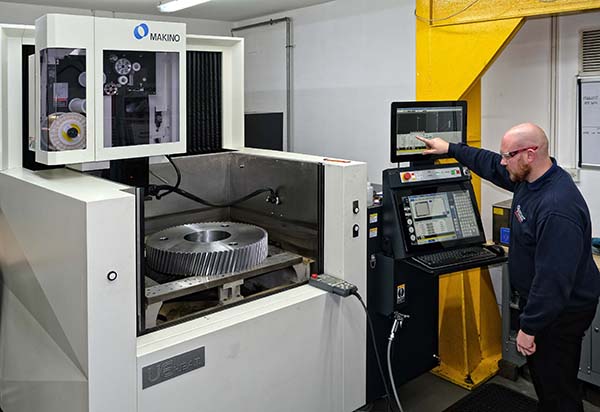
Oldham-based Hopwood Gears, which derives half of its turnover from the manufacture of steel, aluminium and plastic gears – and the remainder from high precision subcontract work (particularly for the robotics and defence sectors) – has invested in a new Makino U6 H.E.A.T wire EDM machine from NCMT. The machine, which is capable of long periods of unattended operations, will help the company boost production capacity.

Behind the latest investment by the family-run firm was a doubling of turnover to £4m over the past two years, despite the pandemic.

Operations director Calum Baines says: “We first became aware of NCMT when we attended a gear seminar at their Coventry technical centre and were impressed with the level of technology, as well as the build quality of the machines.”

The new Makino at Hopwood spends 90% of its time in gear production activities, mainly for the wire-cutting of keyways in hardened steel.

Hopwood Gears’ managing director Cory Hopwood says: “As a result of our rapid growth, there was a shortfall of EDM capacity and we were constantly running behind with orders, but that situation has changed dramatically.”

He says that the Makino U6 H.E.A.T. is 30% quicker at cutting than the other EDM machine on-site and uses 30% less wire. The higher speed is due to a combination of machine rigidity and two large, high-pressure flushing pumps that are able to evacuate chips efficiently, allowing the wire to be pushed harder. Unusually, it is possible to mount a 16 kg wire spool that lasts for the whole of a ghost shift, without need for a space-hungry side loader.

For further information
www.ncmt.co.uk