Winbro strikes partnership deal

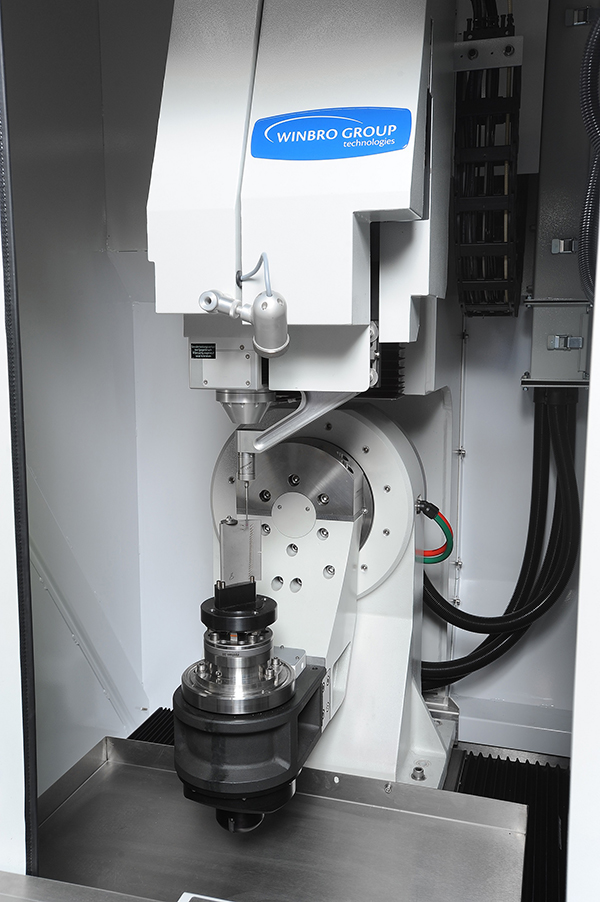
Machine tool manufacturer Winbro Group Technologies has signed a partnership deal with the Engineering Technology Group. The new agreement will streamline and enhance the route to market for Winbro solutions and provide greater accessibility for customers.

Winbro Group Technologies is a specialist in the design and manufacture of advanced machines and technologies based on non-conventional processes that include high-speed EDM drilling and ECM (electro-chemical machining). The company offers a range of high-technology machining systems for the production of cooling holes and other forms and features in turbine components, thus earning a strong reputation in the aerospace, industrial gas turbine and power generation sectors, as well as electronics, medical, electric vehicles and battery technology.

Further solutions offered by Winbro include laser drilling, cutting and ablation, and creep-feed grinding. The company has a manufacturing and assembly facility in Coalville, with another facility in Rock Hill, SC, USA where Winbro can configure machine systems either as a single process or dual complementary process machines.

Winbro Group’s chief commercial officer Andy Lawson says: “The partnership with ETG is an ideal marriage of Winbro’s technology innovations in non-conventional machining and ETG’s broad base across many sectors. Wherever ETG’s customers have a problem that cannot be addressed with conventional machines, Winbro can potentially offer a solution.”

ETG’s group managing director Martin Doyle adds: “By forming this partnership, ETG will identify opportunities whereby manufacturers across the entire spectrum can benefit from investing in Winbro machine tools. The ETG team is excited for the opportunity to work with this key producer of machine tools, and once again promote and support the UK manufactured brand.”

For further information
www.winbrogroup.com
www.engtechgroup.com
Micro-hole EDM gives boost

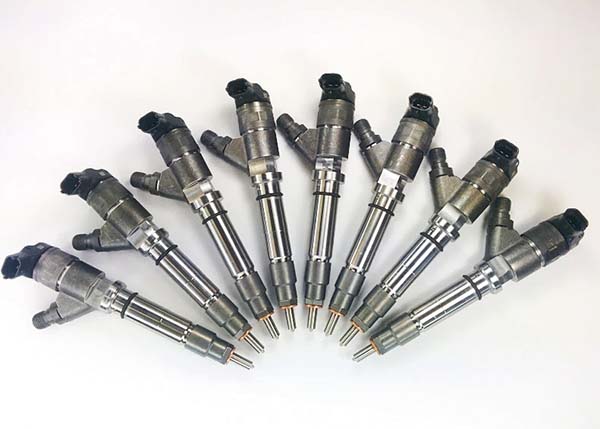
Dynomite Diesel Products, a US-based company with a 20-year history in the manufacture of high-performance diesel fuel injectors, has recently acquired an ONA MF5 micro-hole EDM machine (ONA machines are available in the UK from CNC International).

Until now, producing the high-flow injectors was very expensive and took about 2 hours using a process based on an extrusion machine. The company needed a solution to optimise costs by reducing the manufacturing time, while bringing precision and consistency to the product. By adding the ONA MF5 EDM model to its operations, Dynomite has reduced the cycle time to less than 5 minutes, increased process cost-effectiveness and extended the useful life of its extrusion machine. Furthermore, this new procedure, which combines the company’s extrusion machine and new MF5, makes the final calibration much faster and more consistent, injector-to-injector.

For Lenny Reed, owner of Dynomite, the addition has countless benefits: “The machine offers us to stay abreast of the ever-changing requirements of this sector. We now have the latest technology to manufacture even more precise injectors, which will enable us to create more innovative products in the future.”

Regarding cost and time optimisation, he adds: “We can predict more accurately the time spent on each product, and the costs are very good, which is great for the future as we anticipate the useful life of the machine to be around 20 years.”

Ultimately, the owner is thrilled with his investment as “this machine provides our business with possibilities we never dreamed of.”

For further information
www.onaedm.com

EDM essential at Raysun

Raysun Innovative Design, a Rugby-based end-to-end precision engineering, design and manufacturing business, has invested in a second Mitsubishi EDM machine, an MV1200S model supplied by the Engineering Technology Group (ETG). The new machine sits alongside its existing MV2400S with simultaneous 6th axis rotary indexing unit.

Charles Ray, director at Raysun Innovative Design, says: “We purchased our second Mitsubishi because we had a good experience with the first machine, the larger MV2400S. This first machine was a bit of a chance for a small business like ours, buying a ‘top-end’ machine tool. However, after we had invested, we found that we were using the machine for all kinds of applications that at first didn’t appear obvious.

“The quality of the Mitsubishi machines really is the core of our business,” he continues. “We rely on them perhaps more heavily than we should, but if we are measuring a part on the CMM and get a questionable result, we look at the CMM first rather than the EDM machine. This demonstrates our reliance and faith in this particular platform.”

As an engineering group, Raysun Innovative Design admits it had very limited previous knowledge of EDM.

“I am not a programmer myself, but my colleagues tell me the control is considerably upgraded from the previous version on the MV2400S that was installed some years back,” says Ray. “From a quality viewpoint, it is much more accessible for maintenance routines; in fact, we can add our own maintenance requirements into the control. If we were in the market for another wire EDM machine, which we may be in the future, there is little doubt that Mitsubishi would be top of the list for consideration.”

For further information
www.engtechgroup.com

Wire proves 10% faster in trials

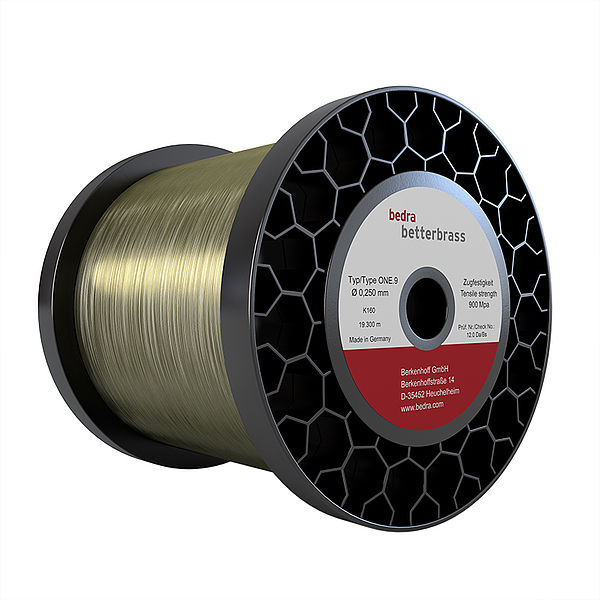
Betterbrass, the next-generation brass alloy wire launched recently in the UK by Erodex, has helped users to increase cutting speed by up to 10% in early trials. Manufactured in Germany by Bedra (Berkenhoff), Betterbrass benefits from novel alloy and casting technology, along with a specially developed annealing process. The wire is plug-and-play on all machine types.

“Since its launch, the Betterbrass wire range has received a positive response from customer trials, meaning that we can now provide EDM subcontractors with a cost-effective step up from standard brass wire,” explains Josh Bye, sales engineer at Erodex UK. “As UK industry starts to recover from the effects of the COVID-19 pandemic, we were keen to introduce a cost-effective wire to the market that facilitates increased performance. Customers will save money by using the wire, as any increase in wire speed ultimately means less wire consumption.”

Luke Hobbs, director of HLP Engineering Solutions in Halesowen, has experienced first-hand the benefits of using both the Gapstar and Betterbrass ranges from Erodex.

“Simply put, Gapstar is the best wire we have ever used on our Sodick machines from a performance and speed perspective,” he says. “We find it ideal for cutting punches and other long-running jobs. However, we found that Betterbrass is excellent on threading and, for the small increase in the cost of the wire, offers decent speed improvement of around 10-12% over standard brass wire using the same settings. When the job dictates, we will certainly use this wire again.”

For further information
www.erodex.com

Slug management made easy

GF Machining Solutions says that its new Automatic Slug Management (ASM) makes true uninterrupted and unmanned wire EDM operations a reality.

Left to their own devices, slugs will fall on to the lower head of an EDM machine. This effect can cause a crash or trigger alerts that cause the machine to stop. To aid prevention, CAM programs include ‘tabs’ to keep the slug connected to the workpiece during machining operations. Once completed, operators remove the tabs and slugs, but such manual intervention prevents true unmanned operation. At best, manufacturers can achieve rough cutting of parts overnight, but will need to wait until operators are available to remove the slugs and run trim and finishing passes.

With ASM, manufacturers can machine parts (roughing and finishing) overnight, and the technology is particularly suited to die-stamping applications and other small cavity operations. The process begins with a complete roughing pass that leaves no welds or tabs but sees the machine’s lower head prevent the slug falling into the tank while a device retrofitted to the upper head descends; this blows high-pressure air over the slug, which creates suction and allows the slug to be pulled from the part and deposited away from the machine.

Although ASM is slower than the manual alternative, the fact that it requires no human intervention means that manufacturers can load up machines at night with raw material and return the next morning to completed components.

For further information
www.gfms.com