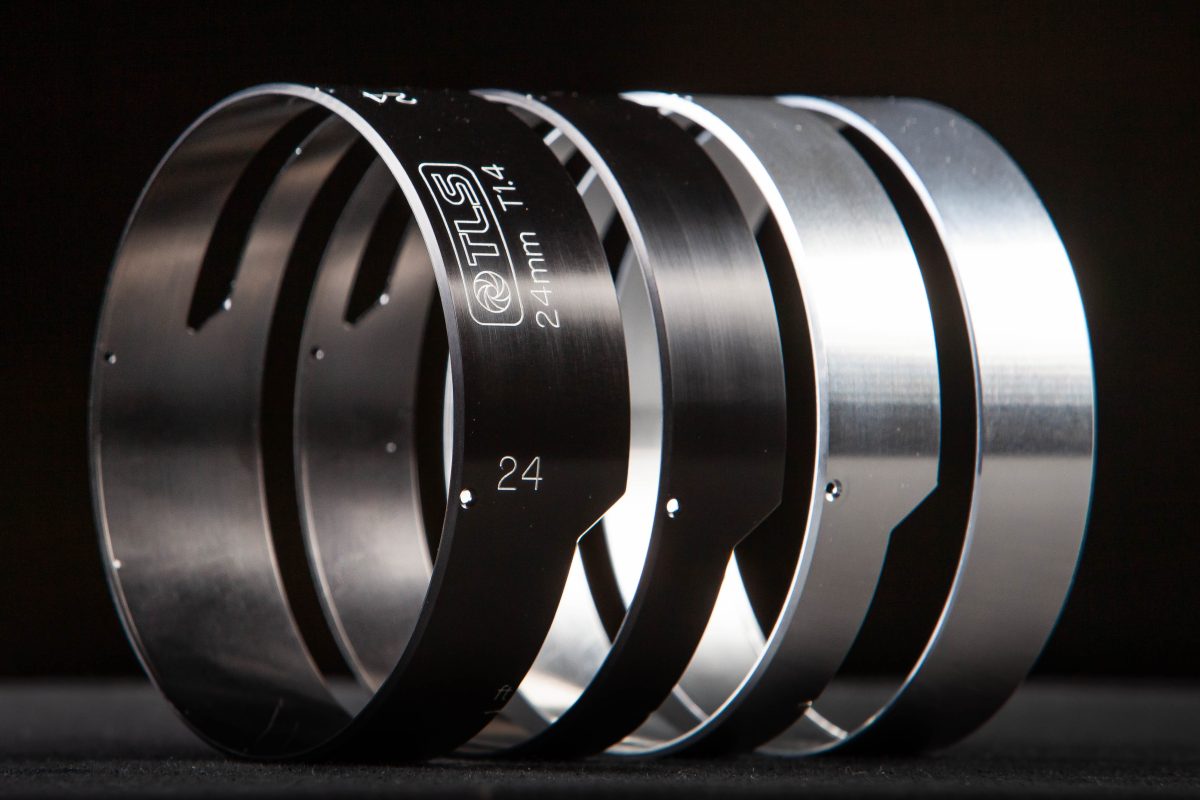
A Leicestershire cine lens specialist turned to TaeguTec’s aluminium turning grade to protect the mirror finish its camera housings demand and discovers an unplanned tool-life benefit along the way. Barwell-based True Lens Services adopted TaeguTec’s TTA101-grade VCGT 110304 FL turning insert after a trial addressed the hand-polishing bottleneck that had been adding time and labour to the production of its aluminium camera lens housings.
True Lens designs, engineers and rehouses professional cinema lenses, converting vintage stills optics into modern cine tools used by filmmakers around the world, alongside lens servicing, repair and custom mechanical work carried out entirely in-house. The company supplies an international client base, and its engineering team won the Bert Easey Technical Award from the British Society of Cinematographers in 2025, recognition of the precision behind every lens leaving its workshop.
Much of what True Lens machines is aluminium, produced on a pair of Nakamura-Tome AS200 turning centres in batches ranging from 50 to 500 pieces, depending on the job. Because the finished components are anodised, any mark or inconsistency left on the surface by the cutting tool is magnified, making a high-quality finish essential.
TaeguTec technical sales engineer Brandon Kane had, in a previous role, helped install the pair of Nakamura-Tome AS200 machines already on the shop floor at True Lens Services. A conversation about that earlier work led the company to ask whether Brandon could take a look at a finishing problem on its aluminium parts.
Working with an existing supplier’s uncoated turning insert, parts coming off the AS200s were failing visual inspection at a rate that meant roughly half of every batch had to be picked out and hand-polished before anodising. Every mark or burr had to be caught by eye by operators experienced enough to spot imperfections invisible to anyone else. Left unresolved, that meant additional manpower and time on every batch, a cost that never appeared as scrap or a cycle-time problem but sat quietly behind every job.
The initial diagnosis pointed towards the machines themselves and a lack of rigidity in the process. Brandon had previously worked as a service engineer supporting Nakamura-Tome turning centres, so he was confident that was not the real cause. Aluminium finishing problems this consistent were more likely to be down to the insert than the machine.
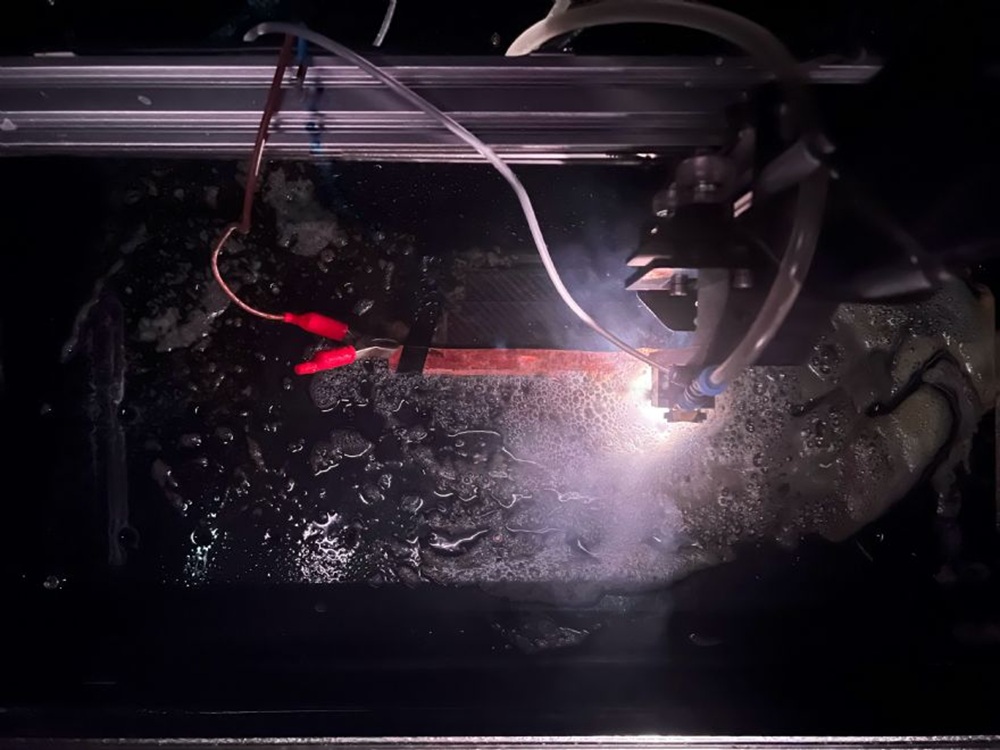
TaeguTec’s TTA101 grade, one of the first new products released since Kane joined the company, was proposed as a targeted trial rather than a wholesale tooling change. The VCGT 110304 FL insert would be introduced purely for the cosmetic outside-diameter finishing pass, with the existing tooling retained for roughing and general machining.
TaeguTec’s TTA101 is a ta-C coated grade, applied at a thickness of less than 0.5 microns to preserve the sharpness of the cutting edge rather than rounding it off. With a hardness rating of HV5000 or higher, it also provides strong resistance to abrasive wear. Engineered specifically to resist the built-up edge that is a persistent problem when machining aluminium, the inserts rapidly made an impact.
The trial insert was run on one Nakamura AS200 at a cutting speed of 525 m/min, a feed rate of 0.07 mm/rev and a depth of cut of 0.4 mm on the finishing pass. Feeds and speeds were fine-tuned specifically for surface quality rather than cycle time and slowed slightly from where they might otherwise have been. It was a trade-off True Lens Services was entirely comfortable with: getting the aesthetics and surface finish correct was the priority, not reducing cycle times.
The formal trial report, compiled by True Lens Services and reviewed by TaeguTec, recorded a significant improvement in surface finish based on the customer’s own visual assessment. The more significant result, however, was tool life. With the previous insert, edges typically needed replacing after five to 10 parts. The TTA101 trial edge was still producing high-quality parts a month after the trial began and had not required changing.
As the insert remains in service well beyond the initial trial period, this substantial improvement has yet to be benchmarked against its predecessor. With no insert failures to date, True Lens and TaeguTec still cannot quantify the tool-life gain. However, fewer insert changes, less operator intervention and more consistent production between tool changes have enabled True Lens Services to meet its surface finish requirements without switching machines, changing processes or resorting to excessive post-machining hand-finishing.
The results were enough to move True Lens Services from trial to purchase. The company placed its first order, a box of 10 TTA101 inserts, and extended use of the TaeguTec grade from the single trial machine to both AS200s.
Mark Lightbown, workshop supervisor at True Lens Services, says: “The TaeguTec inserts have made a massive difference, and we now run the TTA101 inserts on both machines. Whilst still early days, the savings from eliminating hand finishing are considerable. Equally important is process stability, with no need to tweak the process and full confidence that the surface finish on a batch run will not diminish. This is a huge benefit to our highly skilled machinists.”
Parts finished with the TTA101 insert are now coming off the machine ready for anodising, removing the secondary hand-polishing step. For a business where every part is inspected, and where every imperfection is magnified by anodising, that translates into less labour, less handling and a more predictable route from machine to finished lens.
With the trial proving a huge success, the next step for TaeguTec’s Brandon Kane is to identify further areas where the company’s cutting tools can deliver additional process and productivity improvements.
More information www.taegutec.com