Machining large composite motorsport parts

Headquartered in Fontwell, West Sussex and operating from four sites near the south coast of England, GTR Composites is known for supplying Formula One teams with carbon-fibre components and assemblies. The subcontractor has produced lightweight chassis and other large parts from composite materials for a long time, but at the beginning of 2021 it started final-machining them to tolerances measured in tens of microns.

The introduction of this new service followed the purchase of a German-built Zimmermann FZU400 five-axis machining centre, installed at GTR’s Bognor Regis facility at the end of 2020 by UK sales and service agent Kingsbury. Having a 4000 x 3000 x 1250 mm working envelope, the portal machine was selected from a shortlist of three due to its ability to hold very high accuracy.

For example, a positional tolerance of 50 µm is achieved on features across a full chassis, while holes and counterbores are held to within 10 or 20 µm. As the components are of high value, GTR adopts a policy of having an operator permanently in attendance, even when the FZU400 is running overnight.

Simon Kingdon-Butcher, joint owner (with John Biddlecombe) of GTR, says: “The Zimmermann machine stood out in terms of its rigidity, which translates into the tight tolerances we are able to hold when cutting carbon fibre. We’re able to impress our customers by hitting really tight limits that our competitors cannot achieve.

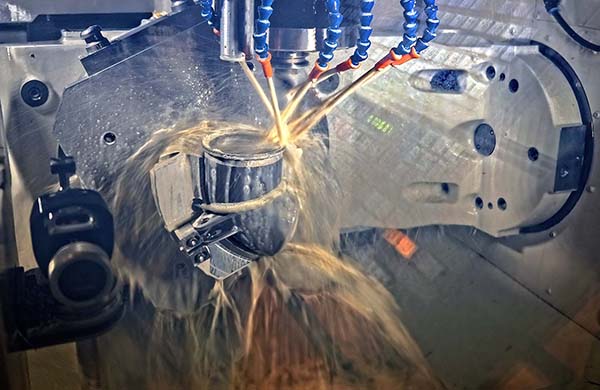
“High spindle power – 34 kW continuous/41 kW peak – enables us to rough aluminium moulds, while spindle speeds up to 24,000 rpm means their surfaces can be finish-machined to very high quality using minimum quantity lubrication,” he adds. “MQL also enables us to mill and drill carbon fibre components containing titanium or aluminium inserts in the presence of a specific type of coolant approved by our customers.”

For further information
www.kingsburyuk.com
IMSA insists on NSK products

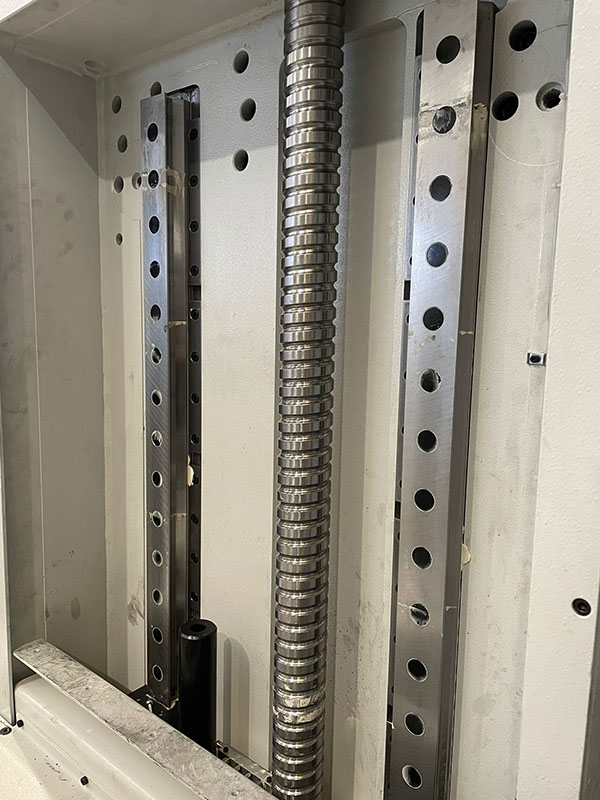
NSK’s ground ball screws, linear roller guides and super-precision ball bearings are helping IMSA to consolidate its market position in the field of specialised deep-hole drilling machines, which are particularly popular for mould-making applications in the automotive sector.

“Our partners have always played a fundamental role in all of the technological innovations that distinguish our company,” says Marco Colombo, head of the technical department at IMSA. “In order to put our design ideas into practice, we use top-quality components that can guarantee the best performance and reliability over time. For example, NSK has always been our point of reference in motion control throughout the evolution of our machines. The availability of optimal-quality NSK bearings, ball screws and linear guides has allowed us to build the highest performance machines in our sector.”

One of IMSA’s most recent innovations has been the development of a rotary-tilting table, which allows the machining of moulds in five axes using just one clamping position, further reducing manufacturing time. MF1000-3T EVO, a deep-hole drilling machine for small to medium automotive moulds up to 2.5 tonnes in weight, is the first model to be equipped with this solution. Here too, IMSA is using NSK’s latest-generation solutions to achieve the very high performance required.

“To transform axial movement into rotary movement, we use two 63 mm diameter NSK ZSS series ground ball screws,” says Colombo. “Compared with the ball screws of previous generations, they guarantee greater rigidity and perform better in terms of speed and load capacity. As a result, the machine’s working axes can move at feed rates of up to 30 m/min.”

For further information
www.nskeurope.com

Big savings and reduced lead time

A few years ago, T&R Precision Engineering in Foulridge, Lancashire, started manufacturing parts from Inconel 625 castings for the hot air side of the GE-Safran LEAP-1A turbofan that powers the Airbus A320neo family of single-aisle jets. The problem was that the work involved a labour-intensive sequence of three or four operations on separate machines.

A more efficient process route for the drilling, milling, chamfering and turning operations was therefore sought by the aerospace components supplier, which employs more than 70 people. The ideal solution identified by engineering manager Graham Gilbert involved the purchase from NCMT of an Okuma MU5000V five-axis VMC equipped with a Dutch-made Cellro 30-station pallet storage and retrieval system served by a six-axis industrial robot.

Managing director Tim Maddison says: “The improvement in production performance has been enormous across the four different LEAP-1A castings that we machine. We now produce all components in a single hit as part of a one-hour cycle, which means that eight parts are now ready the same day rather than after a week. The substantial saving in lead-time is accompanied by vastly less workpiece handling and work-in-progress on the shop floor, while at the same time fewer free-issue Inconel castings need to be supplied by our US customer at any given time, saving them money as well.”

A further benefit is a 50% reduction in total processing time compared with producing the parts in three or four separate operations. An additional saving that Maddison describes as “massive” comes from inspecting every completed part on the VMC in a 10-minute routine at the end of the cutting cycle. So instead of 100% inspection on a CMM, only one part per day now needs checking offline.

For further information
www.ncmt.co.uk

Heller releases HF 3500 Gen2

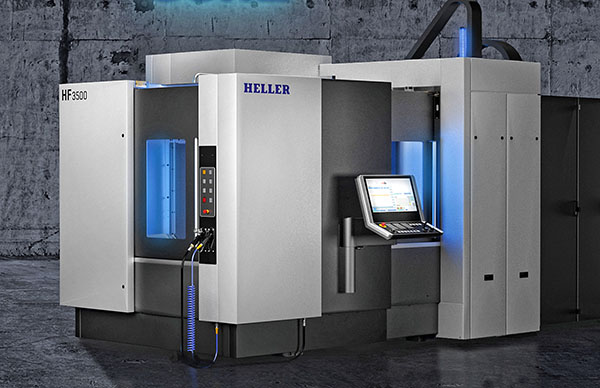
German-owned Heller Machine Tools, whose factory in Redditch produces selected four-axis and five-axis horizontal machining centres (HMCs) for world markets, has released its second-generation HF 3500 five-axis horizontal machining centre. The HF 3500 Gen2, with its 710 x 750 x 710 mm working volume, as well as the larger HF 5500, are available with a fixed table or an automatic pallet changer. Both are built in Redditch and incorporate a multitude of improvements over the previous-generation model. The machines are available with either an HSK-A63 or HSK-A100 tool interface in three versions – POWER, SPEED and the new PRO option – the latter intended for long periods of simultaneous five-axis machining.

Designed to raise cutting performance, innovations in the second generation include: an approximate halving of the minimum distance between the spindle nose and the centreline of the 225° swivelling trunnion; the availability of twin motors and ballscrew drives for moving the trunnion/rotary table assembly in the Z axis, with position feedback via linear scales; and the offer of six new spindles produced in an automated facility at Heller’s headquarters in Nürtingen.

Other notable improvements include increased stiffness of key components, shorter chips-to-chip times and faster tool change from a chain-type magazine with up to 240 pockets or a rack-type magazine with up to 405 positions. The high-end PRO package additionally offers 10 m/s2 acceleration in X, Y and Z.

The guideways employ linear roller bearings, enabling high dynamics and rapids up to 90 m/min, while the rotary axes have direct drives and YRT bearings. There is also increased feed force in the Z axis, dynamic motors driving the rotary axes and the option of adding a turning function using a high-speed rotary torque table.

For further information
www.heller.biz

Precision gears from a single source

NAMCO was founded in 1976 to serve the growing demand for precision machine components, custom gears and transmission parts. With locations in Edmonton, Canada, and Chardon, Ohio, the company employs more than 75 skilled workers who manufacture products for customers in the paper, oil and gas, mining, and other industries. Since 2019, NAMCO has invested in 15 CNC machines from DMG Mori, including a DMC 125 FD duoBLOCK for gear milling with gearMILL software and two Taiyo Koki machines for grinding.

“Thanks to gearMILL gear-cutting software, we can now manufacture our special solutions quickly and, above all, easily,” states Bernard Vukovic, managing director NAMCO Machine & Gear Works. “Furthermore, thanks to the mill-turn technology on the DMC 125 FD duoBLOCK, we achieve high precision in one clamping.”

To be competitive on the production side, NAMCO relies on CNC machine tool technology from DMG Mori. Vukovic explains the high investment volume in the past three years with the need to expand production capability: “On one hand, we need innovative machining technologies to manufacture efficiently and in the required quality, and on the other hand, it was a matter of increasing capacity.”

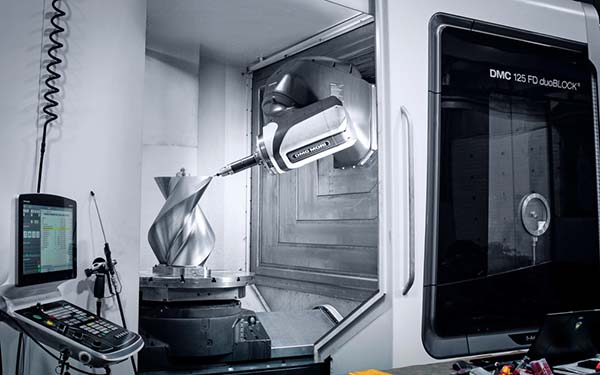
The versatility of DMG Mori machines is reflected in one of NAMCO’s core areas, gear cutting. Here, the team relies on a DMC 125 FD duoBLOCK with the exclusive DMG Mori gearMILL gear-cutting software. The mill-turn centre with pallet changer allows set-up to take place during machining and is designed for high-precision complete machining of rotationally symmetrical components up to 1250 mm in diameter – including five-axis milling and turning. Since everything is done in one set-up, errors due to manual re-clamping operations are eliminated.

For further information
www.dmgmori.com