New entry-level five-axis machining centre

At the recent DMG Mori open house held at the machine tool manufacturer’s Pfronten factory in Germany, a new five-axis machining centre was launched aimed at the entry-level market. Less than 2 m wide, the compact, competitively priced DMU 40 is capable of fully interpolative five-axis machining to within microns inside a 550 x 450 x 420 mm working volume.

Of trunnion-mounted rotary table design, the machine is based on the DMU 50 3rd Generation, of which more than 10,000 have been sold worldwide.The one-piece machine bed is made from grey cast iron, while the optimised geometry of the Y- and Z-axis slideways and the inline spindle with hydraulic clamping further ensure high rigidity. In addition, direct-drive ballscrews in the X and Y axes improve surface quality. For machining flexibility, the swivel range of the B axis extends from -35° to 110°.

The ergonomic design of the DMU 40 offers optimal accessibility to the work area. Table loading height is 800 mm and the distance from the operator to the table centre is short, while it is also possible to load components by crane. A large window and improved lighting provide good visibility. Optionally, the tool magazine may be loaded from the front.

There are three machine options with different equipment packages to meet individual requirements. The standard DMU 40 has a 12,000 rpm spindle and 24-position tool magazine, while the DMU 40 PLUS features a 15,000 rpm spindle and a tool magazine with 30 pockets, linear scales and passive cooling of all main components. Finally, the DMU 40 PRO is the most accurate and productive model, with active cooling and a 20,000 rpm spindle.
For further information www.dmgmori.com
GM CNC unveils heavy-duty machining centre

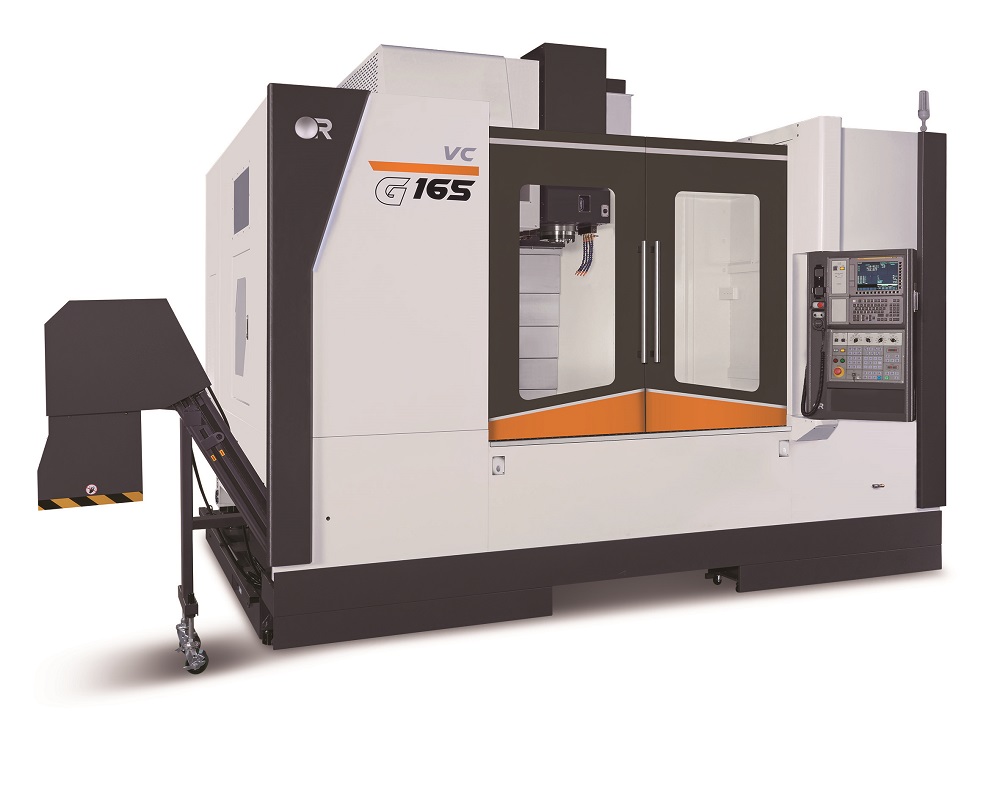
According to GM CNC,unparalleled stability and rigidity are the foundation blocks of the new VictorVcenter G-series range, which offers high material removal rates for applications where manufacturers are processing particularly challenging materials.

The three-axis G series is available in a trio of sizes to meet diverse demands. Unlike its competitors in the mid-sized VMC market segment, the G-series incorporates a meehanite casting with a wide base A-frame design, a wide span column, four boxways and screw removers with a wide boxway.

Victor’s smaller G105 provides X, Y and Z-axis travel of 1050 x 600 x 600mm,stretching to a spacious 1650 x 850 x 900mm on the largest G165. This freedom of movement is matched by accommodating bed sizes of 1100 x 600mm (G105), 1400 x 700mm (G135) and 1700 x 800mm (G165). Furthermore, the robust nature of the range permits the loading of components up to 1200, 2200 and 2500kg respectively.

Common features on all three machines include a powerful gearhead spindle design that generates a power output of 18.5 kW with a torque level of 498Nm. Developed, manufactured and built in-house by Victor, the 6000rpm gearhead design spindle retains maximum torque levels throughout the speed range. Thisfactor makes the Vcenter series a good choice for machining hard materials and exotic alloys with high material removal rates. In addition, the G-series incorporates a Big-Plus BBT-50 spindle taper that guarantees dual face and taper spindle contact.

The Victor Vcenter has an automatic tool change unit with 24-tool capacity and the option for 32 or 40 tool positions; all positions can accommodate tools up to 15kg.
For further information www.gm-cnc.com

Five-axis 30-taper VMC aimed at 40-taper market

30-taper vertical machining centre (VMC) manufacturer, Brother, has introduced a new five-axis model with a swivelling rotary table. Despite having a nominal footprint of just 1.5 x 2 m, the Brother Speedio U500Xd1 is capable of multi-face machining of components up to 500 mm diameter by 270 mm high, and weighing up to 100 kg.

Combined with a 28-position magazine for tools weighing up to 4 kg and either a 10,000 rpm/18.9 kW or 16,000 rpm/15 kW spindle with a face-and-taper interface option, Brother says that the production centre redefines machines in this class and is aimedsquarely at competing with 40-taper machining centres.

Sole sales and service agent in the UK, Whitehouse Machine Tools, points out that there is little competition to the machine on the market in terms of its operating speed. Rapid traverse is 50 m/min in X and Y, and even faster in Z, which accelerates at 2.2 g up to 56 m/min. Chip-to-chip time is 1.3 seconds, or faster still if a 14- or 21-tool magazine is fitted. Cutter exchange and axis motions take place simultaneously to minimise cycle times.

Trunnion swivel (A-axis) at 50 rpm is a -30/+120°and the table (C axis) rotates at 75 rpm. Roller gear cam mechanisms drive both rotary axes and 0-90° indexing times are 0.9 and 1.2 seconds respectively. Clamping torques are high at 610 and 500 Nm.

Lowering the power consumption of its machines has long been Brother’s aim. For a start, the electricity and air used by a 30-taper machine is only about 20% of that required by a 40-taper machine. The U500Xd1 is also equipped with a power regeneration system that reuses energy generated when the spindle motor decelerates.
For further information www.wmtcnc.com

Subcontractor gets into gear with Quaser machine

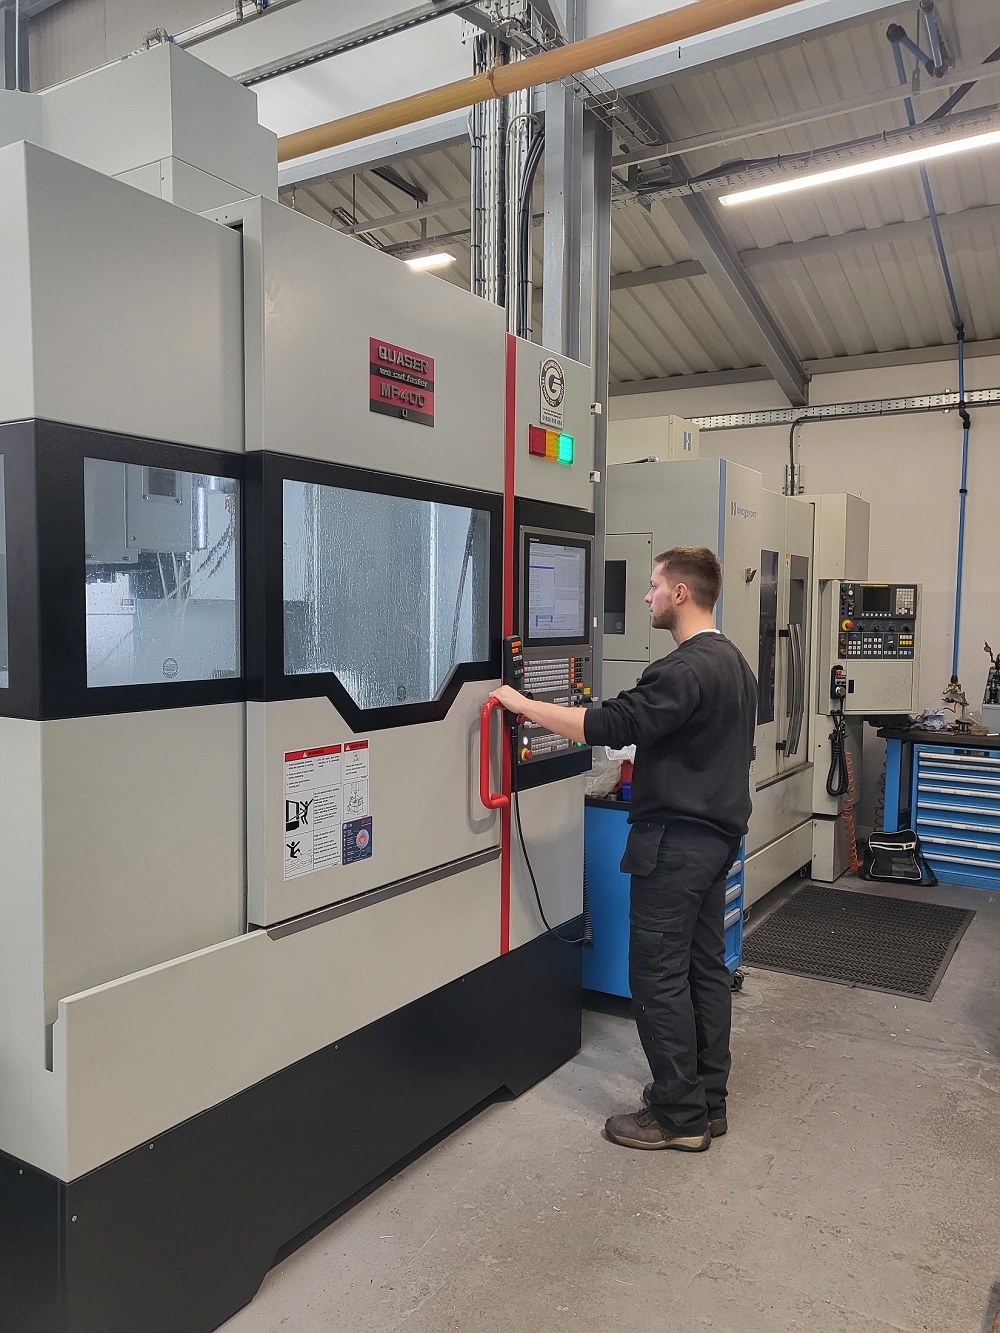
Leicestershire-based Sovereign Gears has recently invested in a Quaser MF400UH five-axis machining centre that follows on from three Nakamura turning centres also purchased from the Engineering Technology Group (ETG).

Director Ryan Spring says: “The majority of our work is 1- and 2-off bespoke gears, as well as jigs and kits for holding, assembling and working with the gears. Unfortunately, with so many complex forms, most of our milling work requires two, three or four set-ups, and this can take a lot of time and slow down our throughput. We bought the Quaser MF400UH with Open Mind’shyperMILL CAM software, also supplied via ETG to reduce our set-ups. The Quaser is our first five-axis machine, but we’re already seeing huge benefits.”

Previously, set-up time were frequently in the order of 4-5 hours, but the Quaser has instantly eliminated 75% of this time, and with only a single set-up required for five-sided machining.The precision of each component is subsequently improved.

“As a small business, it’s imperative that we maximise the productivity of both our machine tools and our staff,” says Spring.“By having the Quaser machine and reducing our set-ups, we’re freeing-up the capacity of two employees. Instead of spending excessive hours repeatedly setting up three-axis machines, staff can be allocated to other tasks.”

He adds: “Since having the Quaser, we’ve improved our ability to machine complex forms and this has ultimately won us new business that previously, we would have turned away. The ability to increase the type of work that we can machine, such as round gear teeth, challenging chamfers, forms and keyways has enabled us to increase our customer base and our offering to those customers.”
For further information www.engtechgroup.com

British Steel to become world leader in special profiles

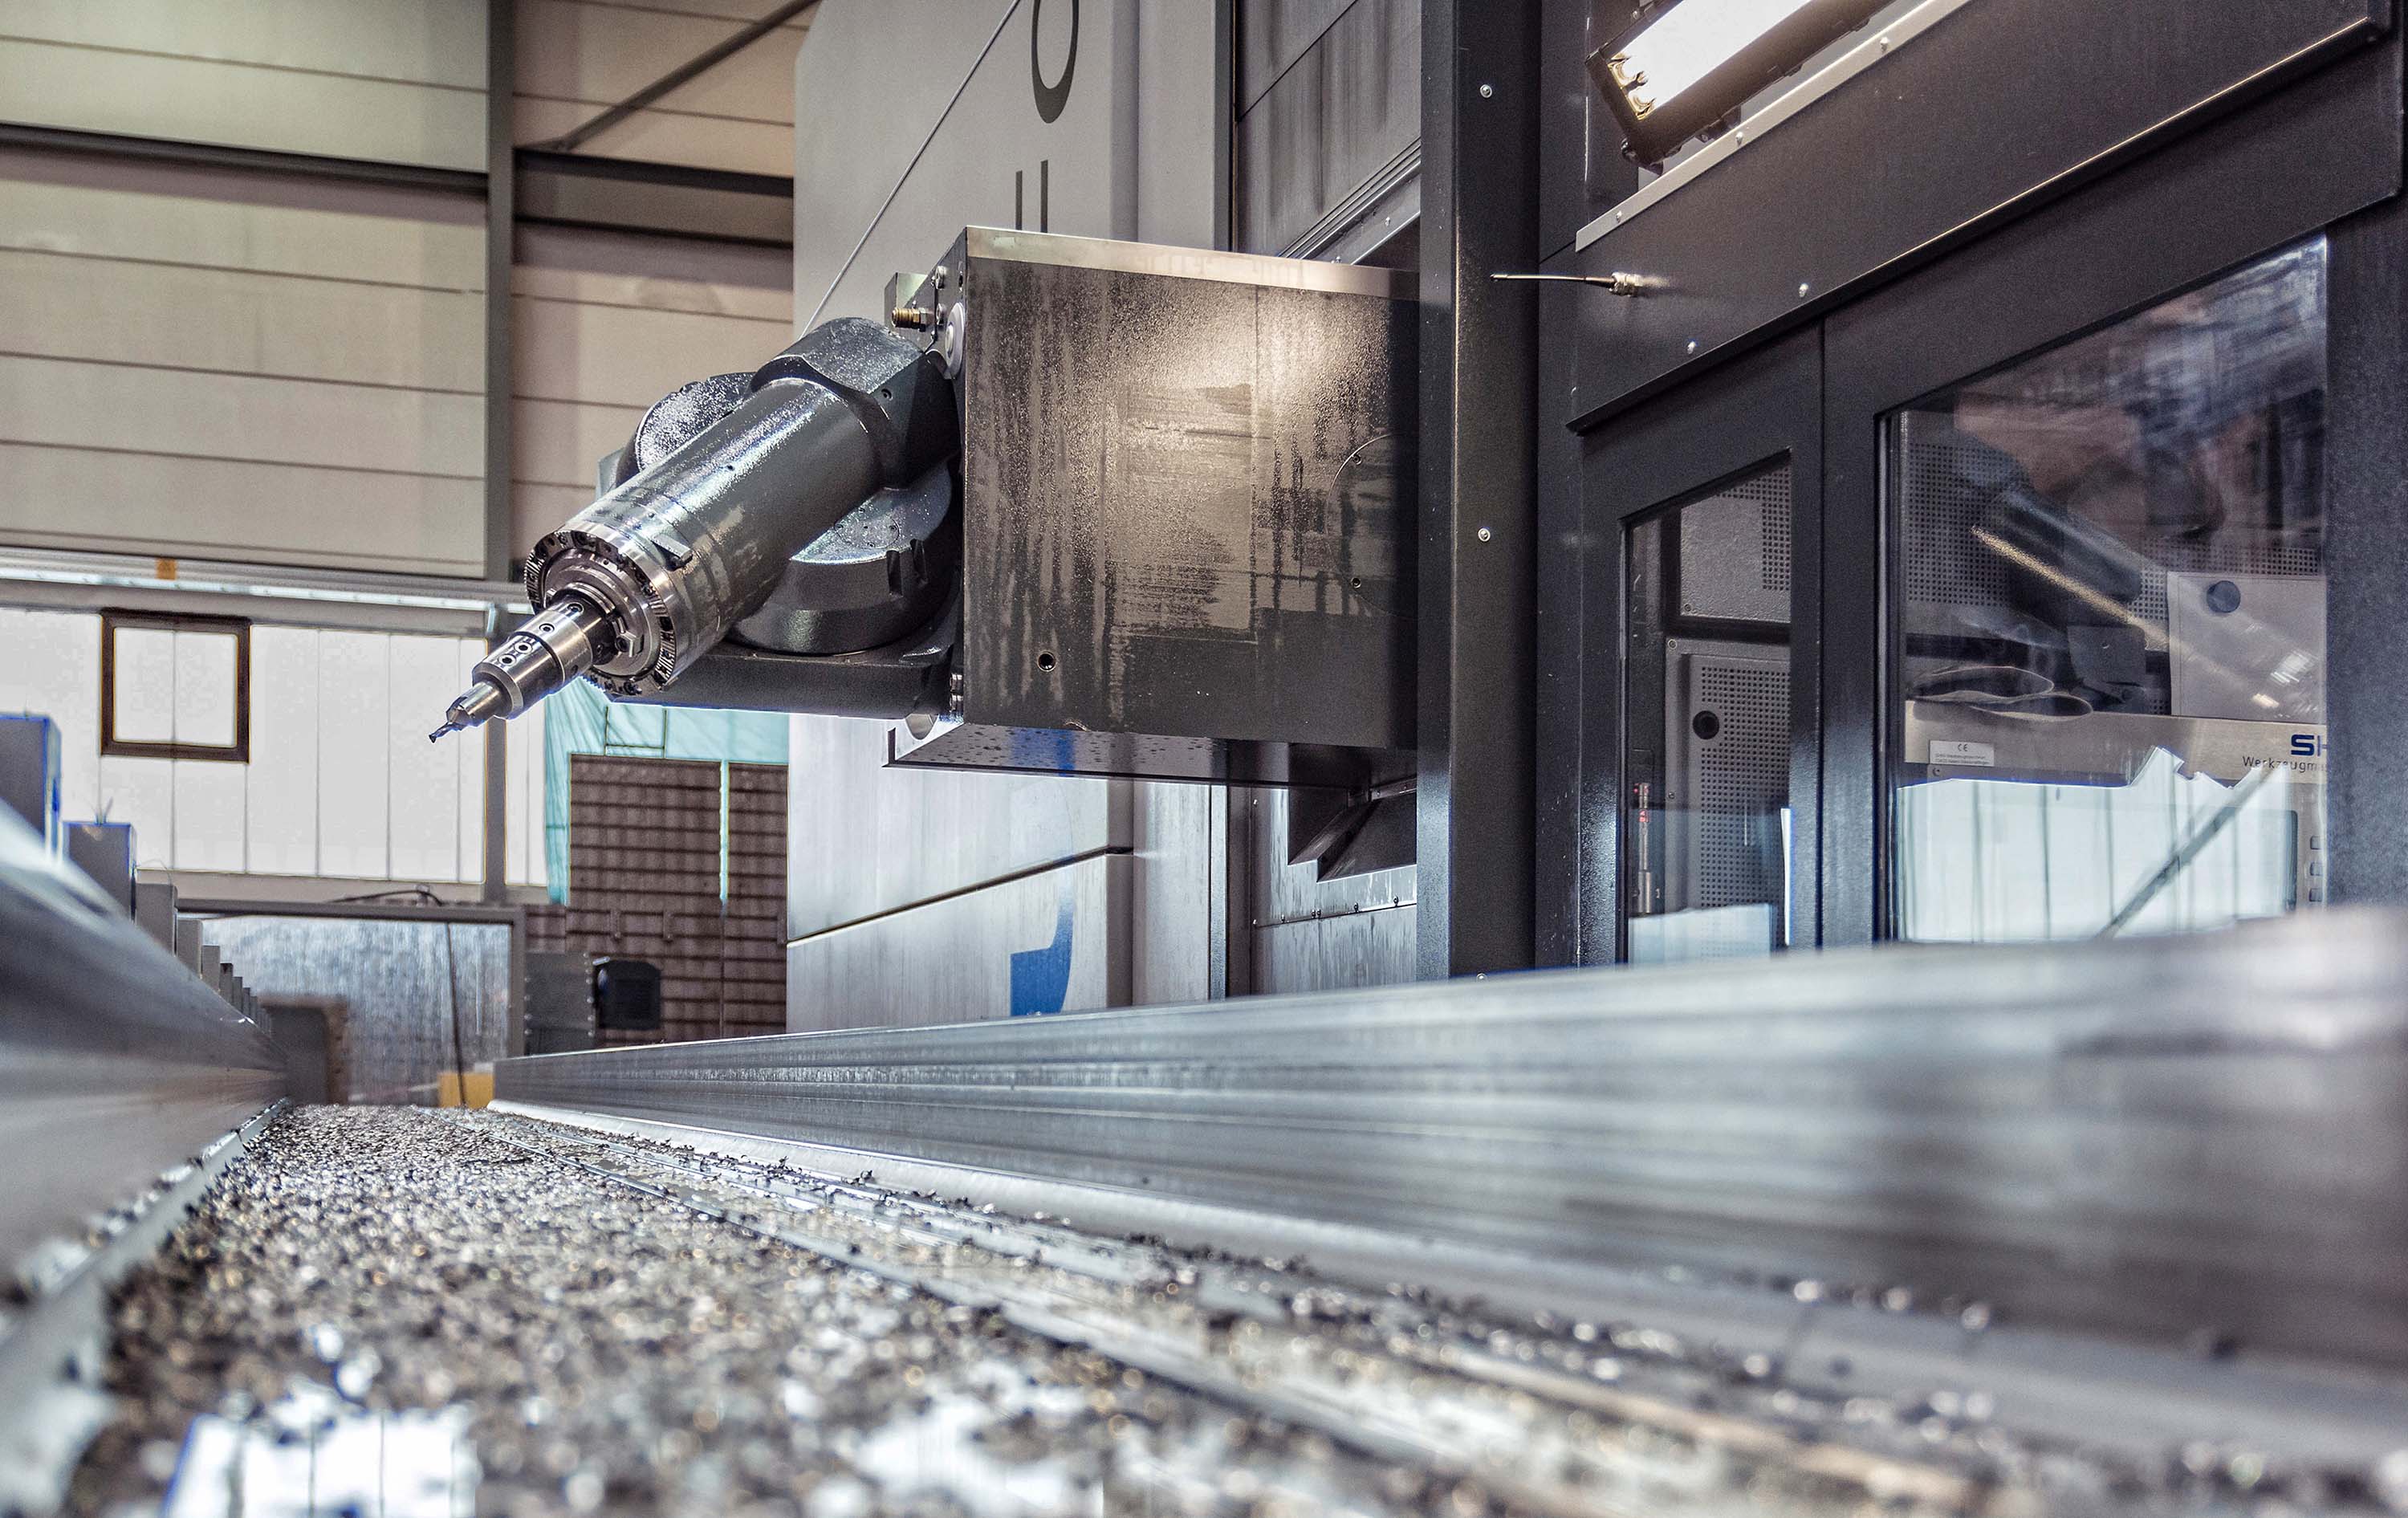
Forming part of a £26m investment by British Steel’s owner Jingye Group in the Skinningrove steelworks near Redcar, a travelling-column machining centre with a working envelope of 14,000 x 4100 x 1600 mm is currently being built in Germany by SHW Werkzeugmaschinen. It will arrive at Skinningrove towards the end of 2023, where it will be set up as a turnkey installation by Kingsbury, SHW’s sole UK agent.

Despite being of such large capacity, the Uniforce 4000 five-axis machine will nevertheless hold extremely tight tolerance on special rolled steel profiles produced in the mill. British Steel says that the combination of size and accuracy will set the company’s machining capability apart from that of other global players.

The rationale for the latest project is a legacy situation within British Steel that for the past 20 years has seen special profiles produced in Skinningrove transferred by truck 35 miles west to the group’s Darlington machine shop for processing. The resulting bottleneck limited throughput of the company’s special steel profiles and delayed its just-in-time delivery to world markets.

Dominic Hill, British Steel’s technical manager -special profiles, says: “We opted for this large milling solution from Kingsbury rather than those by other suppliers due to the high build quality of the German machine, as well as certain design features that are unique in this size range.One is counterbalancing of the head driven by twin ballscrews to compensate mechanically for droop, whereas the other OEMs offered less effective software compensation.

He adds: “The other significant plus point is the use of box guideways rather than linear guideways, which translates into higher rigidity, productivity and machining accuracy.”
For further information www.kingsburyuk.com