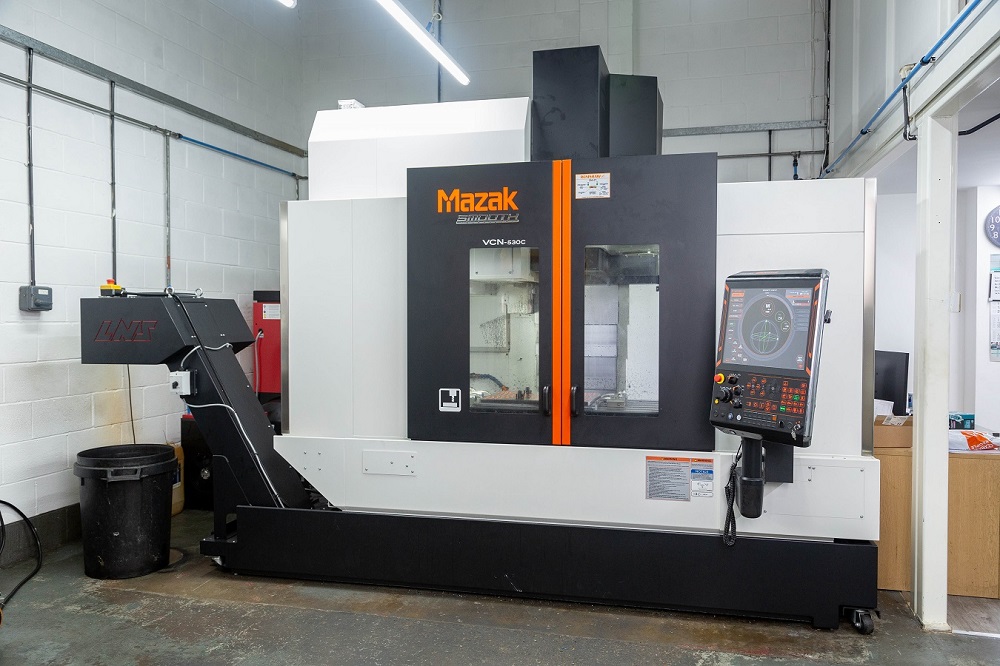
Toolmaker upgrades capabilities with Mazak VMC

Toolmaker SJ Dimmock has upgraded its manufacturing capabilities with the purchase of the company’s first UK-made Yamazaki Mazak VCN 530C vertical machining centre.The family-owned firm, based in Dunstable, was set up in 1985, since building a reputation for manufacturing high-specification injection moulding tools for the aerospace, medical, food and drink, automotive, and Formula One industries.

Company director Jamie Dimmock says: “Following the retirement of one of our long-serving employees, I found myself in the position of having three machines that I’d need to train myself to operate. As they were older machines, I thought it would be more effective to sell the machines to finance a new, larger vertical machining centre.After a lot of careful consideration and time spent evaluating the performance of comparable machines, I chose the VCN 530C vertical machining centre from Mazak. Each day that goes by confirms it was a fantastic decision.”

The VCN 530C is a high productivity vertical machining centre made at Mazak’s European manufacturing facility in Worcester. Equipped with a 40-taper spindle, Mazak says the machine excels at delivering high-speed machining with maximum stability and rigidity thanks to its heavy-duty casting.

Typically, SJ Dimmock is working to exceptionally tight tolerances of ±0.005 mm to meet the surface finish requirements of its customers. Here,Dimmock says the VCN has transformed the company’s machining operations. “We’ve replaced three machines with one and vastly improved the surface quality of the moulds, while reducing the volume of second operation work. The processing speeds are exceptional with the Mazak, which has not only helped with the quality of work, but has also doubled our capacity.”
For further information www.mazakeu.co.uk
Subcontractor progresses to five-axis machining

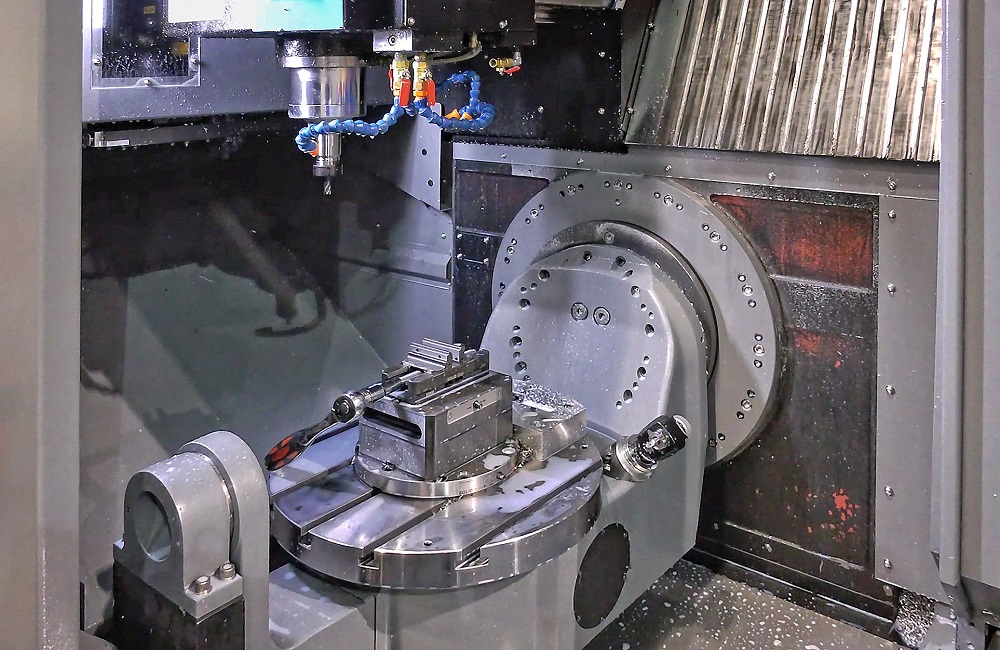
In its 20,000 sq ft, purpose-built factory in Hayes, near London Heathrow airport, subcontractor Wellington Engineering uses 45 CNC machine tools to produce parts for sectors as diverse as aerospace, medical, semiconductors and cryogenics. The latest machine to arrive on the shop floor isa Hurco VC500i machining centre.

Owner and managing director Daimon Wellington says: “We recently adopted a strategy of looking to take on more complex prismatic machining work and had already identified a number of contracts. It was just a question of finding a suitable machining centre.Full five-axis capability was the next step up for us in terms of technology and, as we use a lot of Hurcos, we decided to source our first true five-axis machining centre from them.”

The cantilever-type VC500i is ergonomic for easy operator access, has a 520 x 450 x 400 mm working volume and a ±100° swivelling trunnion carrying a rotary table, suitable for machining five faces of a component in a single set-up. It reduces the number of separate operations needed compared with using the subcontractor’s three- axis machines, including those fitted with single- or two-axis dividing heads.

Wellington says: “Our other machining centres were taking too long to produce the increasingly complex components. Productivity drives profits and we’ve had excellent results in this respect since the five-axis Hurco arrived. Parts come off much quicker and we’re not tying up the capacity of our other machines and their operators. Also there are far fewer issues with workholding and there is less deburring and hand fettling, all of which saves time.With five-axis strategies, jobs are coming off more economically in shorter cycle times.”
For further information www.hurco.co.uk

Burr-free results using supercritical CO2 coolant

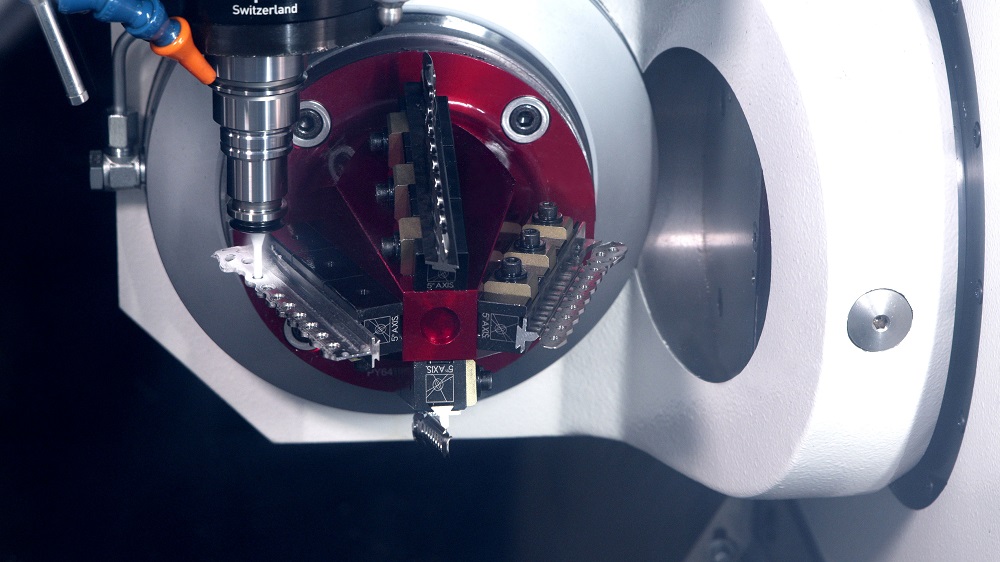
Supercritical CO2 milling of medical plastics using a Mikron Mill S 400U simultaneous five-axis machining centre from GFMS equipped with a Fusion Coolant Systems’ sc-CO2 delivery system produced impressive burr-free results in trials organised by GF Machining Solutions and the Competence Centre for Machining (KSF) at Furtwangen University IFC, Tuttlingen.

Ultra-high molecular weight polyethylene (UHMWPE) is a common material used in medical orthopaedics.The material’s durable, low-friction surface acts as a spacer that ensures mobility for knee, hip and shoulder implants. However, machining this material with traditional milling techniques results in the formation of burrs that often require manual removal in a secondary process.In addition, as the thermal expansion coefficient of UHMWPE is more than 12 times higher than steel, controlling heat during machining operations is essential to achieve the tight tolerances and high dimensional accuracies required for implants.

In recent tests, the effects of using supercritical CO2 cooling (sc-CO2) for the milling of spacers, using a Mikron Mill S 400 U five-axis milling machine equipped with a Step-Tec 42,000 rpm spindle and a Fusion Coolant Systems’ Pure-Cut+ sc-CO2 delivery system, were undertaken. The sc-CO2 is capable of providing CO2 up to 110 bar pressure and includes a Pure-Cut+ MQL delivery system.

Two different spacer cutting trials took place: slot cutting using a 3mm single-blade end mill andfive-axis milling using a 6 mm ball-nose endmill.The results obtained in both trials indicate a significant reduction in burr formation, improved workpiece accuracies and better surface quality.These factors point toward a more reliable machining process that may greatly reduce, or even eliminate, manual deburring.
For further information www.gfms.com

Start-up invests in MACH MDS 845-8T mill

MACH Machine Tools has supplied PMR Developments & Engineering, a precision subcontract specialist start-up, with a new tool-room mill. Now in situ at the company’s Hereford facility,the three-axis MACH MDS 845-8T features theDynaPath WinDelta CNC.
The MDS 845-8T is the most recent machine tool investment made by PMR in its three-year history and has taken its place alongside a new mini mill and a pre-owned two-axis lathe.

PMR’s new MDS 845-8T machines a range of precision components, including injection mould tool inserts and associated parts for a number of customers in the automotive and medical sectors, as well as new and replacement industrial equipment parts.These parts, typically machined in small volumes from a range of different materials, are characterised by their tight geometric and dimensional tolerances, and their high surface finishes.

To meet lead times and ensure that PMR achieves its machining contract requirements on time and in budget, the company regularly pushes the MDS 845-8T’s capabilities to the limit in order to reduce part cycle times.Where feasible, PMR deploys high material removal rates involving extended depths of cut and optimised speeds and feeds.

Says William Homes, PMR’s owner and director:“Our investment in the new MDS 845-8T has significantly increased our machining capacity and capabilities. The machine is powerful, fast, accurate and flexible and, although classified as a ‘tool-room mill’, such is its technical specification and processing capabilities that it’s much more production-oriented.”

He adds: “The versatility and flexibility of the DynaPath control system are also impressive. “Straight-off-the-bat, we liked the control’s large 15.6” LED touchscreen, its clear and logical navigation, and its simple-to-use and understand menus and operation screens, which all help reduce set-up times and prevent input errors.”
For further information www.machmt.co.uk

700% growth in three years in partnership with XYZ

James White joined NSK Precision Engineering in 2015 and took the company over in 2019, making a new CNC machining centre his top priority. His research led him to invest in anXYZ 750 LR with 750 x 440 x 500mm travel, Siemens 828D control (with optional ShopMill), and linear rail technology for fast acceleration and deceleration rates.

“XYZ Machine Tools listened to where we wanted to take the business, asking the right questions, showing that they understood how our company works,” he says.“They also came up with an attractive solution to get our CNC machining capacity started. We already had a 1994 XYZ turret mill with ProtoTRAK control, which is used daily, so this gave us extra confidence in our decision.”

Taking over NSK Precision Engineering, which has been in operation since 1995, was a steep learning curve, figuring out how to manage both the workforce and the day-to-day administration of the company. Additionally, White relocated the company from its previous 1500 sq ft factory to a new 10,000 sq ft site near Reading, while growing turnover by 700% and increasing his workforce from two to seven.

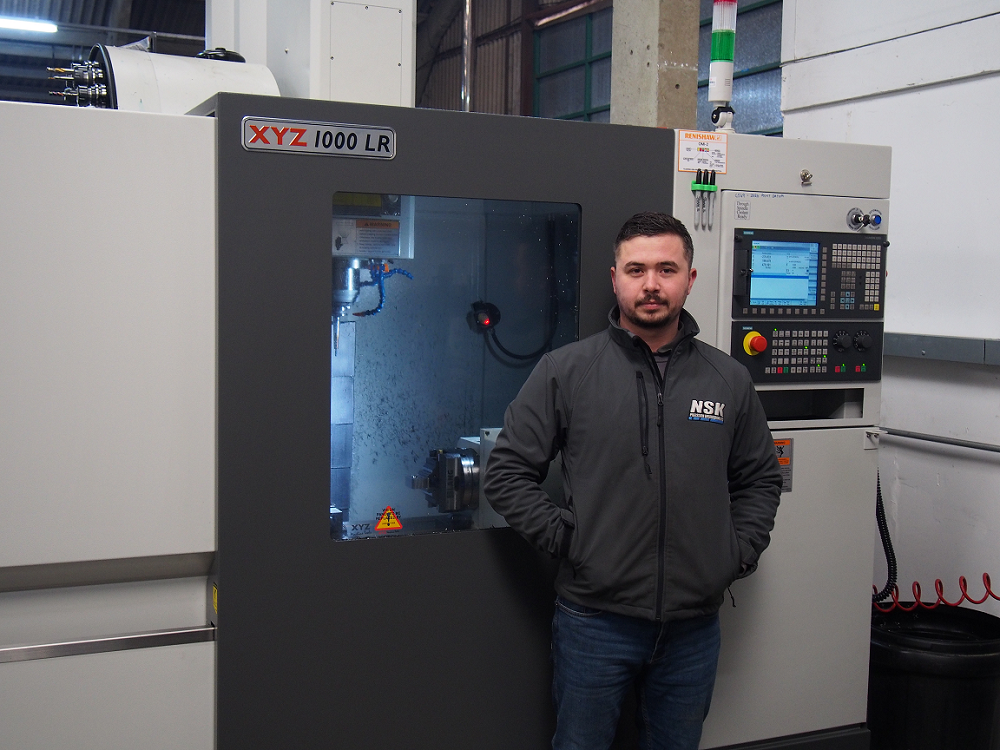
“Previously, we were subcontracting a lot of work to local companies,” he explains.“Investing in CNC has enabled us to take this work back in-house, which gives us more control over quality and delivery while at the same time improving our profit margins. At the old factory, we were limited for space, restricting which XYZ machine we could choose. With the new factory and the increase in workload we’ve been able to make a further investment in a XYZ 1000 LR with 4th-axis rotary table, Siemens 828D control with the ShopMill option, expanded 24-station tool carousel and a swarf conveyor.”
For further information www.xyzmachinetools.com