Entry-level robot automates machine tending

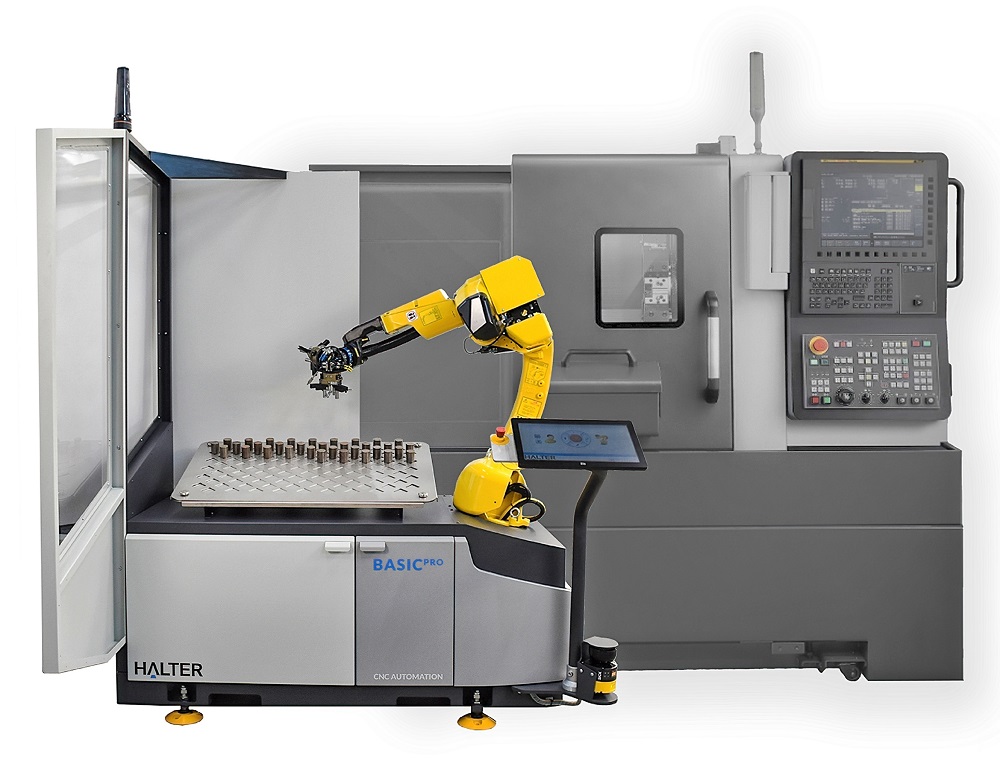
Dutch firm Halter CNC Automation has introduced an entry-level machine tending cell for
loading and unloading. Availability in Great Britain is through sole agent 1st Machine Tool
Accessories.
Comprising a six-axis industrial robot, the Basic Pro offers a price-competitive automation
solution. With the manufacturer’s user-friendly touchscreen SmartControl, the changeover
time to start a new production process is only a few minutes. Furthermore, the operator
needs no prior experience of robot programming, which takes place while machining of the
previous parts is in progress.
The plug-and-play Halter Basic Pro can be supplied with new machines or retrofitted to
existing plant regardless of machine age and control type. Use of a floor-level, 270° laser
scanner provides a safety zone. The robot slows if the operator approaches and stops
immediately upon breaching the light curtain.
An adjustable air pressure supply is provided for the double gripper, which can have either
two or three fingers for holding raw material and finish-machined workpieces internally or
externally. It is possible to handle workpieces from 10 to 135 mm diameter or square up to
a maximum weight of 12 kg, including the gripper head. The grid plate holding the raw
material and finished parts is adjustable in height to suit the installation and can hold up to
188 workpieces if the locations are sized up to 20 mm, the number dropping to 14 parts as
the size reaches 135 mm.
Halter has more than 1000 installations worldwide feeding CNC lathes, machining centres,
deep-hole drilling machines, grinders and other machine tools, as well as CMMs. Nearly 95%
of customers across 25 countries, including two dozen or so in the UK, report a return on
investment within 5 to 18 months.
More information www.1mta.com
Green energy powers XYZ lathe purchase

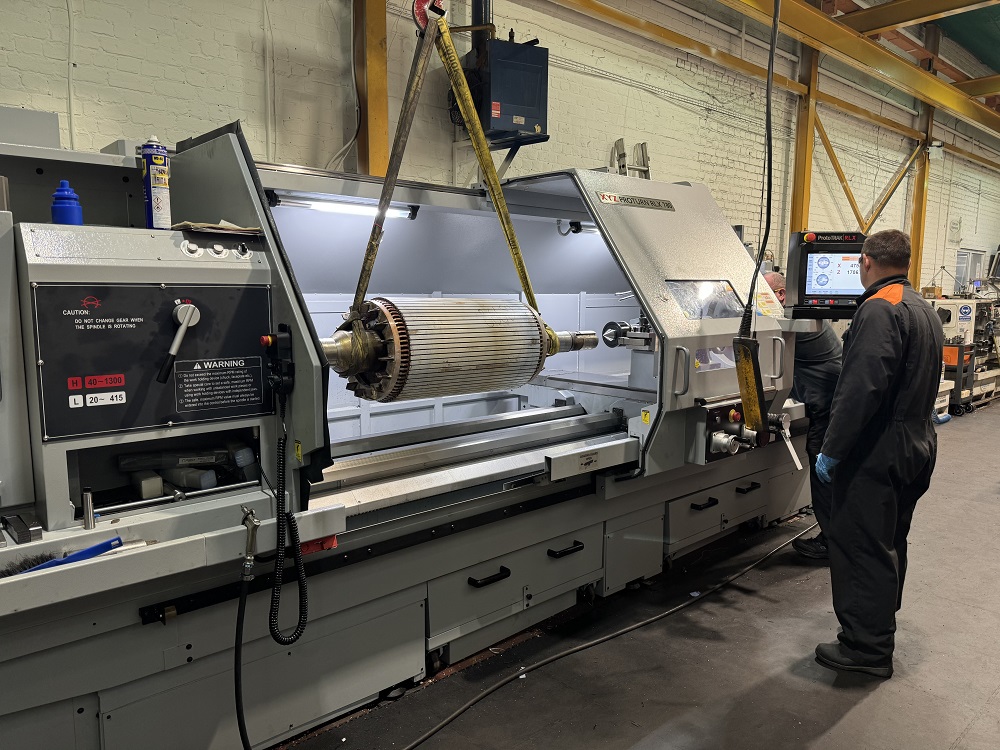
Fletcher Moorland, a Stoke-based company that repairs and refurbishes motors, pumps,
gearboxes and fans, has purchased an XYZ RLX 780 flat-bed CNC lathe with ProtoTRAK RLX
control as part of efforts to expand services for its growing customer base.
Says third-generation managing director Matt Fletcher: “We traditionally worked on sub 1
MW motors but, with advances in wind turbines, we’re now seeing repairs required on
equipment up to 2.5 MW. These machines, which weigh around 10 tons, have bigger rotors
and end shields, and we didn’t have a machine to process these larger parts.”
The process of acquiring a large-capacity lathe involved researching the market, which
culminated in two visits to XYZ’s Midlands Technical Centre in Nuneaton.

Electrical-mechanical workshop Manager Matt Sparkes says: “Demonstrations from XYZ’s
area sales manager gave us the confidence that the RLX 780 was the right fit in terms of
machine size and capacity. After seeing the ProtoTRAK RLX control, used both manually and
in CNC modes, we knew it was the best solution for our workshop.”
With shafts and rotors increasing in size, Fletcher Moorland is already benefiting from the
purchase of the XYZ RLX 780.
“Its 160 mm diameter spindle bore is advantageous, especially when we recently machined
a batch of conveyor rollers,” explains Sparkes. “The additional fixed steady we purchased is
also proving its worth.”
In a closing remark, Sparkes says: “We really feel that the ProtoTRAK control is the way
forward. Its ease of use and flexibility aligns with our processes, and we see it enabling us to
produce one-offs quickly and efficiently using the conversational format that the control
provides.”
More information www.xyzmachinetools.com

B-axis tool spindle instead of a turret

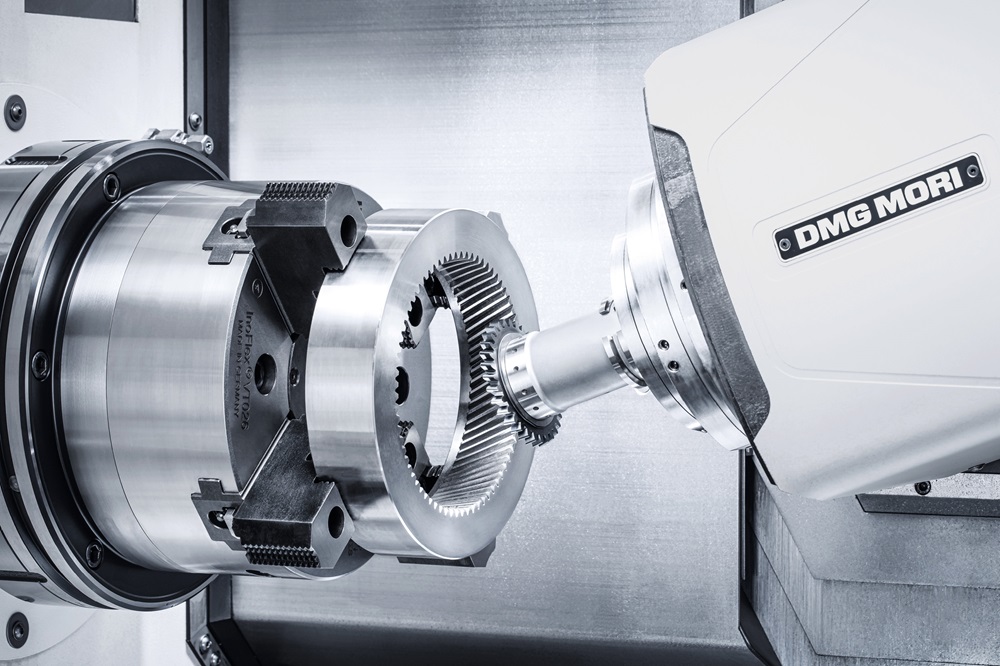
Increasing component diversity and diminishing batch sizes tend to extend periods of unproductive set-up. The CLX TC turning centre series from DMG Mori addresses this issue by replacing the tool turret in the company’s CLX lathes with a ±120° swivelling B-axis tool spindle that offers positioning resolution of 0.001°. The new CLX 550 TC model is now available, joining the smaller capacity CLX 450 TC introduced in 2023.

A tool magazine offering space for up to 60 cutters (30 tools is standard) serves a CompactMaster 12,000 rpm turn-mill spindle with 90 Nm of torque. Tools can be loaded and unloaded in parallel with production to minimise machine downtime.

The main and counter-spindle motors are rated at 4000 rpm/720 Nm, maintaining flexibility when programming the machine to produce complex components on six sides in one hit. Users can deploy chucks up to 400 mm in diameter, while bar capacity is 102 mm.

Maximum workpiece size is 550 mm diameter by 1600 mm in length. The use of steady rests, which are available up to a workpiece diameter of 360 mm, is recommended for machining long components. A Y axis with 270 mm of travel allows eccentric machining.

DMG Mori’s Celos X user interface in conjunction with the Siemens Sinumerik One control and ErgoLine operating panel enable the use of multiple software offerings. They include OP Workbench to enhance the efficiency and productivity of machine operators, as well as dozens of app-based technology cycles.

In addition, 3D Shopfloor Programming, a joint development by DMG Mori and Siemens, uses the 3D model of a component from the design department to create an NC program mostly automatically based on underlying data. Automated feature recognition speeds programming time by up to 80%.

More information www.dmgmori.com

Quest for flexibility brings Nakamura investment

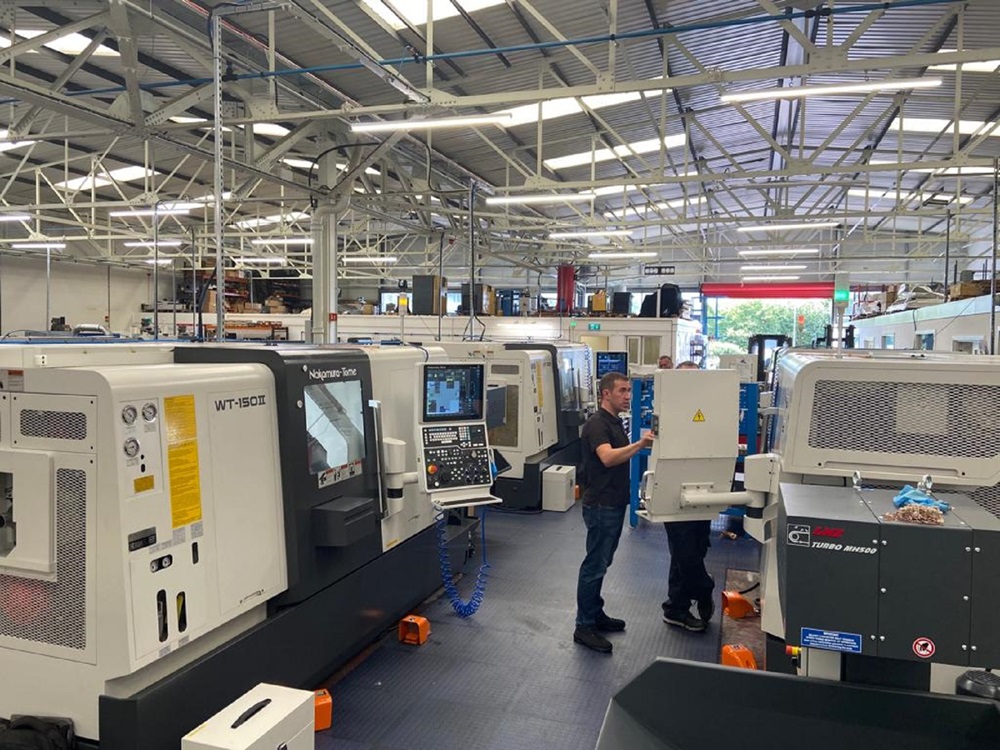
Quest Precision Engineering has been on a trajectory of continuous growth thanks to the acquisition of seven high-end Nakamura-Tome turning centres from the Engineering Technology Group (ETG). The Scottish manufacturer initially acquired two Nakamura-Tome turning centres through the pandemic and has kept adding to the plant list ever since.

The Dundee-based company has four Nakamura-Tome WT150II turning centres, two NTY3-150 turn-mill centres and has just purchased a Nakamura MX-100 from ETG’s Scottish distribution partner RAM Engineering & Tooling.

“We’ve been working with Quest Precision for over 20 years and done a lot of applications together, focusing on productivity and flexibility,” says Ross Milne, company director at RAM Engineering & Tooling. “This is epitomised by the Nakamura MX-100 turn-mill centre with swivelling B axis, opposing spindles and lower turret. We’ve also got a gantry loader and bar feed on the machine. It’s a proper step-change.”

Gordon Deuchars, managing director at Quest Precision, says: “Nakamura one led to Nakamura two in just three months, and then around 18 months later we won a big order. This brought Nakamura three and four online. More recently, we’ve been manufacturing the complex ‘Mark 3’ autonomous valve for the oil and gas industry from Inconel 718. We needed a robust machine to take us to the next level, namely the NTY3-150. We’ve now progressed to the Mark 4 valve, which is why we recently installed the MX-100 multi-axis machine.”

He adds: “Our relationship with ETG has been first class. From the moment we enquired about the first machine they’ve been there for us on every turnkey project. The Nakamura range offers the flexibility, efficiency and reliability that we need as a busy manufacturer in the subcontract field.”

More information www.engtechgroup.com

Dorries VT 28 vertical turning centre unveiled

The Starrag Dörries VT 28 vertical turning centre is now available for the one-hit machining of large components in the aerospace, power generation and offshore sectors. It combines proven technology from the Dörries Contumat VCE series with a raft of new solutions and technologies that the company says enhance both machining performance and productivity.

Capable of machining heavy components up to 17 tonnes with a maximum diameter of 2.8 m and a height of 2.65 m, the Dörries VT 28 is a multifunctional, high-precision, flexible vertical turning centre for everything from rough to finish machining in a single operation. The compact single-column vertical turning lathe is suitable for turning, drilling, boring, milling, grinding and more.

Notably, the column base forms part of the machine’s foundations, increasing rigidity, performance and stability while minimising installation costs and machine footprint. From a dimensional perspective, the Dörries VT 28 offers a 2.8 m swing diameter and a 2.5 m table diameter that permits the machining of exceptionally large components.

The VT 28 delivers torque of 11 kNm with 98 kW on the main S1 drive and a speed range of 250 rpm. According to the company, this enables end users to wield vast depths of cut at high machining parameters while ensuring maximum stability, rigidity, performance and surface finish.

Further enhancing the stability and rigidity characteristics of the Dörries VT 28 are wear-free hydrostatic guides in all linear axes that maximise the vibration-damping performance. The new hydrostatic system reacts with minimum fluctuation to deviations in temperature and viscosity.

From a flexibility standpoint, the Dörries VT 28 has a ‘master head’ concept that enables the decoupling of the milling drive and tool interface to provide additional protection against collisions. More information www.starrag.com