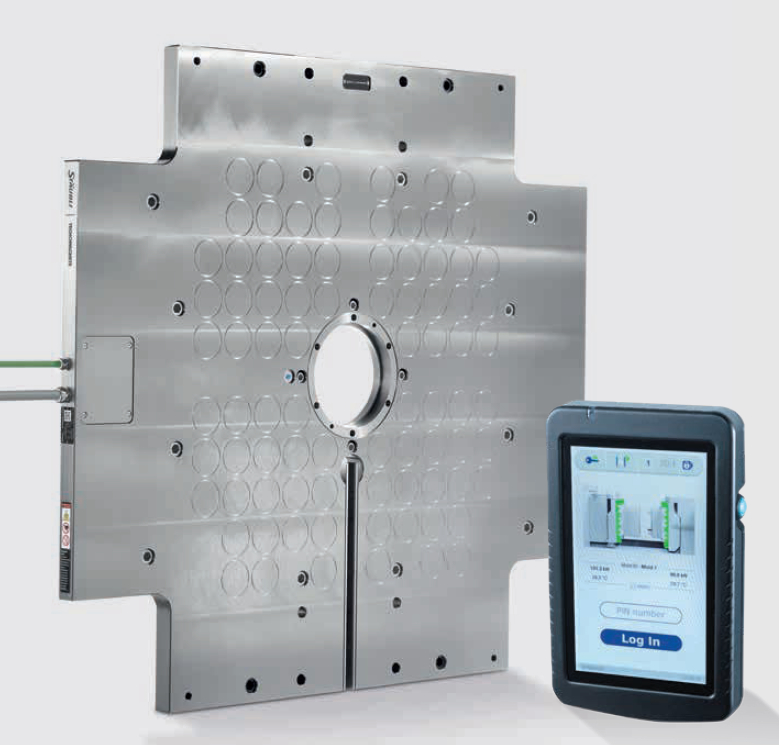
Magnetic injection mould clamping system unveiled

Staubli and Mag-Autoblok Tecnomagnete say they have pooled their expertise totake the capabilities of magnetic clamping technology to the next level with the release of the QMC123 magnetic clamping system for injection moulding machines. An essential part of the co-development process for QMC123 was to ensure that the new system not only retained the previous system’s attributes of robustness and reliability, but also a level of familiarity for existing customers who have been using the current system since 2010.

QMC123 provides greater levels of information and features a new and easier-to-use operator touchscreen thatenables the validation of the various safety points during mould-changing operations. The IMAG-Editor software enables the calculation of clamping force for each mould prior to loading, based upon the customer’s specific press. This information highlights any potential problems ahead of production. Furthermore, intuitive guidance is availableto the operator, not only during set up, but also to assist in diagnosing warnings or error conditions, facilitating faster and safe resolution.

The manufacturing processes for the QMC123 magnetic platen design have also seen optimisation to guarantee better measurement accuracy of the clamping forces. In addition, the system is able to detect flux changes before actual mould movement takes place, further increasing safety.

As a further point, the QMC123 magnetic clamping solution will play a key role in SMED (Single Minute Exchange of Die) strategies by minimising the time between the last good part and the first good new part. Moreover, with its data acquisition capabilities, this new-generation technology is also compatible with the principles of Industry 4.0.
For further information www.staubli.com
Okuma to hold open house in November

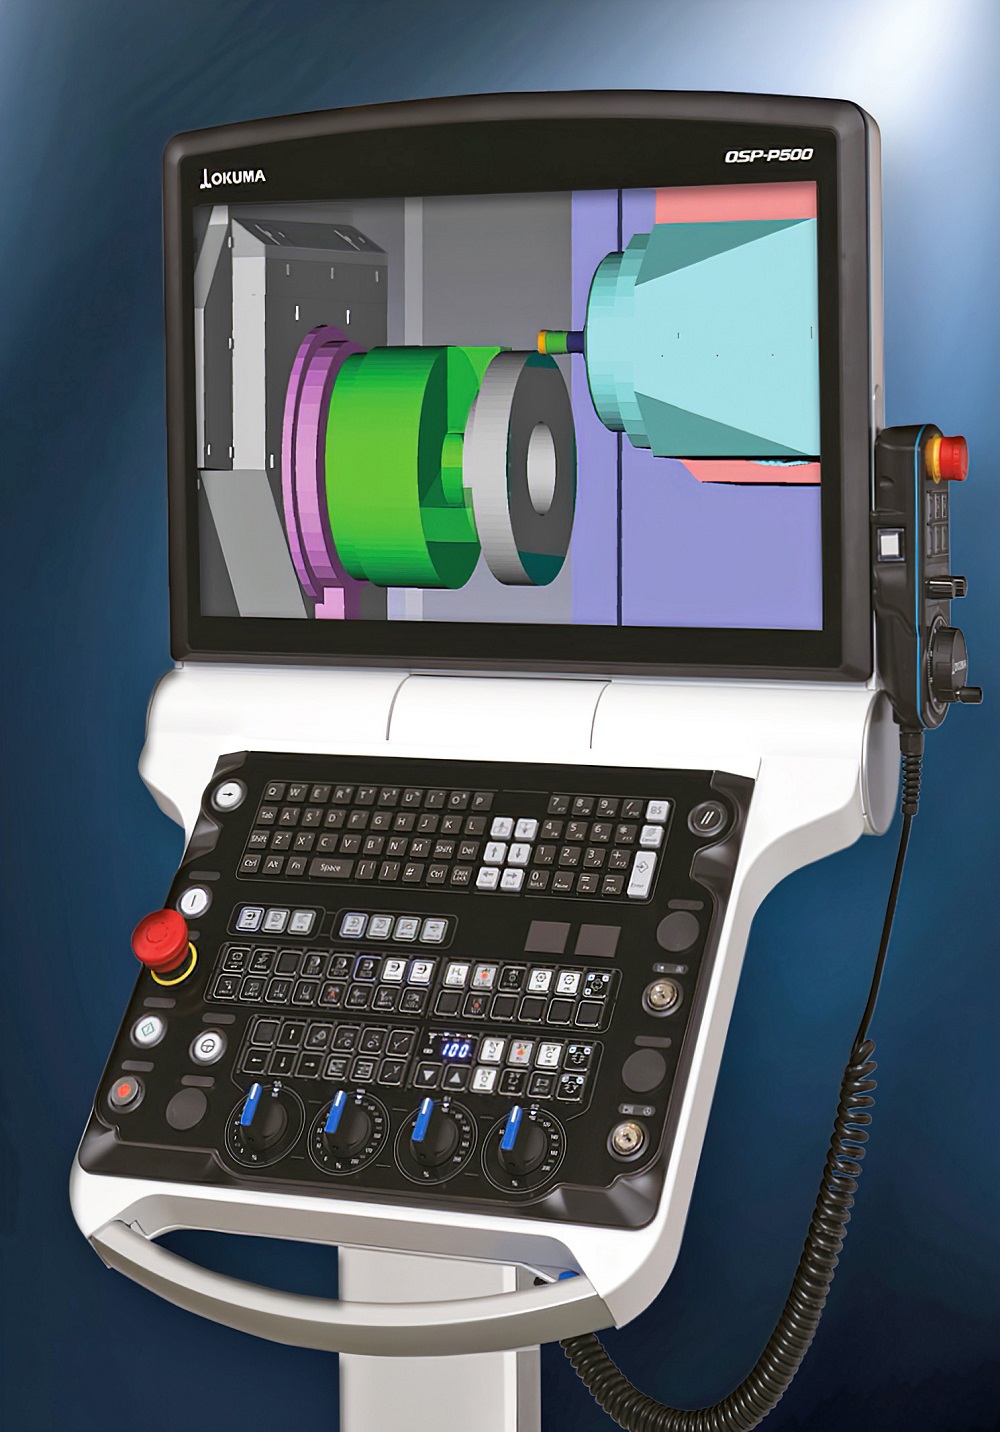
This year marks the 125th anniversary of Japanese machine tool manufacturer Okuma, as well as the 60th birthday of its in-house manufactured CNC system, OSP. In celebration of these milestones, an open house will take place at the group’s European headquarters in Krefeld, Germany on 21-23 November. The company will also provide guided tours in English and German, live machining sessions and new equipment presentations. Anyone wishing to attend the free event can register at the web address below. NCMT is the sole sales and service agent for Okuma in the UK and Ireland.
For further information https://openhouse2023.okuma.eu

Investment at Ficep UK

Ficep UK is investing in its offices and stockholding capacity as a direct response to growing
demand from clients who rely on the company’s machines. Newly added storage space
holds more stock by introducing 44 pallet spaces to its 17,000 sq ft warehouse in West
Yorkshire. The installation of an additional carousel system will double holding capacity,
ensuring that essential components and spare parts are readily available to meet customer
requirements. Ficep UK has also created new office space, located within the warehouse, to
serve as a hub for the company's tooling and consumables service team.
For further information www.ficep.co.uk

Expediting production of high-precision blades

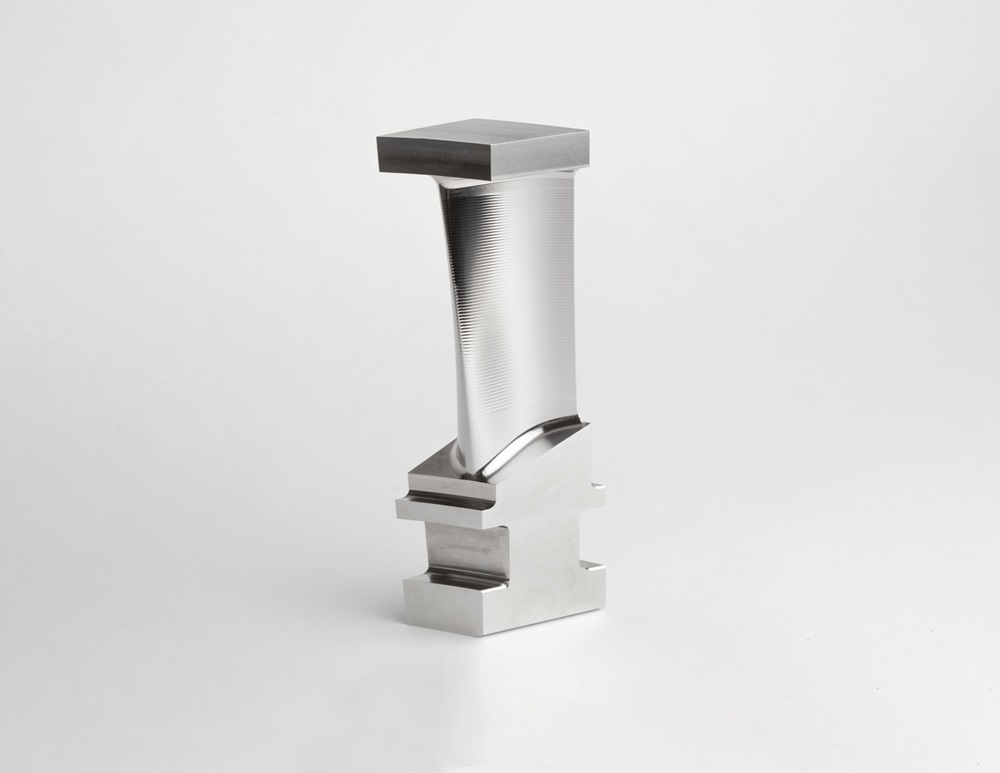
GF Machining Solutions (GFMS) recently introduced, via its Liechti Engineering AG subsidiary, a high-performance simultaneous five-axis machining dedicated to the fast and efficient processing of high-precision blades used in the aerospace and power generation industries. The Liechti Turbomill 500g, with a whole host of features that include Liechti’s g-technology and ‘Tool Pivot Point’ machining capability, helps manufacturers machine high-quality, competitively-priced blade components in double-quick time, reports the company.

The machine, equipped with a 20,000 rpm HSK-A63 StepTec spindle and up to 2000 rpm turning capability, boasts 2 g acceleration/deceleration rates and 60 m/min linear feed rates, ensuring that the Turbomill 500g gets down to business fast. According to GFMS, the machine helps to reduce part cycle times by up to 30%.

These ultra-fast processing speeds do not compromise accuracy or quality as the Turbomill 500g can achieve blade accuracies of ±0.015 mm, and surface finishes of 0.4 µm. To ensure high-productivity through unattended operation, users can opt to equip the Turbomill 500g with a bar feeder that automatically loads bar stock into the machine.

For consistent, high-quality part production, the machine features direct-drive motors (on all five axes), as well as an internal bed cooling system and intelligent thermal compensation that helps stabilise machining temperatures and reduce the effects of thermal drift. The machine is also equipped with Liechti’s 100 rpm Tool Pivot Point innovation which, available on the machine’s B axis, ensures fast and accurate contouring around blade edges. Reduced movement of the linear axis delivers shorter cycle times, higher positional accuracies and less mechanical wear.
For further information www.gfms.com

A new dawn at Norton Motorcycle Company

One of the great names in British motorcycling is rising again under new ownership and with new state-of-the-art machining technology. The Norton name is synonymous with the golden age of British motorcycling that ran from the end of the 19th century to the second decade of the 21st. It is a history that takes in Grand Prix wins in the 1930s to World Championships in the 50s.

Alas, the decline of British motorbike manufacturing led the company to the brink of bankruptcy and it was only the intervention of Indian motorbike manufacturing giant, TVS, which saved it in 2020. Following the new investment, a willingness to embrace new ways of working led Norton to examine its bike frame fabrication processes.

“Previously, we’d been hand bending and hand scalloping the bike frames because we didn’t know how to do anything different,” says Adam Green, senior manufacturing process engineer at Norton Motorcycles. “We looked at various options, but wanted to invest in the best-available machine. Mazak are the kind of people we want to be doing business with.”

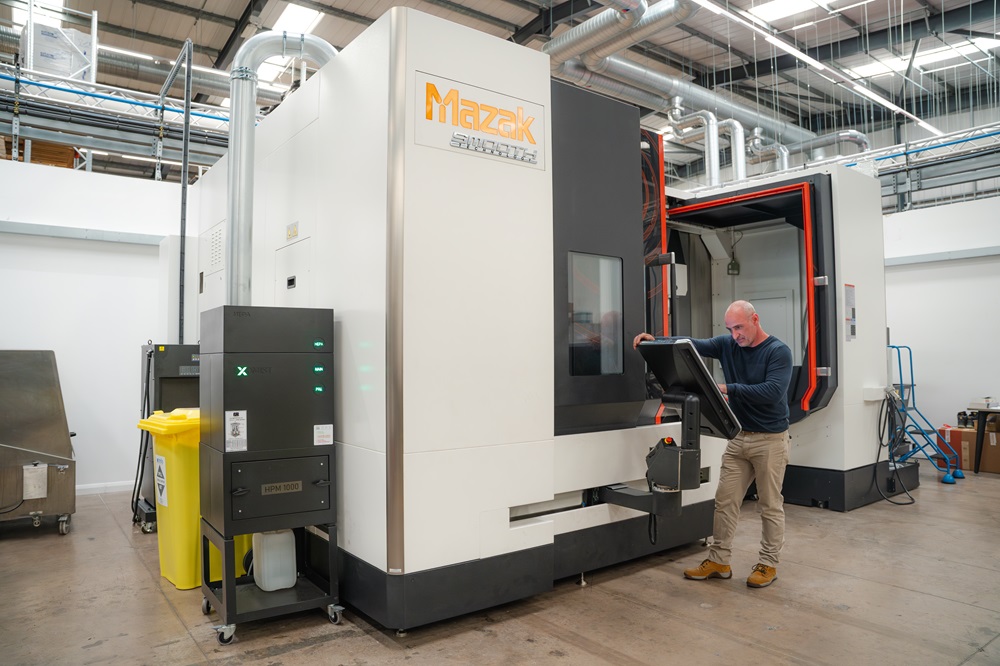
Norton specified a VTC 800/30SLR, manufactured in nearby Worcester, which has a high-capacity working area and a wide door opening making it suitable for larger workpieces, such as motorbike frames.

“The size of the frame meant we needed a big machine, but also one that could work to very high tolerances,” says Green. “It’s all about repeatability. The machine takes away manual process. Now every single dimension will be within 0.2 mm of each other. We’ve tightened tolerances up by 80%, whereas previously there was 6 mm of difference at times from one frame to another.”
For further information www.mazakeu.co.uk